Home Authors Posts by BLADE Staff

BLADE Staff

Video: Homemade Hydraulic Press for Knifemaking

1

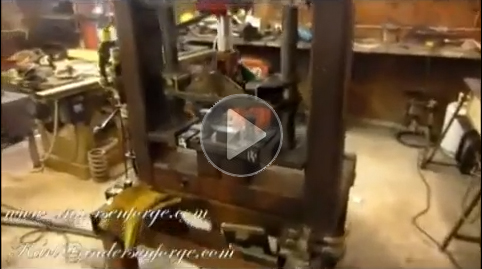
In this video from the American Bladesmith Society (ABS), journeyman smith Karl B. Andersen reviews his homemade hydraulic press. Andersen uses the innovative device to make damascus steel for his blades.

Andersen said he receives questions about what went into his homemade hydraulic press. It’s no wonder. This is one cool piece of knifemaking machinery. While Andersen has made his own modifications, the core design is from the mind of Michael Kanter from Wisconsin. From the video:

“It just doesn’t look like the other presses going…It’s very unique in its structure. Everything is contained within a picture frame. The tubular frame is made up of real high tensile steel.”

Despite being built like tank, Andersen points out that the pressure is all contained inside the homemade hydraulic press. Note the part where the arrow on a postage scale underneath the press doesn’t budge while the machine is running.

What about you? Ever consider building your own homemade hydraulic press? Leave a comment below.

Tips for making damascus knivesSpeaking of damascus, you don’t necessary need a homemade hydraulic press to make those eye-catching blades. Check out this download from BLADE on how to make damascus knives.

Benchmade Hires David Fee as VP Sales/Marketing

0

Benchmade Knife Company has announced that David Fee will be the new Vice President of Sales and Marketing. The position involves all sales and marketing activities for Benchmade at their headquarters in Oregon.

“We’re thrilled to have David join the Benchmade senior management team,” said Les de Asis, founder and CEO of Benchmade Knife Company, in a news release. “His background and success in the consumer product and automotive industries will help drive our sales, marketing and new products initiatives as we continue to grow and compete on a global scale.”

Click here to visit the Benchmade website.

Video: New England School of Metalwork Tour

0

Here’s a look at the classes offered by the American Bladesmith Society at the New England School of Metalwork.

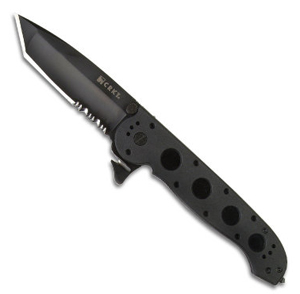
Featured Knife: CRKT Kit Carson M16-14ZLEK

0

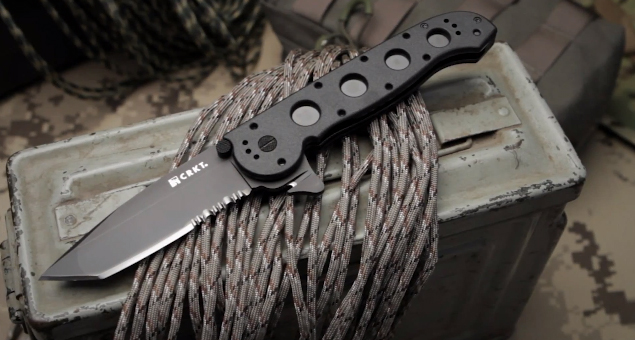
The M16 line of Kit Carson knives manufactured by Columbia River Knife and Tool (CRKT) continues to grow in popularity. The latest from this partnership is the M16-14ZLEK, a blade that some are calling the best tactical knife in the M16 family.

Here’s the rundown on one of the hottest CRKT knives on the market:

Columbia River Knife and Tool Kit Carson M16-14ZLEK
The M16-14ZLEK is the latest knife from the CRKT/Kit Carson partnership. Like all knives in the M16 line, it’s ready for tough jobs right out of the box.

Columbia River Knife and Tool produced Kit Carson‘s popular M16® line in many variations over the past decade. Our glass filled nylon version has built the largest user base of all. These knives are built for function, not fad, and they are exceptional values.

Our new M16 ZLEK line uses our very successful InterFrame construction, with tough, textured glass filled nylon scales over a 420J2 stainless steel liner InterFrame and solid glass filled nylon back spacers. We assemble the handle with superior offset Torx® fasteners.

For professional use, we’ve added a seat belt cutter to the Carson Flipper, and a tungsten carbide window breaker at the butt. Automobile side windows shatter with one quick whack from the butt of the knife.

All components receive a tough tactical black coating. The Flipper can be pressed for fast one-hand opening, and creates a blade guard when open. We use our premium AUS 8 high-carbon stainless steel for the blades, which have Combined Razor-Sharp and Triple-Point™ Serrated edges to easily cut rope, cord, canvas, and vegetation.

All three models are fitted with our exclusive patented* AutoLAWKS™ safety, which automatically makes them into virtual fixed blades when the blade is opened and locked.

M16®-14ZLEK. The “Big Dog” M16 is a hefty 6.2-ounce knife with a 3.75″- long Tanto blade that is able to tackle virtually any emergency task. This larger model features a four-position clip, allowing carry on belts or webbing— tip up, tip down, left or right. Please note: These knives are not designed for tip-up in pocket carry.

Full professional features. Non-reflective black finish. Exceptional affordability. Kit Carson rides again. This is without a doubt the best tactical knife in the line of CRKT knives to hit the market in a long time.

Click here to order a Kit Carson M16-14ZLEK CRKT.com.

Video: Jigging and Shaping Knife Handle Scales

0

American Bladesmith Society master smith Steve Dunn demonstrates how to jig and shape knife handle scales in this video.

The tutorial was shot during the Slip Joint Folding Knife class at Haywood Community College in Clyde, North Carolina, on Dec. 3-7, 2012.

Learn more about knife designs, including handles, in 101 Knife Designs.

Video: How to Select a Milling Vise for Knifemaking

0

This demonstration on the selection and use of milling vises is by Dale Schafer, Machine/Tool Technology Instructor at the Washburn Institute of Technology. This was one of the demonstrations at the 3rd Heartland Hammer-In in Topeka, Kansas sponsored by the American Bladesmith Society and hosted by the Kansas Custom Knife Makers Association.


For more about knifemaking, be sure to pick up a copy of BLADE’s Guide to Making Knives. This second edition shows step-by-step the tools and techniques for making a knife.

Click here to order BLADE’s Guide to Making Knives.

Tips for Grinding a Blade

1

Editor’s Note: This is an excerpt from Murray Carter’s new book, Bladesmithing with Murray Carter. Click here to learn more from this renowned knifemaker.

The shape of the blade, or profile, must be precisely ground. Grinding is the operation of using files or other abrasives to mechanically shape the steel into a functional blade.

Grinding can be divided into two categories: grinding the blade profile and grinding the blade’s edges (secondary and primary).

Let’s talk about the profile. Grinding a forged blade’s profile can be done with a variety of tools. Heating the blade via friction is not a big concern because this grinding is done prior to heat treating (annealing, quenching and tempering). As you may know, the blade needs to be shaped after a pattern or template. At this stage that template is scribed onto the billet of steel that is to become your knife.

Place the pattern so that it most appropriately covers the billet in relation to the thickness and tang. Be careful on full-tang knife billets to orient the template the correct way. I once made the mistake of switching the tang end of the billet for the blade end and wound up with a blade with way too much taper.

Once the template is in place, secure it with a pair of locking pliers or strong clamps. Any sharp-pointed tool that is harder than the annealed steel will scribe (scratch) lines onto the billet. Trace around the template completely. Examine it before you remove the clamp(s) to make sure you can see the scribe lines clearly. Examine it again, checking it against this list:

* Are the lines clear and not making little “train tracks?”

* Is the blade/tang junction exactly where it should be?

* Is the blade where it should be?

* If you have made a mistake scribing the lines, you can lightly grind the surface and scribe again, but you will now be committed to grinding and polishing the flats of your finished blade.

Also remember that, on a laminated billet, if you grind steel from one side you really ought to grind the same amount from the other side as well, or the steel core will no longer line up in the middle. For blades
that are meant to have a forge finish or a hammer-forged finish, these options will no longer be possible, so take great care when scribing lines on a billet.

There are several methods for removing the excess steel from the billet to produce the perfect profile.

* Steel shears

* Cut-off wheel

* Band saw

* Drill press and hack saw

* Belt sander

* Bench grinder

* Kaiten toishi

As the smith is cutting out or grinding the blade profile, the scribed lines, which should be clearly visible, are the guide. As soon as you are so close to the lines that you are actually touching them in places, it is necessary to employ another “micro observation” technique to be in full control of the profile.

In a good source of natural light, hold the blade at eye height with the flats of the blade horizontal. Instead of focusing your attention on the flats, look closely at the outer edges of the blade. If you hold the blade with the point towards your eye, the spine of the blade should look compressed into a few millimeters.

Compressed like this, every high or low spot on your scribed line will be evident. Similarly, every line on the outer profile of the blade should be examined this way. In the pattern or template you used, every line should be well defined and with a purpose. Ask yourself if the lines you are now looking at were meant to be perfectly straight, curved or pointed. Pinpoint trouble areas, then attempt to grind in a way to affect only those areas and re-examine.

At this stage, the blade should be at 97 percent of its final profile. The other 3 percent will be removed in the final polishing stages.

Click here to get 40% off Bladesmithing with Murray Carter and take the next step in the knifemaking journey.
Advertisement

Must Read Articles

Read this before you make a knife

Knifemaking 101 – Read This Before You Make a Knife

  by Wayne Goddard My experience has taught me that there's nothing like digging in and getting started. I've often said the hardest part of the...
how to forge damascus steel

How to Forge Damascus

Advertisement
Advertisement