Knifemaking

Knifemaking is the building of a knife, which includes the blade, handle and other accouterments. Blades are made by either removing metal from a steel blank via a grinder – known as stock removal – and the forging to shape of hot steel into a blade in the process known as bladesmithing. Other parts, including bolsters, guards, pommels, etc., are needed to complete the finished knife.

Featured Knives – – Knife Collecting – – Tactical Knives – – Survival Knives

Robertson’s Maker Market Matrix: An Explainer

The author’s system is designed to help you accurately price custom knives.

After I wrote a recent BLADE® article on custom knife pricing, editor Steve Shackleford suggested I write a follow-up on the system I use to price custom knives—Robertson’s Maker Market Matrix or RM3. I wrote it to provide a basic guide for each collector or maker on how to do their own pricing. You can find many examples of weighted score tables with a quick Internet search.

A collection or business is a very individual thing. The research required to create a successful Matrix for either one depends on the individual doing it. Let’s dive in.

Market Position

A maker’s position in a market is not always apparent. While in graduate school, I wrote a paper on the impact of pricing and how it can apply to products. As a custom knife dealer, I was looking for a business advantage. I applied the findings in my paper to my business.

I opened my copy of KNIVES ’92 and, using a weighted score table, started to compare makers I found in the book’s index. Initially, I placed the knives in recognized categories, for example, hunters, fighters, bowies, tactical folders, etc. I wanted to compare similar knives/apples to apples. Each category had several hundred entrants.

My goal was to create a top-third, middle-third and bottom-third strata. This is where the weighted aspect of the table comes in. I developed essential criteria, such as quality of work, demand in the primary market, demand in the aftermarket, materials used, delivery time, awards and other gauges. Once I established the criteria, I gave each criterion an importance weight.   
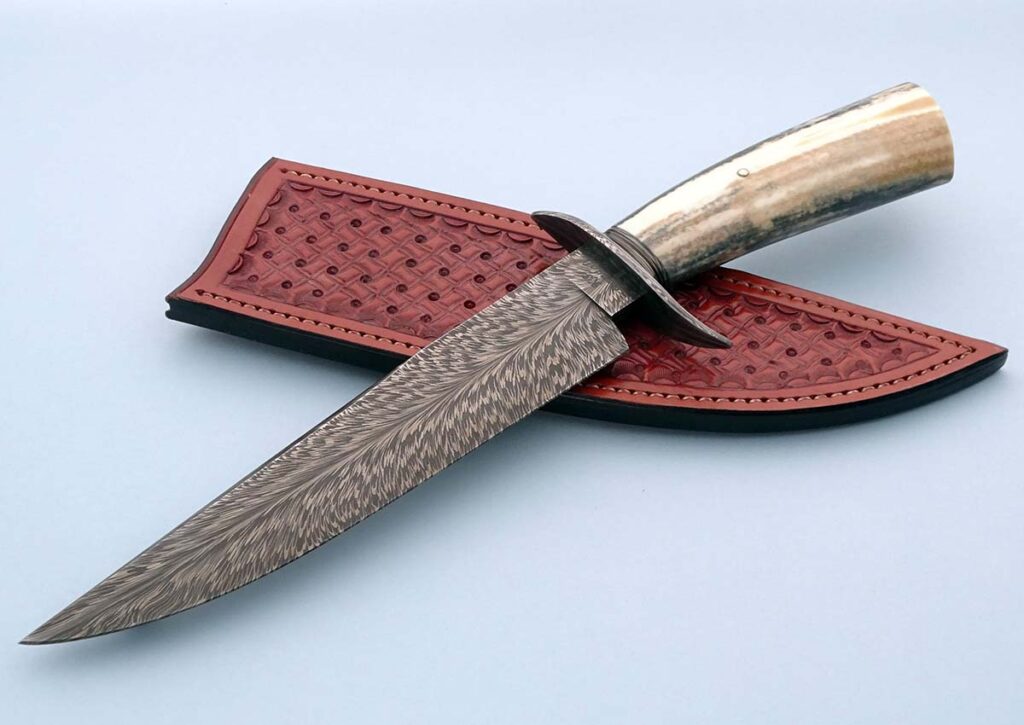

Custom Randall-Orig-Forged-Dam-Fighter-lg

Maker: Steve Randall  
Model: Feather Damascus Fighter  
Blade Length: 8”
Overall Length: 14”
Blade Steel: Feather Pattern Damascus 
Guard Material: Feather Pattern Damascus  
Handle Material: Ancient Walrus Ivory  
Author’s Comments: “Steve is the quintessential ABS master smith. He is versatile, inquisitive, loves a challenge and always strives for perfection in every aspect of his knifemaking.” (Robertson’s Custom Cutlery image)


After the Matrix determined the maker’s position in the strata, the ultimate goal of the RM3 took shape in determining which makers’ prices accurately reflected their position in a particular market sector. My research showed that hundreds of makers’ prices were above their position in the market. In other words, many of these makers who were in the second strata were asking first-strata prices. The same was true for third-strata makers asking second-strata prices. The main reason for this is that the makers asked their knifemaking friends to price their knives.

Knifemakers are not knife buyers and, as such, generally do not have a real sense of what knives should sell for. This is especially true if they don’t know their market position. Additionally, asking your competitors/fellow makers to price your knives is not a recommended business strategy.

Among other things, one aspect of the RM3 I was surprised to find is that it identified makers who offered value pricing. At first glance, many people mistakenly think this means the least expensive price. Instead, given the maker’s position in the market, a value price provides the buyer value regardless of the price tag. The makers who came to my attention were those pricing their knives commensurate with the pricing in lower strata, e.g., a first-strata maker asking for a second-strata price.

Blade Game

When knife shows or knife sales are slow, the blame game begins. The reasons for the slowdowns usually center around the show promoter not doing the job. The economy is a favorite reason, along with the weather, lighting and position in the room. A maker once told me his sales were slow because he was facing a wall. Note that we were in a square room; everyone was facing a wall. What seldom, if ever, is brought up as a reason for slow sales is the maker’s prices.
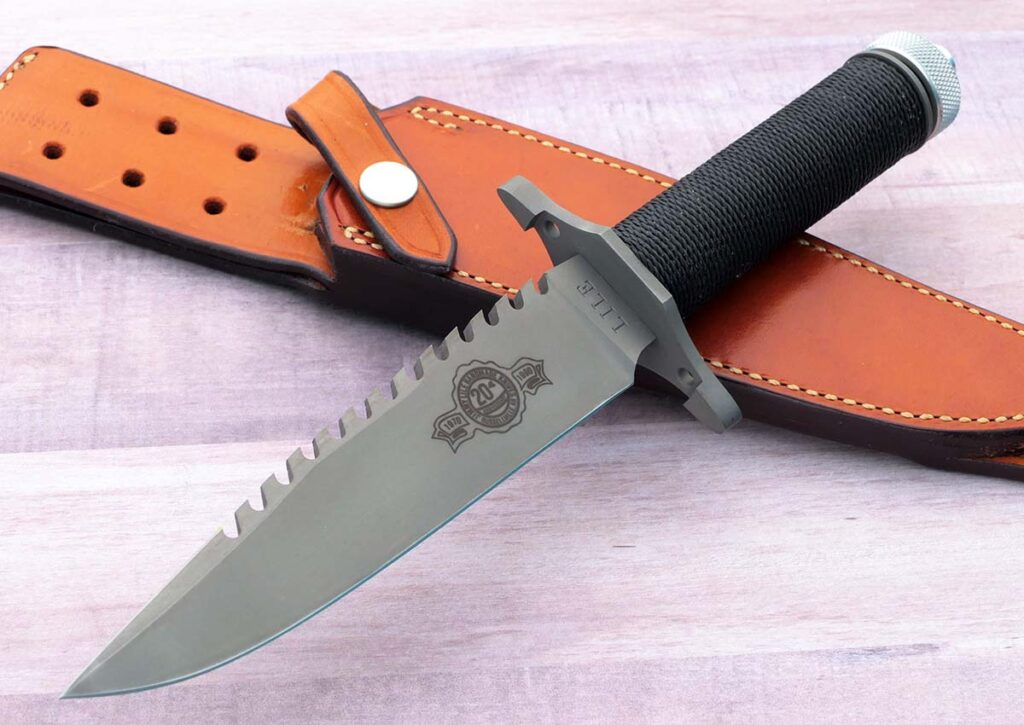

Custom Lile-20-Anniv-Sly-II-Tactical-Fighter-Blade

Maker: Jimmy Lile 
Model: 20th Anniversary SLY II Fighter 
Blade Length: 6”
Overall Length: 10.5”
Blade Steel: 440C stainless
Blade Finish: Bead blast 
Guard Material: Stainless steel 
Handle Material: Aluminum tube w/cord wrapping 
Author’s comments: “A BLADE Magazine Cutlery Hall-of-Fame® member, Jimmy did more to introduce the knife world to the tactical fixed blade than any other custom knifemaker. This young infantry lieutenant saw a Rambo movie and it changed my world.” (Robertson’s Custom Cutlery image)


Very few people will tell makers their prices are too high, as makers can be touchy about their pricing. At the same time, few makers ask collectors or buyers what they think of their knives. This interaction is a prime opportunity for a maker to work on his or her Matrix. Further, this is an opportunity to educate the collector on why the maker’s knives are priced the way they are, and to give the collector a chance to work on his or her Matrix.

I cannot overstate how vital this flow of information is for both the maker and the collector. For the past 30+ years, at every show I have attended I have heard, “Les, come and look at my knives and tell me what you think.” I have the utmost respect for the makers who ask me to do that. It can be daunting for a maker to ask someone to critique the maker’s knives and prices. A quick “good job” may be nice for the maker’s ego, but a critical examination of the work and pricing will ultimately improve the maker’s knives and bottom line. 

Hype Cycle

The Hype Cycle occurs when a custom knife market sector takes center stage. In 1988, interframe folders were all the rage—many sold for over $10,000 each. In 2001, I bought one of the same knives for $600 at an auction. The original sale price was $14,000. What happened? Answer: the Hype Cycle. The hype drove up the prices, and when the hype went away, the prices crashed. The Hype Cycle is a Matrix killer as prices become skewed to the point that they are unsustainable. 

Whether you’re a collector or a maker, the Matrix can benefit you. Identifying the maker’s position in the market aids in an appropriate price, thus increasing sales for the maker. At the same time, it gives the collector a chance to sell or trade a knife at a fair price in the aftermarket, as it is in the aftermarket where collectors pay to go to school. 

Custom knife markets are small cycles inside of larger cycles. New criteria will always enter a Matrix. Consequently, both makers and collectors must be sensitive to the ever-changing markets. Retirements, new materials, awards, bad reviews and other factors can all impact pricing.

R&T

Reading this, some may think the RM3 is a quick and easy solution for pricing knives. I assure you, it is not. The amount of research and time you put into your Matrix will directly affect your ability as a collector or as a maker to identify the maker’s position in his or her market. It also will give valuable insight as to whether the maker is offering value pricing. Makers will gain useful knowledge on how to price their knives correctly for their position in the market, helping them eliminate the blame game.
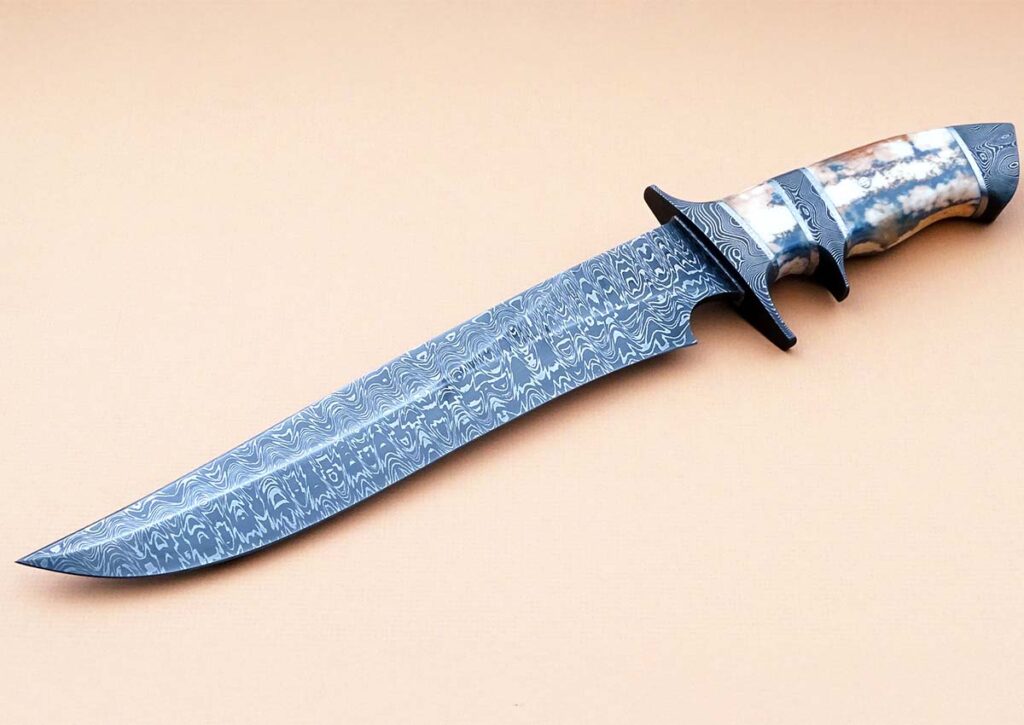

Custom Broadwell-Damascus-SubHilt-Ivory-Blade-Article

Maker: David Broadwell   
Model: MLR Sub-Hilt Fighter 
Blade Length: 8”
Overall Length: 14”
Blade Steel: Wolf’s Tooth Pattern Damascus Guard, Sub-Hilt and Pommel Material: Wolf’s Tooth Pattern Damascus
Handle Material: Ancient Walrus Ivory  
Author’s Comments: “Dave has been making some of the finest sub-hilt fighters for over 40 years. His knives are the epitome of the 4 F’s; Fit, Finish, Form and Function.” (Robertson’s Custom Cutlery image)


More On the Robertson Matrix

How do you give what you call an “importance weight” to each criterion in a Matrix? What makes specific criteria more important than others?
ROBERTSON: One criterion that has moved up my list and now carries more weight is customer service. We deal in so much poor customer service in our everyday lives. We don’t need this in our hobby. I am still amazed at the number of clients who tell me they have emailed or called a maker, often several times, with no response. Everyone is busy but it takes literally 60 seconds to respond to an email acknowledging receipt and indicating a response will be forthcoming asap. Those makers who don’t respond in a timely manner are telling you it is about them and not you. If they are making it difficult for you to give them your money, don’t. 

What makes the ratings for your criteria change?
ROBERTSON: Actually, it is the ratings of knife organizations that have caused me to change the weight the ratings carry in my criteria. When I first started in custom knives, to be a Knifemakers’ Guild voting member carried a lot of weight in the knifemaking community. Today the Guild is more of a club, though still a good idea that provides insight and help for makers. For me, at least, if a maker tells me he or she is a Guild voting member, that mostly tells me the maker is serious and has shown improvement in his or her knifemaking skills over the years, but it does not carry the weight in my criteria it once did.

How often do you update the ratings, and why?
ROBERTSON: The custom knife market is never static and is always evolving.  This evolution demands that weight associated with each criterion evolve as well. The weight I associate with a particular maker changes with the maker’s ability to incorporate the changes the collectors want, be it materials or design elements.

How often do you change the criteria themselves, and why?
LES ROBERTSON: I’m generally one-to-two years ahead of where a market sector that interests me is going. Given this extended lead time, I often have to account for new information and tweaking of the weight within a particular criterion or the criterion itself. Perhaps the most difficult aspect of this is to not put too much weight into a criterion due to my personal biases. In other words, just because a particular style of knife is my favorite does not mean the majority of other collectors feel the same way. I try to take my feelings out of the equation and I am not always successful. The Matrix is not an exact science.
More On Knife Collecting:

Leap Of Faith Knifemakers: From Home Shop To Factory

0

How two U.S. knifemakers successfully transitioned from home shop to factory.

Ever wonder why some custom knifemakers decide to take the leap from the rarified air of being a sole artisan to the crowded arena of factory fare? Sometimes the answer is easy. For instance, in 1999, BLADE Magazine Cutlery Hall-of-Fame® member Chris Reeve switched his custom shop over to a micro-manufacturing outfit in Boise, Idaho, simply because he couldn’t supply enough of his popular Sebenzas to a thirsty knife-buying public. That one move catapulted Chris Reeve Knives (page 26) into a successful American manufacturer of folders and fixed blades.

We thought the practice of switching from shop-to-factory, and the reasoning behind such a move, to be an interesting one, so we sought out a couple of like-minded makers from two different genres to bring you an inside look at such a move.

Long Road Of American Knife Manufacturing

Daniel Winkler never planned on producing factory knives, but when a government contract to aid the troops fighting in the Middle East came along, his love of country won out. He had, however, made a name for himself long before that. Winkler built his first knife in high school shop class and still has it among the knives he has archived. In the ensuing years he began gaining popularity among members of the black-powder and knifemaking communities. In the late 1980s he teamed up with partner Karen Shook, whose sheaths greatly complement his custom period knives to this day. In 1992 he forged blades for the hit movie The Last of the Mohicans starring Daniel Day-Lewis, which enhanced Winkler’s popularity even more.

Daniel Winkler went from a one-man knifemaking shop he used from 1992-2006 in Blowing Rock, North Carolina, to the 35,000-square-foot facility he and partner Karen Shook operate in Blowing Rock today.

Simply stated, Daniel Winkler is more than a knifemaker, he’s an institution. But it was a long road with a lot of steps along the way. “My first shop was in the hall of my house. I would clamp knives to the stairs and file them to shape,” he recalls. “I graduated to a garage and bought a 1-by-42-inch belt sander. My first forge was made from a truck wheel and a vacuum cleaner. I used charcoal and a piece of railroad rail for an anvil. I still have that anvil, too.” Winkler says his biggest challenge during those early days was “a lack of time, as I had to work a full-time job—and mostly a lack of practical knowledge.” As his popularity grew so did his equipment and capabilities as a master forger, but that would bring change as well.

“I never really wanted to make factory knives,” Winkler opines. “Back in the mid-2000s I was contacted by members of a Special Operations group. They were not happy with the edged equipment they were getting and asked if I would help them get better designed and higher functioning equipment. Initially, I was going to help with the design and development and contract another manufacturer to make the tools. What I found was other people wanted to do things their way and not adapt their manufacturing methods to how I wanted operations done.

“Karen and I discussed the situation and decided whether we were going to be involved with making edged equipment that could very realistically mean life or death based on the performance of the equipment. We decided that no compromise was worth accepting, so we started our own limited production company. We called it Winkler Knives II since we were still making our hand-forged pieces. We successfully made the requested equipment, and [Winkler Knives II] started growing by word of mouth in the military community. As we grew in professional circles, the public with an interest in Tier-1-level military uses found us. Our involvement was verified in a book written by a Navy SEAL and the Sunday edition of The New York Times. Business took a big leap after that.”

Making The Leap Into Knife Manufacturing

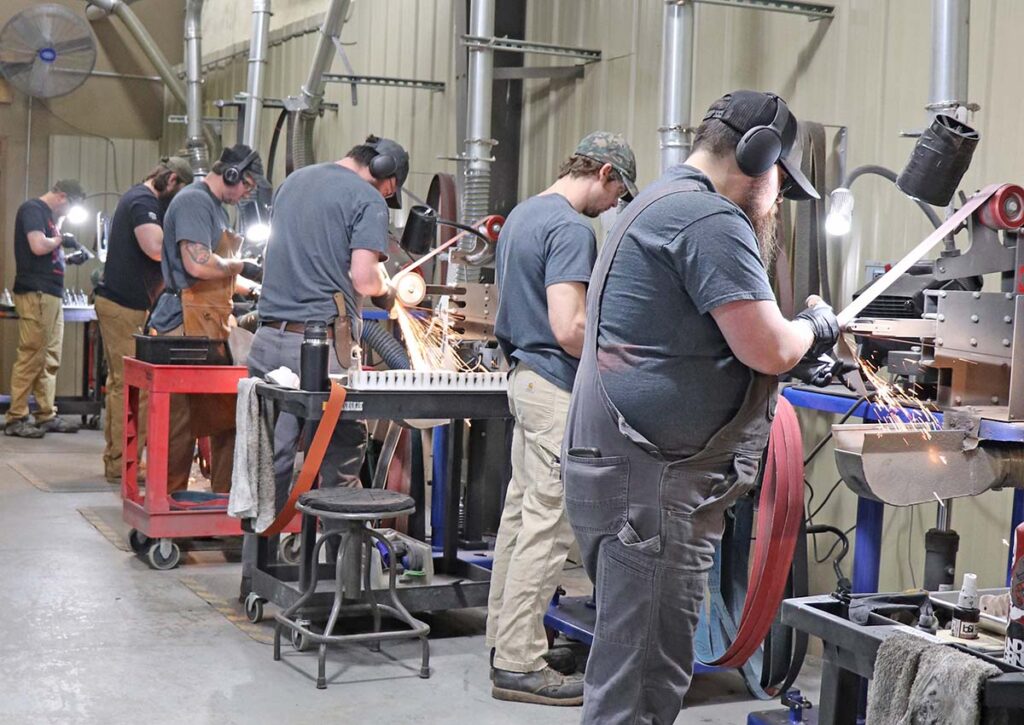
Sparks fly on the grinding line in Winkler’s Blowing Rock, North Carolina, facility. The company employs one part-time and 28 full-time employees.

“My first shop was my one-man forging/grinding shop. I hired two part-time staff to assist in handling it. It was a very tight space,” Daniel notes. “From here I added additional grinders and rented a small space in a warehouse. I did the steel grinding and heat treating while Karen worked on finishing. The first models were two Combat/Breaching Hatchets—one for Naval Special Warfare and another for Army Special Operations. That was in 2004-2005.”

Today Winkler Knives has exploded in size to a 35,000-square-foot facility with one part-time and 28 full-time employees. Daniel credits buying a water jet to cut production costs, hiring the right people, and creating an environment for lasting and satisfying jobs.

“I have a rule we adhere to,” he observes. “Any changes we make must make the product better in performance and/or quality, and make the operation safer for our employees.” It is a dictate that continues to make Winkler Knives a mainstay in the business of all that cuts.

Paying Dues

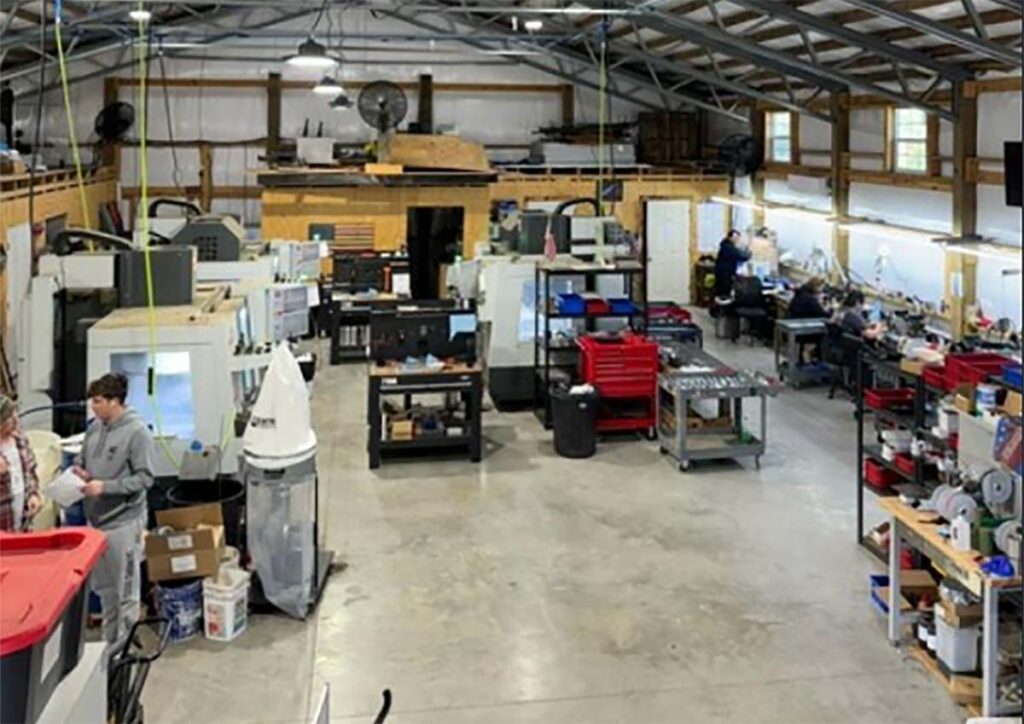
In 2019 McNees Knives went from a 400-square-foot shop to today’s 3,500-square-foot factory. Among the hot sellers for McNees are the MAC2 integral-lock folders.

United States Marine Corps veteran and devoted outdoorsman Jonathan McNees of Vernon, Alabama, has always been a knife fan, and when he got drawn into the world of custom knifemaking on the internet he was hooked for good. “I started making knives in 2008 after discovering online forums where people were discussing making knives in their personal garages and the like. Before that,” he remembers, “I really had no idea people were doing that—not at that level, at least.” Finding some brands he’d never seen before, like Strider Knives, led him to locating the forums, he added.

“My first shop was a 400-square-foot pole barn in my backyard that started with an extension cord run from the house to power it,” McNees reveals. “I cobbled together my first 2-by-72 grinder using some ‘no weld’ grinder plans I picked up. It was the epitome of a ‘Frankengrinder’—a bench grinder for a motor and a plastic lawnmower wheel as a drive wheel, but it got the job done. I ground hundreds of knives on it before I bought a real grinder. The most difficult thing in the early days, aside from learning the hand-to-eye coordination on the technical stuff, was getting my name out there and building a reputation. I had to be aware of my place in the food chain and pay my dues.

“My breakthrough moment to switch to factory knives came from looking at my work from a business perspective. I always tried to work fast but no matter how fast I got, the business was never going to scale with me building customs by myself. I realized I not only wanted to be a craftsman but I also wanted to build a business. I went to production in 2019. I realized I couldn’t make the kind of impact in the industry I wanted to by just flying solo doing customs. I was probably putting out between 200-to-300 knives a year as a custom knifemaker.

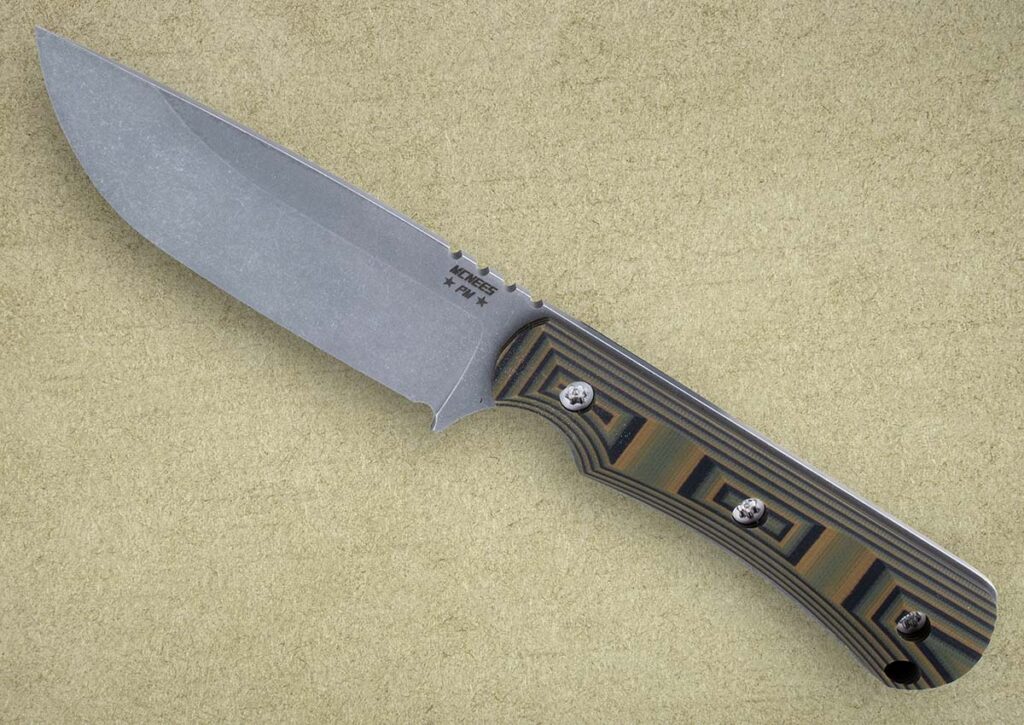
The McNees Knives Ridge Runner won the BLADE Magazine 2024 Fixed Blade Knife Of The Year® Award at last year’s BLADE Show. The 3.7-inch blade is CPM 3V carbon steel and the handle is G-10. MSRP: $312. (Jocelyn Frasier image)

“The first step into production was using U.S. OEM shops to do all the machining and grinding work,” he continues. “I hired two people—one primarily ran our laser, which we did non-knife projects with to help with cash flow, and the other I taught to do all the hand fitting and assembly. I helped where needed on the production but mostly continued to make customs during this phase.” All this continued to be done in the 400-square-foot shop.

“One big step forward came in 2021 when we moved and built a 3,500-square-foot shop and bought our first CNC mill,” Jonathan states. “Since then, we’re up to seven full-time employees plus myself, and my wife has come to work full time in the business for a total of nine. Our bread and butter is our framelock tactical folders, but we also have a good start on a fixed-blade line with three new models added this year.

“We should finish with 3,000-to-4,000 knives produced this year, but our biggest recent accomplishment is a great increase in production numbers thanks to getting a lot of processes dialed in and getting a really solid team in place,” he observes. “We have a new folder coming out next year that is based off one of my most popular custom designs, so we’re really excited about that. We plan to continue to scale and grow as much as we can. We love this industry and want to provide a positive influence.”

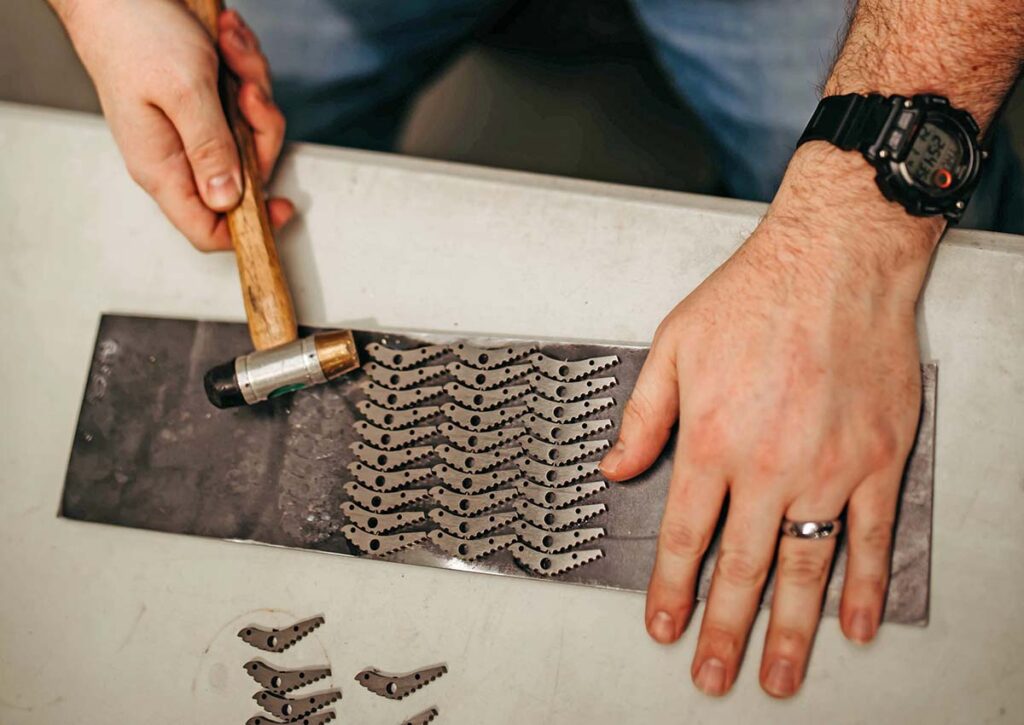
Parts for a McNees Knives folder are removed from the plate used to surface grind them, a far cry from the days when they were done by hand.

Daniel and Jonathan are two custom knifemakers who made the leap to factory production for two different yet legitimate reasons, but both share the common commitment of making knives. They reflect the American dream in action and have done themselves proud.

More On Knifemaking:

Winkler Knives Overcoming Hurricane Helene

0

The Tar Heel Hurricane turned lives upside down, but North Carolina knifemaker Winkler Knives has proven resilient.

Hurricane Helene devastated parts of Western North Carolina, East Tennessee and other states this past fall. Among those damaged was the Winkler Knives shop in Blowing Rock, North Carolina.

Daniel Winkler estimated the monetary loss to his business from $500,000 to $600,000, though the biggest setback was the death of one of the company’s long-time employees, Steve Limbacher.

“He could not handle the stress and his heart just gave out,” Winkler wrote. “Steve is missed every day at Winkler Knives.”

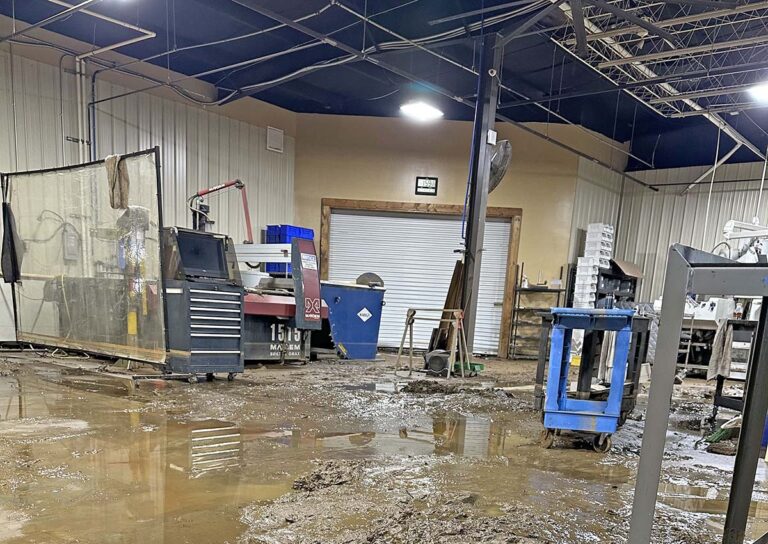
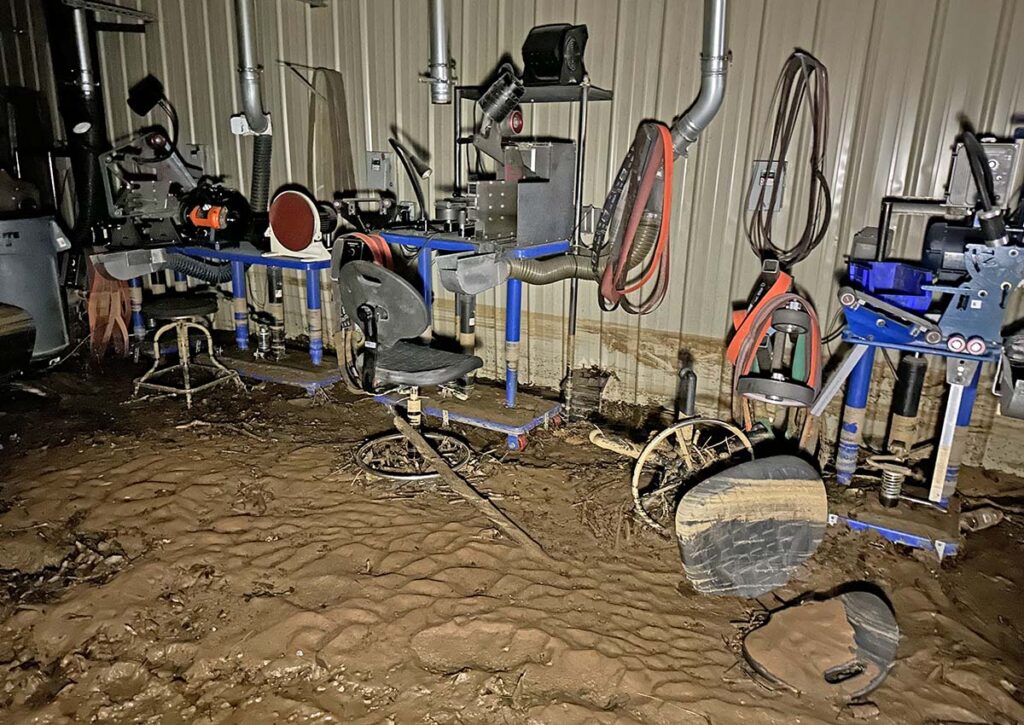
Up to 15 inches of water flowed through the Winkler shop from a creek adjacent to the structure, leaving behind one to 6 inches of mud. The company lost several machines, computers, printers, cabinets and shelves, carts and other daily use tools. Materials for handles, sheaths and other shop supplies were destroyed. Four large garage doors were damaged, as was all the flooring in the office and breakroom. All the office doors were lost.

Winkler Knives
One to 6 inches of mud were left at Winkler Knives factory requiring a extensive cleanup process.

For cleanup the Winklers bought a track hoe, dump truck and small skid steer, and also numerous hoses, pressure washers, wet vacuums, mops and scrubbers. In all, it took the full staff 2 ½ weeks to clean up the mess.
“However, compared to others in our area, we were just inconvenienced,” Daniel noted.

“Many others were devastated with lost buildings, vehicles and many lives. We are truly blessed.”

To aid those in one of the most severely damaged areas in North Carolina, through its fundraising efforts Winkler Knives presented a check for $13,018.75 to the Mitchelle County Development Foundation. The company also raised money for its own recovery efforts via tent sales of Winkler knives, tomahawks, axes and sheaths at Winkler Knives Actual on Nov. 30 and Dec. 2.

More On Winkler Knives:

Roadblocks to U.S. Knife Manufacture

2

Leading domestic factory companies outline barriers to producing knives in America.

The slogan “Made in the USA” carries a specific meaning across the globe. American knife manufacturers tout that aspect of their operations with justifiable pride. Still, they face challenges in the arena of worldwide competition, constantly seeking methods and management that offer the best opportunities for success.

In addition to the inherent competition related to the actual quality of their finished products—the attributes that compel the buyer to choose their knives over that of a competitor—American cutlery manufacturers often find themselves up against a foreign-government-subsidized or bankrolled competitor. Trade barriers may prevent their products from reaching a broader customer base, and the shifting costs of labor, materials and production demand attention.

Export Hurdles

To remain successful in today’s competitive knife marketplace, Anne (left) and Tim (right) Reeve of Chris Reeve Knives focus on consistency in the company’s brand and models, as well as uncompromising quality in materials, designs, workmanship and customer service.

“One major challenge is the cost of distributing products overseas, particularly to the European Union,” related Curtis Iovito of North Carolina-based Spartan Blades. “The combined impact of Value Added Tax [VAT] and customs duty can exceed 21 percent, and in some countries it is even higher. These additional costs ultimately get passed on to the consumer, making it harder to remain competitive.”

The Spartan experience is not unique, and in order to address the issue American knife manufacturers naturally gravitate toward the domestic consumer.

“One of our strategies is to focus on the American market,” Curtis advised, “where consumers value high-quality products and excellent customer service. We optimize our manufacturing processes for maximum efficiency, allowing us to control costs as effectively as possible.”

Such an inward perspective is driven both by access to markets and by an acknowledgement of the barriers that exist in global trade.

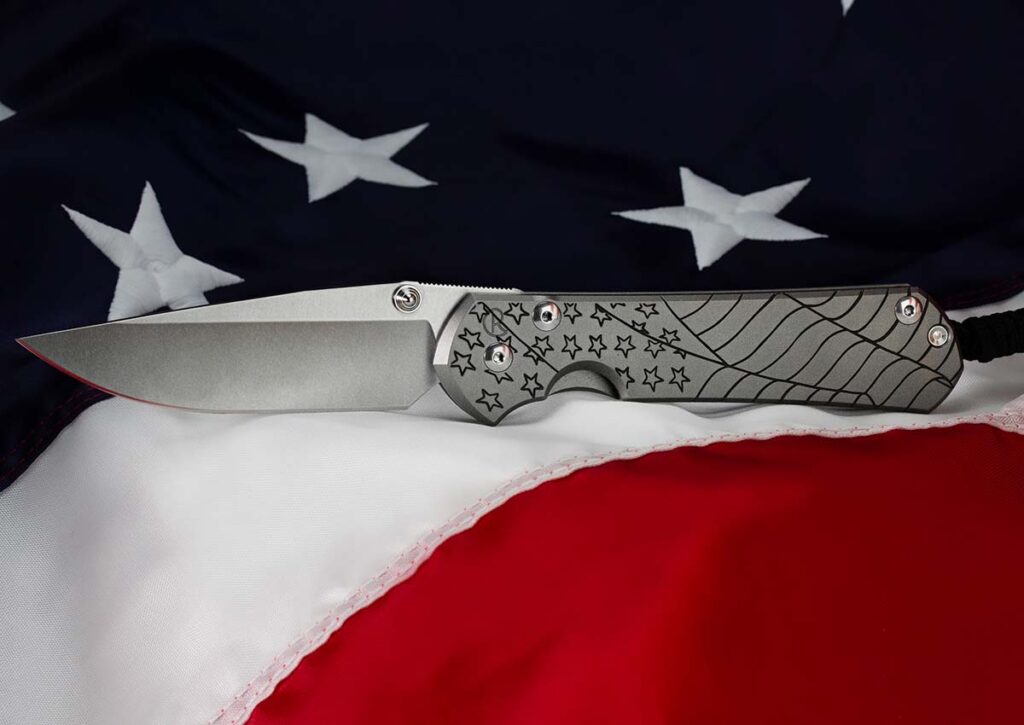
Illustrative of Chris Reeves Knives' approach to the market is the most American-looking of the U.S.-based manufacturer’s knives: the Sebenza 31 CGG Forever Flag Drop Point. MSRP: $550.
Illustrative of Chris Reeves Knives’ approach to the market is the most American-looking of the U.S.-based manufacturer’s knives: the Sebenza 31 CGG Forever Flag Drop Point. MSRP: $550.

“In regard to stuff abroad, we source everything in the U.S., period,” asserted Ernest Emerson of Emerson Knives, Inc., located in the Los Angeles, California, area. “We don’t get steel screws or handle materials except from U.S. suppliers at this point, so availability of materials doesn’t affect us. Also, 99 percent of our product is sold domestically, so we don’t have any dealers set up in Europe, although there is a tremendous fan base for us there.”

The benefits of an established brand and loyal following are hallmarks of the success story at Chris Reeve Knives, located in Boise, Idaho, as well.

“We are in the very fortunate position of having established a legacy brand many years ago and are supported by an incredibly loyal customer base,” explained Anne and Tim Reeve. “The market has changed considerably in recent years, but we have remained stable. To keep competitive, we focus on consistency in our brand and our models and uncompromising quality in materials, designs, workmanship and customer service.”

Dangers Abroad

Domestic competition is welcomed among American knife companies. Consumers are invited to question, evaluate and commit with their dollar at home. However, in the wider world there are obvious signs that the playing field is far from level when it comes to price points.

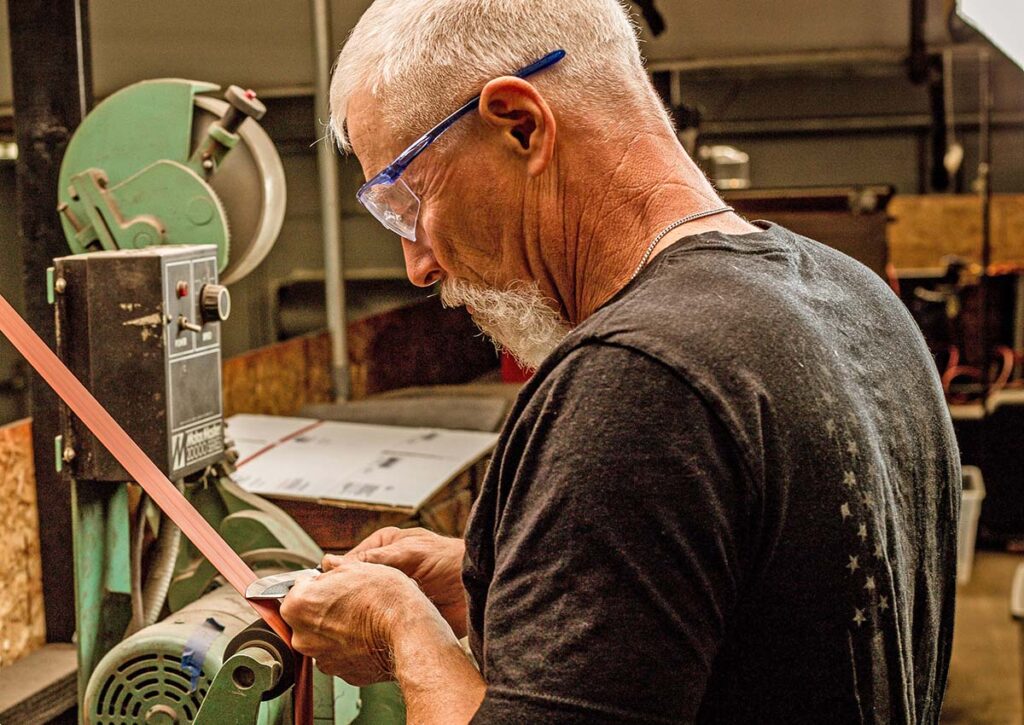
Known worldwide for his custom as well as his factory knives, Ernest Emerson—putting blade to grinding belt here—said he finds Chinese knife companies and their advantages a real danger to the knife industry overall. “They are ruthless,” he opined, “and their endeavors inside our industry are the same exact game plan as the Chinese government is using across all U.S. industries—break them down, undercut them, put them out of business.”

Further, the encroachment of foreign knife companies into the American market with the economic power and financial backing of their government’s bankroll is troubling—and among these foreign companies no others stand out more prominently than those headquartered in the People’s Republic of China.

“A very real danger to our industry is the Chinese knife companies,” Emerson declared. “They are ruthless, and their endeavors inside our industry are the same exact game plan as the Chinese government is using across all U.S. industries—break them down, undercut them, put them out of business. They are funded by the Chinese Communist Party, and don’t get me wrong, the product is good. But what happens is they come in at prices just under [Emerson], Buck or Spyderco. So, in the consumer’s mind they may reason that the Civivi or WE knife is $50 cheaper and buy that knife. It’s a shame because we have seen companies that have been in business for years go out of business. If you take an 18-to-25 percent hit to the bottom line, it affects you like crazy. That’s millions in revenue.”

Iovito adds to that perspective.

“There are two main disadvantages,” he said. “Increased competition from Chinese-made products and rising concerns about counterfeiting. The lower labor costs and government funding available to manufacturers in China create a significant competitive gap. Additionally, counterfeits have become harder to distinguish from genuine American-made knives, especially as platforms like Alibaba make it easier for counterfeiters to distribute their products. The situation is compounded by foreign-government-backed knife companies with substantial marketing budgets, which make it difficult for smaller U.S. companies to compete at sub-$150 price points. We’re also seeing foreign interests penetrate U.S. industry organizations through donations and sponsorships aimed at market expansion.”

At Chris Reeve Knives, the owners acknowledge the market conditions that drive profitability.

In terms of state and local taxes and restrictions, the Chris Reeve Knives business environment in Idaho seems to be better off overall than some other domestic knife manufacturers. “We are fortunate that Idaho is a good place to do business,” Anne Reeve noted, “and there are no particularly difficult restrictions.”

“It is becoming more and more expensive to produce knives or anything else in the USA, but we are grateful that we established ourselves as much USA-made as is possible many years ago,” Anne commented. “Labor costs have skyrocketed and all materials have increased. We monitor costs closely and negotiate as much as feasible with our suppliers. We focus on innovative manufacturing processes, employee training and scrap reduction without compromising quality.”

Hence, keeping costs contained in light of wage pressure, materials availability driven by demand, and other factors that are basic for any business—including utility costs, equipment maintenance, upkeep and upgrades, and the retention of skilled and even unskilled workers—is always a priority. The companies who manage such challenges best are those that survive and prosper.

Trade Protection

However, where is the pressure point or the point of relief when it comes to foreign competition? How does the American knife manufacturer remain competitive and keep each of these critical components in fragile balance? Perspectives on trade protection are somewhat varied but they may well have a purpose in the overall economic scheme of things.

“We see an average Total Import Tax of about 22.4 percent on folding knives and 23.6 percent on fixed blades,” Iovito related. “Often it is much higher. There aren’t many solutions to this issue other than competitive tariffs and trade agreements. The VAT and tax outlay by our dealers can almost double the price of our knives in the European Union. Additionally, the dealer doesn’t receive a refund on the VAT until the knives are sold. This effectively disincentivizes the stocking of American knife brands.

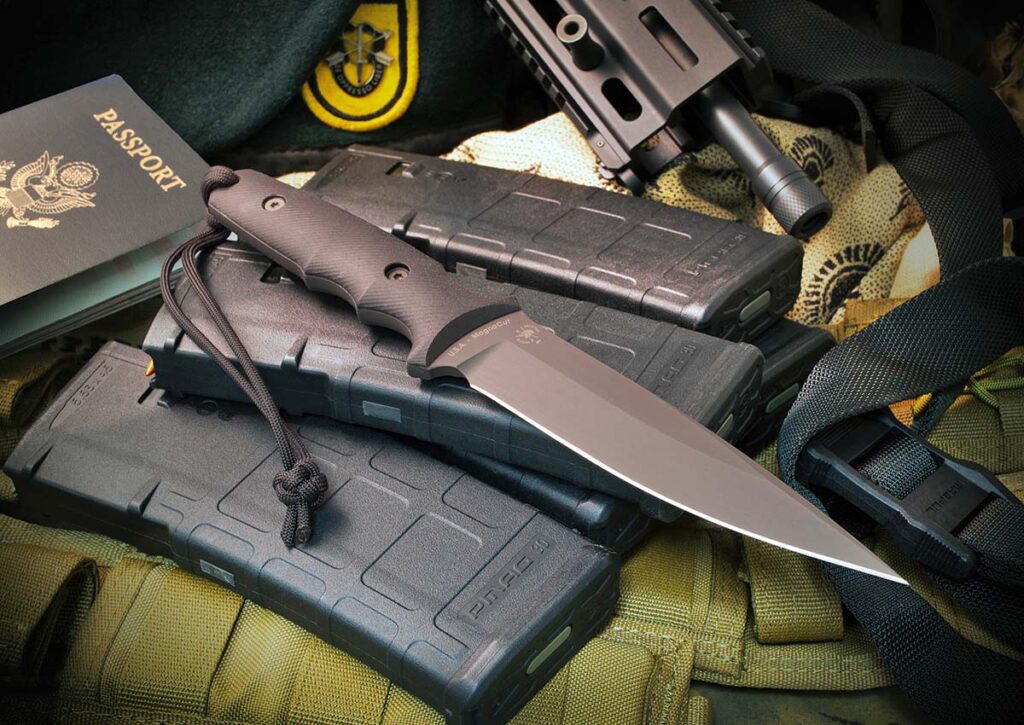
Spartan Blades won its first-ever BLADE Magazine Overall Knife-of-the-Year® Award last year for the full-tang Clandestina fighter designed by BLADE Magazine Cutlery Hall-of-Fame® member Bill Harsey. The 5.5-inch blade is flat-ground CPM MagnaCut stainless steel. It is also available in a flat-dark blade finish and canvas Micarta® handle. MSRP: $360.

“I believe in maintaining ‘Most Favored Nation Status’ with our allies,” Curtis added, “but tariffs could still be adjusted to ensure fair competition. Ideally, tariffs should be leveled in a way that provides an advantage to U.S. manufacturers, helping to balance the playing field. For those countries that are international trade competitors, I feel their products should be taxed at an equal rate or in a manner that places them at a competitive disadvantage.”

Fair is fair, say Anne and Tim.

“Tariffs hurt the international dealers and, as a result, the end users. The dealers often work on reduced profit margins simply to sell the product at an affordable price. We are fortunate to be an accepted luxury brand and, without sounding arrogant, our international end users generally have higher disposable incomes. There is little that we can offer by way of incentives or discounts to combat tariffs.

“First reaction [to U.S.-imposed tariffs] would say that reciprocity would be fair,” the Reeves concluded. “We should charge as they [other nations] charge us. However, the reality is that high tariffs on incoming knives hurt our industry by making everything more expensive. Tariffs are such a political thing, and a general rise in tariffs is not a good answer to the problem.”

Domestic Taxes & Restrictions

“The Los Angeles council passed a law that the minimum wage will be $30 per hour by 2028,” Ernest Emerson noted. “They are sneaky in that they apply this only to groups like ‘hospitality workers,’ but the truth is that any worker can look at what they are currently doing and say, ‘I can fold bedsheets for $30 an hour instead of doing this.’”

In addition to foreign competition, there are restrictions right here at home that challenge the knife manufacturer on a daily basis. That situation is particularly true for Emerson Knives, Inc. Ernest says the continual pinch of California’s local and state taxes, restrictions and legislation impede his company’s performance. But don’t jump to the conclusion that simply relocating to another state holds the answer. Emerson is committed to his employees, many of whom have been with him for more than 25 years. They have families and deep roots in California and can’t relocate to a more business-friendly state.

Still, Ernest bristles at the simple fact that taxes are levied against every piece of equipment on his facility’s floor. He must follow rigorous guidelines on disposal of byproducts, pay fees for parking, comply with building restrictions, and fork over a fee for a license to operate his laser machines. All the while, he is aware that other companies operate under the radar, ignoring these state-imposed requirements.

“The Los Angeles council passed a law that the minimum wage will be $30 per hour by 2028,” Ernest noted. “They are sneaky in that they apply this only to groups like ‘hospitality workers,’ but the truth is that any worker can look at what they are currently doing and say, ‘I can fold bedsheets for $30 an hour instead of doing this.’ That means that everybody has to pay $30 an hour to retain their workers. Imagine what the cost of a Big Mac will be when fast food workers at McDonald’s are paid $30 an hour.”

In contrast, the Chris Reeve Knives business environment in Idaho is apparently better overall.

“We are fortunate that Idaho is a good place to do business, and there are no particularly difficult restrictions,” Anne remarked. “One of the biggest issues for small businesses is high rates of taxation. I understand that taxes are necessary, but I would rather invest in my employees and equipment than see my tax dollars spent unwisely. The American drive to make high quality goods is still very much alive! We are fortunate to have employees who are proud to work for an ‘all American’ company and strive to make the very best. Most of our market is in the USA and our customers appreciate the fact that we are so doggedly ‘Made in Idaho!’”

Anti-Knife Laws

For years, the issues surrounding restrictive knife laws have influenced American knife manufacturers, from the types of knives they make domestically to their ability to import or export. These days, some softening has been experienced, particularly due to the efforts of groups like Knife Rights and the American Knife & Tool Institute (AKTI), which have challenged some laws in court or successfully lobbied to keep others from reaching the books at the federal or state level.

“Our knives don’t gain too much attention in anti-knife legislation,” Anne said. “The one-hand-opening issue that caused so much concern some years ago has subsided. AKTI and Knife Rights have done yeoman’s work in overturning dated and irrational legislation, and we are happy to support them.”

Interstate commerce remains solid for Emerson as restrictive knife laws appear to be on the wane.

“Knife restrictions state to state don’t really affect us,” he commented. “I’m not aware of any state that we can’t ship to. Thank goodness for AKTI and Knife Rights fighting the good fight for us. I’ve always told everybody that we have to fight for the 2nd Amendment whether you are a gun person or a knife person. No matter what, where guns go, knives are soon to follow.”

When it comes to tariffs, Anne and Tim Reeve recommend reciprocity. The USA should charge other nations as those nations charge the USA, the Reeves stated, though noting that “high tariffs on incoming knives hurt our industry by making everything more expensive.” Here Tim inspects a tray of folders in the Chris Reeve Knives manufacturing facility.

Iovito added a positive point of view.

“In the U.S., legal restrictions on knives are often based on a mistrust of citizens or as a way for a politician to appear tough on crime instead of addressing the root cause of crime in his district. However, I’m seeing positive change as lawmakers and the public recognize that most people carry knives as tools rather than weapons. As knife laws in the U.S. evolve, I’m optimistic about their eventual liberalization. While I won’t comment on laws in other countries, most of these laws tend to be reactive responses to broader societal issues.”

American Resilience

Considering the challenges of modern business and the complications presented, American knife companies have proven remarkably adaptable and resilient.

“The thing that has kept Emerson Knives, Inc., afloat,” Ernest explained, “is being the right size to be super flexible. We are small and every operation is done in-house, and I have worked with companies over the years to make smaller amounts of knives to fill orders. That way we don’t sit on ‘XYZ number’ of knives and wonder what we’re gonna do. Small businesses and shop owners really drive the average Joe in the U.S., and I’m proud to be a part of it.”

Read About Custom Knives:

Cool Customs: Pat Antuzzi’s Hand-Knapped Fixed Blade

When it comes to crafting a knife, Pat Antuzzi works one flake at a time.

“What I do is go back to the Stone Age,” Pat Antuzzi says of his knapped obsidian knives. He has been knapping blades for almost a quarter century.

In that time he has found the best of the best obsidian to be the royal Mexican variety from the state of Jalisco in Mexico, a variety that’s basically been mined out. He used the material for the blade of his straight-edged fixed blade, as well as Portoro marble from Italy for the handle. But it’s the royal Mexican obsidian itself and how it’s knapped that are the keys.

Pat Antuzzi

“Every indentation you see on the blade is one flake removal from [the obsidian], and if it’s done right, you’re going to see it one flake after the other, just like the ancients would’ve done it,” he explained. “It’s wicked sharp.”

Hand-Knapped Fixed Blade Specs
Maker: Pat Antuzzi
Blade length: Not quite 5”
Blade material: Mexican gold obsidian volcanic glass from Jalisco, Mexico
Handle material: Portoro marble from Italy
Overall length: 9.5”
Maker’s price for a similar knife: N/A

Best Steel For Knives: How To Choose

Intended cutting use and blade style help determine the ideal alloy for you and your knives.

Knives Annual
This article is an excerpt from the KNIVES 2025 annual, available at GunDigestStore.com.

Three critical aspects of creating or choosing a quality blade are steel selection, heat treatment and geometry. This feature focuses on the first of these, and the first any aspiring knifemaker or enthusiast will be tasked with—choosing the right blade steel for you and your knives.

To the casual observer, the steel selection process wouldn’t seem like such a big deal, but as in-depth as this article is, it barely scratches the surface of the topic.

Not all steels are created equal. Each varies as much as knife style and is designed for a specific application. So, matching the correct steel to the specific blade, intended use, and maker or user can be critical in creating a quality tool. Choosing the best alloy for your purpose can mean the difference between achieving the highest performance by effortlessly allowing the steel to do what it does best and struggling to pound a square peg into a round hole by forcing it to do something it was never designed to accomplish.

From my observations after a lifetime of providing metallurgical consulting services for various industrial clients and countless knifemakers, the latter rarely select steel with the same analytical vigor as the former. Rather than independent research to match steel chemistry to a process and product, knifemakers often choose whatever alloy everybody else is using.

American Bladesmith Society Journeyman Smith John Schultz chose well with 1075 steel for its natural toughness on his recurved chopper.

Be it a ubiquitous old favorite or the newest rage in the “steel of the month club,” no single alloy is the best fit for every knife, use or maker. On the other hand, the one area where knifemakers often exceed my industrial clients is letting frugality make the choice. The number of knifemakers who have told me they use a specific type of steel because of their access to a cheap or free supply is unfortunate.

The trouble with these approaches is needlessly steepening the learning curve for many a new maker or knife user. I can’t count the number of times I have heard a frustrated knifemaker state that an alloy they have tried is a bad steel. But there is no such thing as bad steel. Industry wouldn’t bother wasting time, effort or money on steel that wasn’t optimum for its intended purpose. There are poor application choices and bad heat treatments. Any fault lies with the knifemakers or bladesmiths and not the steel.

A36 is an excellent steel choice for use in buildings and bridges, but it is a bad reflection on knifemakers if they insist on making a blade with it. The steel properties of A36 are not conducive to knife blades. Alloys like 1095 or O-1 can make good hunting knife blades, but if the steels are heat treated like 5160, they won’t measure up in edge performance. I can’t tell you how often I’ve bitten my tongue when shown a blade fashioned from steel with barely enough carbon for adequate strength or an abrasion-resistant edge.

If knifemakers have to deviate from standard heat treatment practices with unorthodox extra steps, it is most likely the result of a steel choice that does not match their application or methods. You can under-soak or over-temper a 1% carbon steel sword or use an alloy better suited for such a blade. You can add several steps to heat-treating richly alloyed steel in your forge or choose a steel that readily responds to that heat source.

Intended Knife Use

Rather than using hard and soft layers for damascus, the author, Kevin Cashen, has always combined toughness with abrasion resistance, as in this O1/L6 skinner.

The problem is that we often proceed from the wrong direction. Whatever the reason, many knifemakers have already settled on their steel before determining what knife they will fashion, but how can you make the right choice in a material before you even know its intended use?

A better model for success is letting the primary tasks a knife is meant to perform determine needs and goals. Develop a plan to achieve those goals by designing a hand tool that will perform a specific task or even multiple tasks, keeping in mind that the intended uses of a single knife can be much more varied than people think. With the desired tasks for the edged tool in mind, choose the material based on the desired properties inherent to each steel’s specific chemistry. Equally important is recognizing the limits of a maker’s abilities to work with a given chemistry.

To explain how to choose the correct steel for you and your knives, the myriad of blade designs is distilled down to two primary categories. The first group—fine-cutting knives—is designed to perform keen slicing or aggressive slashing. They are most often used in a draw-type cut that is optimized like a saw at the microscopic level. Think of scalpels, skinning and hunting knives, and many kitchen knives. Their edges are thin, flat or hollow ground for cutting various soft, fibrous materials.

This group has a subcategory of blades, including some kitchen knives and razors, that will be identical in many design features and desired properties, but they are used more in a push cut. Regardless, impact toughness is not nearly as crucial as abrasion resistance for knives like this.

The effects of carbon content in a simple steel can be seen on the Iron-Carbon phase diagram.

In contrast, the second group—choppers—is used in straight-on, push-type motions, cleaving, or cutting that often involves impact. These knives cut more like a chisel than a blade drawn into a cut like a saw. Camp knives, some bowies, and many swords fall into this category. They benefit from polished, beefier, convex edge grinds that don’t require abrasion resistance as much as impact toughness.

By definition, a knife is a cutting tool. If we should ever find ourselves detracting from a blade’s ability to cut in any part of our plan or execution thereof, we may need to consider whether making a knife or another tool is the better option.

Thus, all the properties discussed herein are relevant to cutting. A fundamental condition for a blade to slice through material is that it must be stronger than the cutting medium. There is tremendous load pressure at the microscopic level, where the cut is initiated. So, almost by definition, strength must be a top priority in any knife edge.

For this article, strength is the ability to resist deformation under load. Opposing this prized quality of strength is ductility, or the ability to easily deform without edge or blade failure. Knifemakers heat treat steel to replace ductility with strength. For millennia, it was the job of the blade maker to find the most acceptable compromise between strength and ductility for their blades to cut while avoiding brittle failure.

Steel Strength

The graph shows the total hardness from proper solution in steels soaked for 1 minute and 10 minutes, respectively, illustrating the effects alloying can have on heating requirements.

There are many types of strength in steel. Examples are compressive strength and tensile strength. These and shear strength are not as apparent in general knife use, so knifemakers more easily conceptualize them as hardness.

The other quality prized in a blade is toughness, which should be viewed as the steel’s ability to withstand shock from sudden loads rather than bending in a ductile manner under gradual load. These are two entirely different behaviors, with one being more relevant to a blade used in chopping. Rather than the Faustian bargain of trading strength for ductility, the Holy Grail of blade making is maintaining high strength with impact toughness. In chopping-type blades, impact toughness is almost as valuable as strength.

The next property to consider in a knife blade is abrasion resistance. Microscopically, the knife edge is subjected to tremendous wear, even when cutting seemingly soft materials. It is this wear that results in the tool dulling when used. Abrasion resistance is the steel’s ability to withstand such friction effects. While this property does increase with overall hardness, steel’s unique makeup gives it abrasion resistance above and beyond hardness and even independently from it. Within the steel, there might also be carbide particles with a hardness that far exceeds the overall Rockwell measurement numbers of the blade. Fine cutting and slicing blades benefit more from abrasion resistance than impact toughness.

Although the possible steel choices for modern knifemakers are endless, for simplicity’s sake, this discussion is limited to non-stainless alloys commonly used by forgers and grinders alike. Although many knifemakers have become dependent on AISI (American Iron and Steel Institute) or SAE (Society of Automotive Engineers) steel names, such titles as 1084, W-2 or 80CrV2 lack specificity and meaning compared to studying the individual steel’s chemistry in determining its potential properties.

The more alloying helps us in gentler quenches, the more attention must be paid to proper heating, making some steels a better match for a forge and others a digital oven.

I strongly encourage knifemakers to study the chemistry of any potential steel choices to decide which one to use and how to work it. A supplier that provides the chemistry for your steel understands this and is well worth doing business with rather than a source that omits the alloy’s makeup.

Carbon content is the first consideration within a steel’s chemistry and perhaps the most important. Carbon is the main element responsible for strength in steel. The more carbon a steel has, the greater strength can be achieved in hardening. However, this is only true to a certain point; maximum hardness in carbon steel is achieved at around .80% carbon, and beyond this, not much more is gained in that area. Putting more carbon than .80% into the solution during the hardening process can harm a bladesmith’s goals. However, carbon beyond this optimum level will add abrasion resistance if allowed to stay in carbide form.

This sweet spot in carbon levels around .80% is known as the eutectoid. It is the most efficient use of carbon in steel, with no leftover iron (ferrite) or any leftover carbide (cementite). Steels with less than .80% carbon content are inherently tougher and less brittle, while steels with more can have much greater abrasion resistance with a tendency to be less tough. This is important to consider when choosing steel for your intended blade purpose. Does a machete need abrasion resistance? Does a skinning knife need to be tough? Choosing 1075 for one or 1095 for the other could make all the difference in having a steel that will work for you or against you in creating that blade.

In centuries past, bladesmiths had no choice but to compromise between strength and ductility when working with simple iron-carbon material. But then, starting in the early 19th century, alloying changed everything. Finally, with the intentional addition of other elements to steel, bladesmiths could have their cake and eat it, too.

Steel Alloys

Combining it in one chart helps select the correct steel based on knife use and a knifemaker’s heat-treating equipment.

A sword in the 13th century that had to be kept in the low hardness ranges could now be just as tough at much higher hardness levels. Fine slicing cutters could have an abrasion-resistant carbide boost far exceeding simple cementite abilities. But with these gains in performance came greater demands for more precise controls in heat treating, atmosphere, and more refined blade quenches. Today, even the most basic carbon steels have enough alloys to radically differentiate them from the old steel. Anybody who thought they would water quench 1084, just like traditional tamahagane steel, can attest to this fact.

For this reason, another critical factor must be considered in proper steel selection beyond the type of knife being made. It is why the premise of this article is choosing the right steel for you and your knife. Our modern steel alchemists may have created the perfect high-tech steel for a knifemaker’s application. But if they’re learning the ropes, or all they own is a humble forge, it could still be a terrible choice for their knife.

If your shop is equipped with a digitally controlled oven, all the many modern alloy options are available if you learn the rules each steel choice requires. The same chemistry that makes one steel harden in almost any oil or air makes it much more finicky when heated before being quenched. An alloy steel may have the potential to outperform a simple carbon steel, but not if you lack the equipment necessary to unlock that potential.

Figure 1 shows the as-quenched hardness results of a series of tests involving simple heating versus a standard 10-minute soak on commonly used steels. Here, the effect of increased alloying is plain to see when looking at each steel’s time and temperature requirements, which many open-flame heat sources or forges may struggle to meet. Unless armed with an excellent understanding of the metallurgy, a smith desiring to stick with more traditional tools would be better served by more traditional steels. Simple carbon steels such as “W” or 10XX series are like what forges were initially made for and will allow the traditional smith to produce a fine blade effortlessly.

Knowing what each of the additional alloying elements brings to the table is valuable in knowing what to seek in steel. If you’re looking for impact toughness, consider chemistries that include nickel or silicon. These additions affect the iron’s atomic lattice, which acts like a shock absorber. For a knife needing abrasion resistance, a boost from the more powerful carbide formers can give you longer wear than simple cementite, with two of the most common examples being vanadium (above .25% of overall elements) or tungsten. Chromium will also help in this area to a lesser extent.

If you wish to achieve a fully hardened blade with minimal effort, manganese over 1% or relatively modest additions of chromium are just the ticket for leaving behind your stressful days of the water quench. And, of course, for applications where simple carbon steels would rust too quickly, chromium over 11% will also help resist corrosion.
The chart in Figure 2 brings together all these considerations. On a final note, it must be conceded that a skilled bladesmith with a solid knowledge of heat treatment could push several of these alloys into adjacent categories. Still, here, we’ve focused on the path of least resistance.

By capitalizing on the characteristics of an alloy’s chemistry, a maker can spend less time getting it to behave in the desired manner and more time maximizing its performance.

More On Knife Steel:

Dietmar Pohl Celebrates 30 Years In The Knife Industry

0

From passion to icon: celebrating 30 years of Dietmar Pohl’s knife mastery.

Dietmar Pohl is a name well-known in knife circles. More so than his groundbreaking designs, the founder of Pohl Force knives might also be known for his professionalism. On Nov. 18, the designer celebrated 30 years in the industry. 

With over 100 knife designs, three books translated into multiple languages, and a reputation for innovation, Pohl has established himself as a leading figure in the world of blades.  

While Pohl might be best known for his knives, such as the Magnum Colection Knife and the Böker Speedlock switchblade, he has held many roles in the industry.  

Dietmar Pohl talking with military man

Pohl started his career as marketing director, design and production manager in Solingen, Germany.  Combining contemporary design with cutting-edge materials, he quickly made his mark by creating knives that balanced performance and aesthetics.  

However, his interest in edged tools started well before then. His imagination was captured at 11 years old when his older brother—10 years his senior—returned from the Bundeswehr paratroopers and showed him his paratrooper knife. 

While Pohl has no military or law enforcement background, he’s built his expertise through hands-on training and close collaboration with professionals in elite units like Germany’s GSG9, SEK, and U.S. Marine Force Recon.  

Practical experiences, such as SWAT training in Virginia and knife combat sessions with Marine Force Recon at Camp Pendleton, have deepened his understanding of tactical requirements.  

Dietmar Pohl with sylvester stallone

Pohl’s influence extends beyond design. His books are respected resources for enthusiasts, and his work is frequently featured in trade publications. Among his standout achievements is the MK9 Heartstopper, created for Sylvester Stallone’s final Rambo movie, Last Blood. Dubbed The Knife Guy by the film crew, this project solidified his global reputation.  

Read Knife Reviews:

Advertisement

Must Read Articles

Read this before you make a knife

Knifemaking 101 – Read This Before You Make a Knife

  by Wayne Goddard My experience has taught me that there's nothing like digging in and getting started. I've often said the hardest part of the...
how to forge damascus steel

How to Forge Damascus

Advertisement
Advertisement