Knifemaking

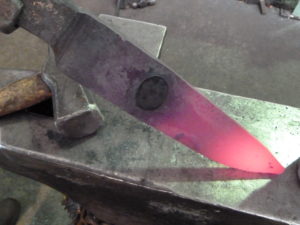
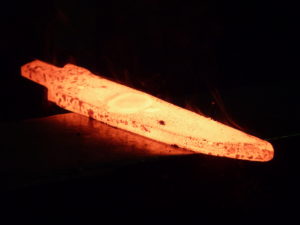
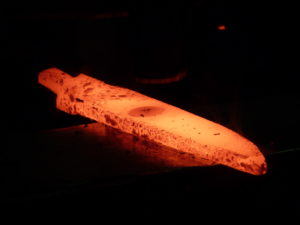
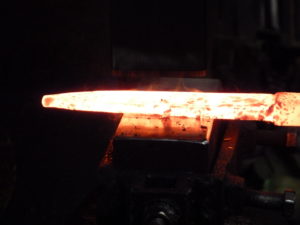
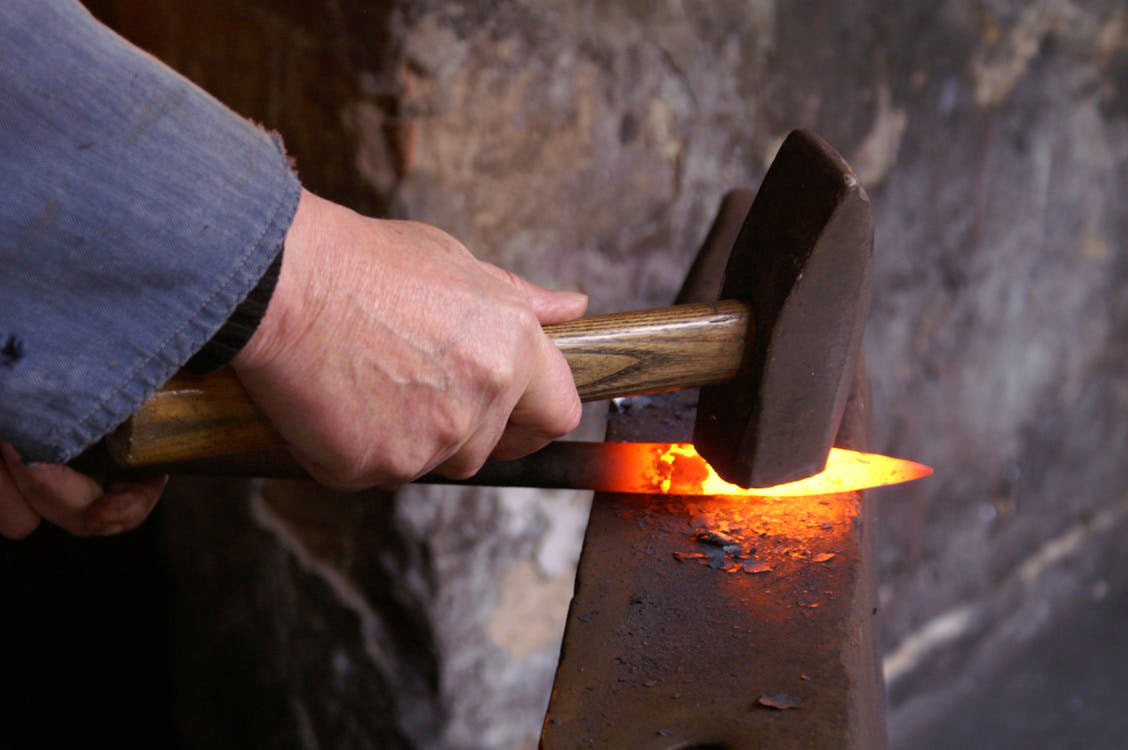
Knifemaking is the building of a knife, which includes the blade, handle and other accouterments. Blades are made by either removing metal from a steel blank via a grinder – known as stock removal – and the forging to shape of hot steel into a blade in the process known as bladesmithing. Other parts, including bolsters, guards, pommels, etc., are needed to complete the finished knife.

Featured Knives – – Knife Collecting – – Tactical Knives – – Survival Knives

DIY Engraving Vise or Block

0

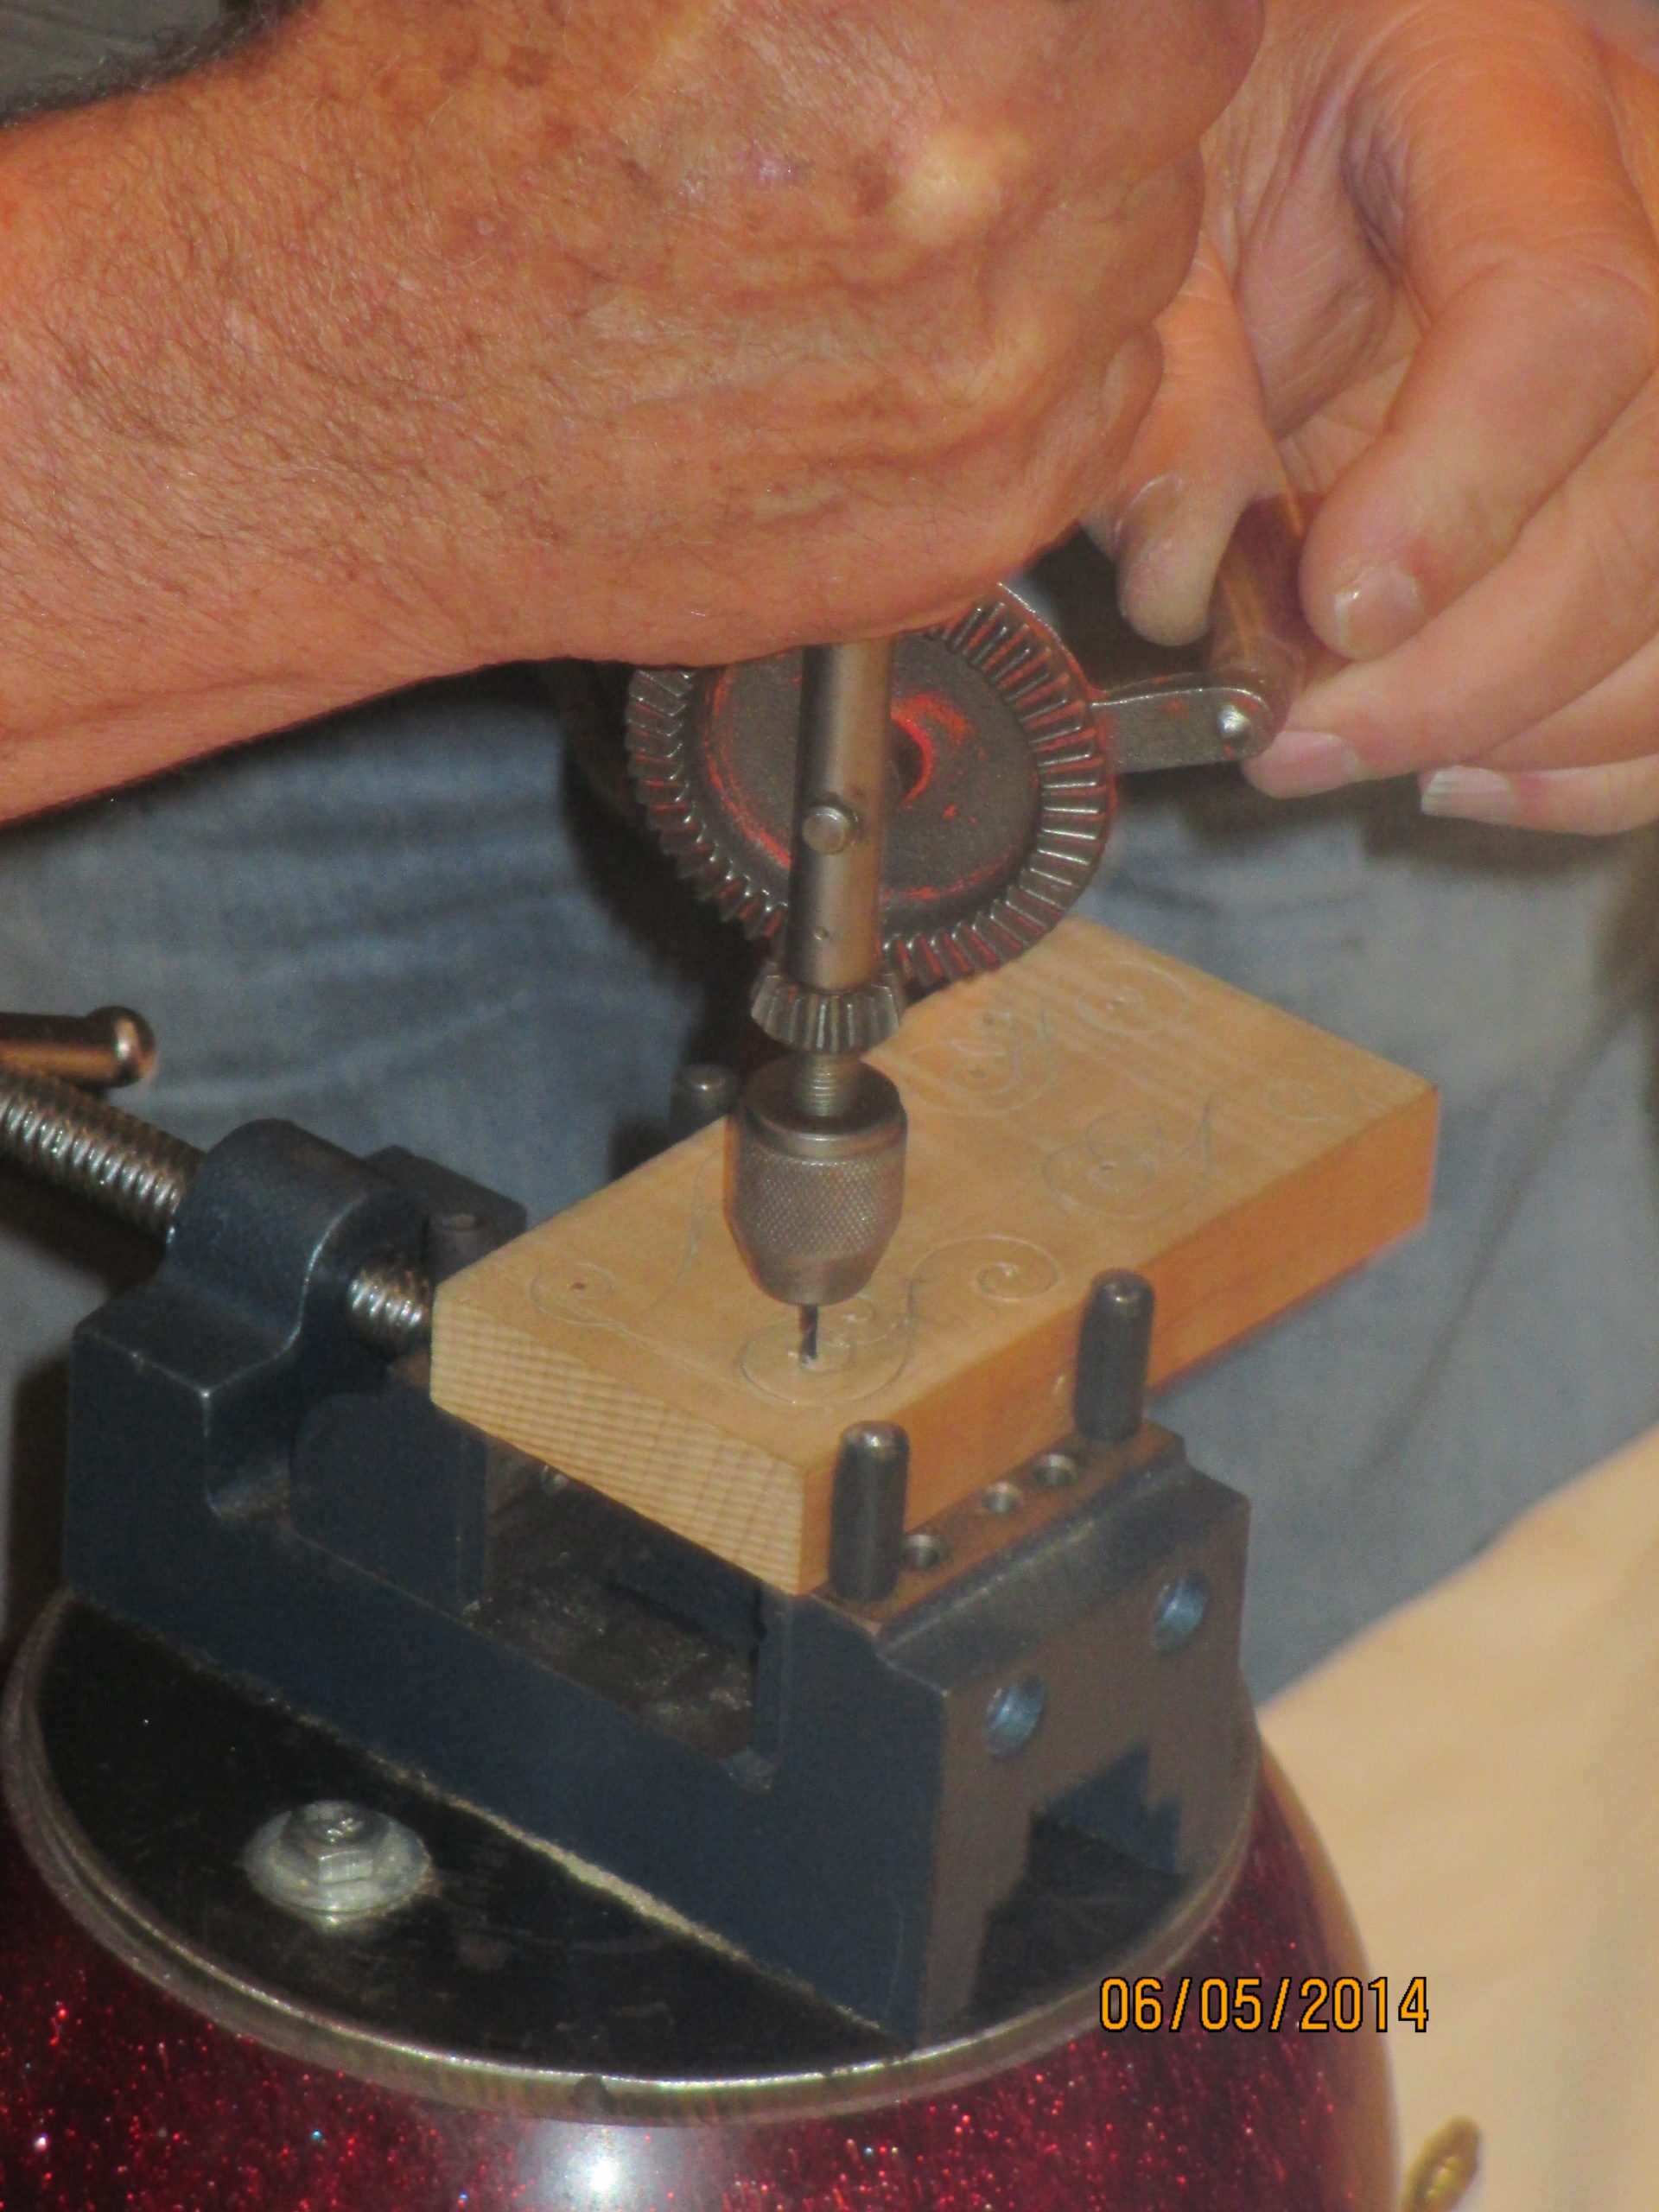
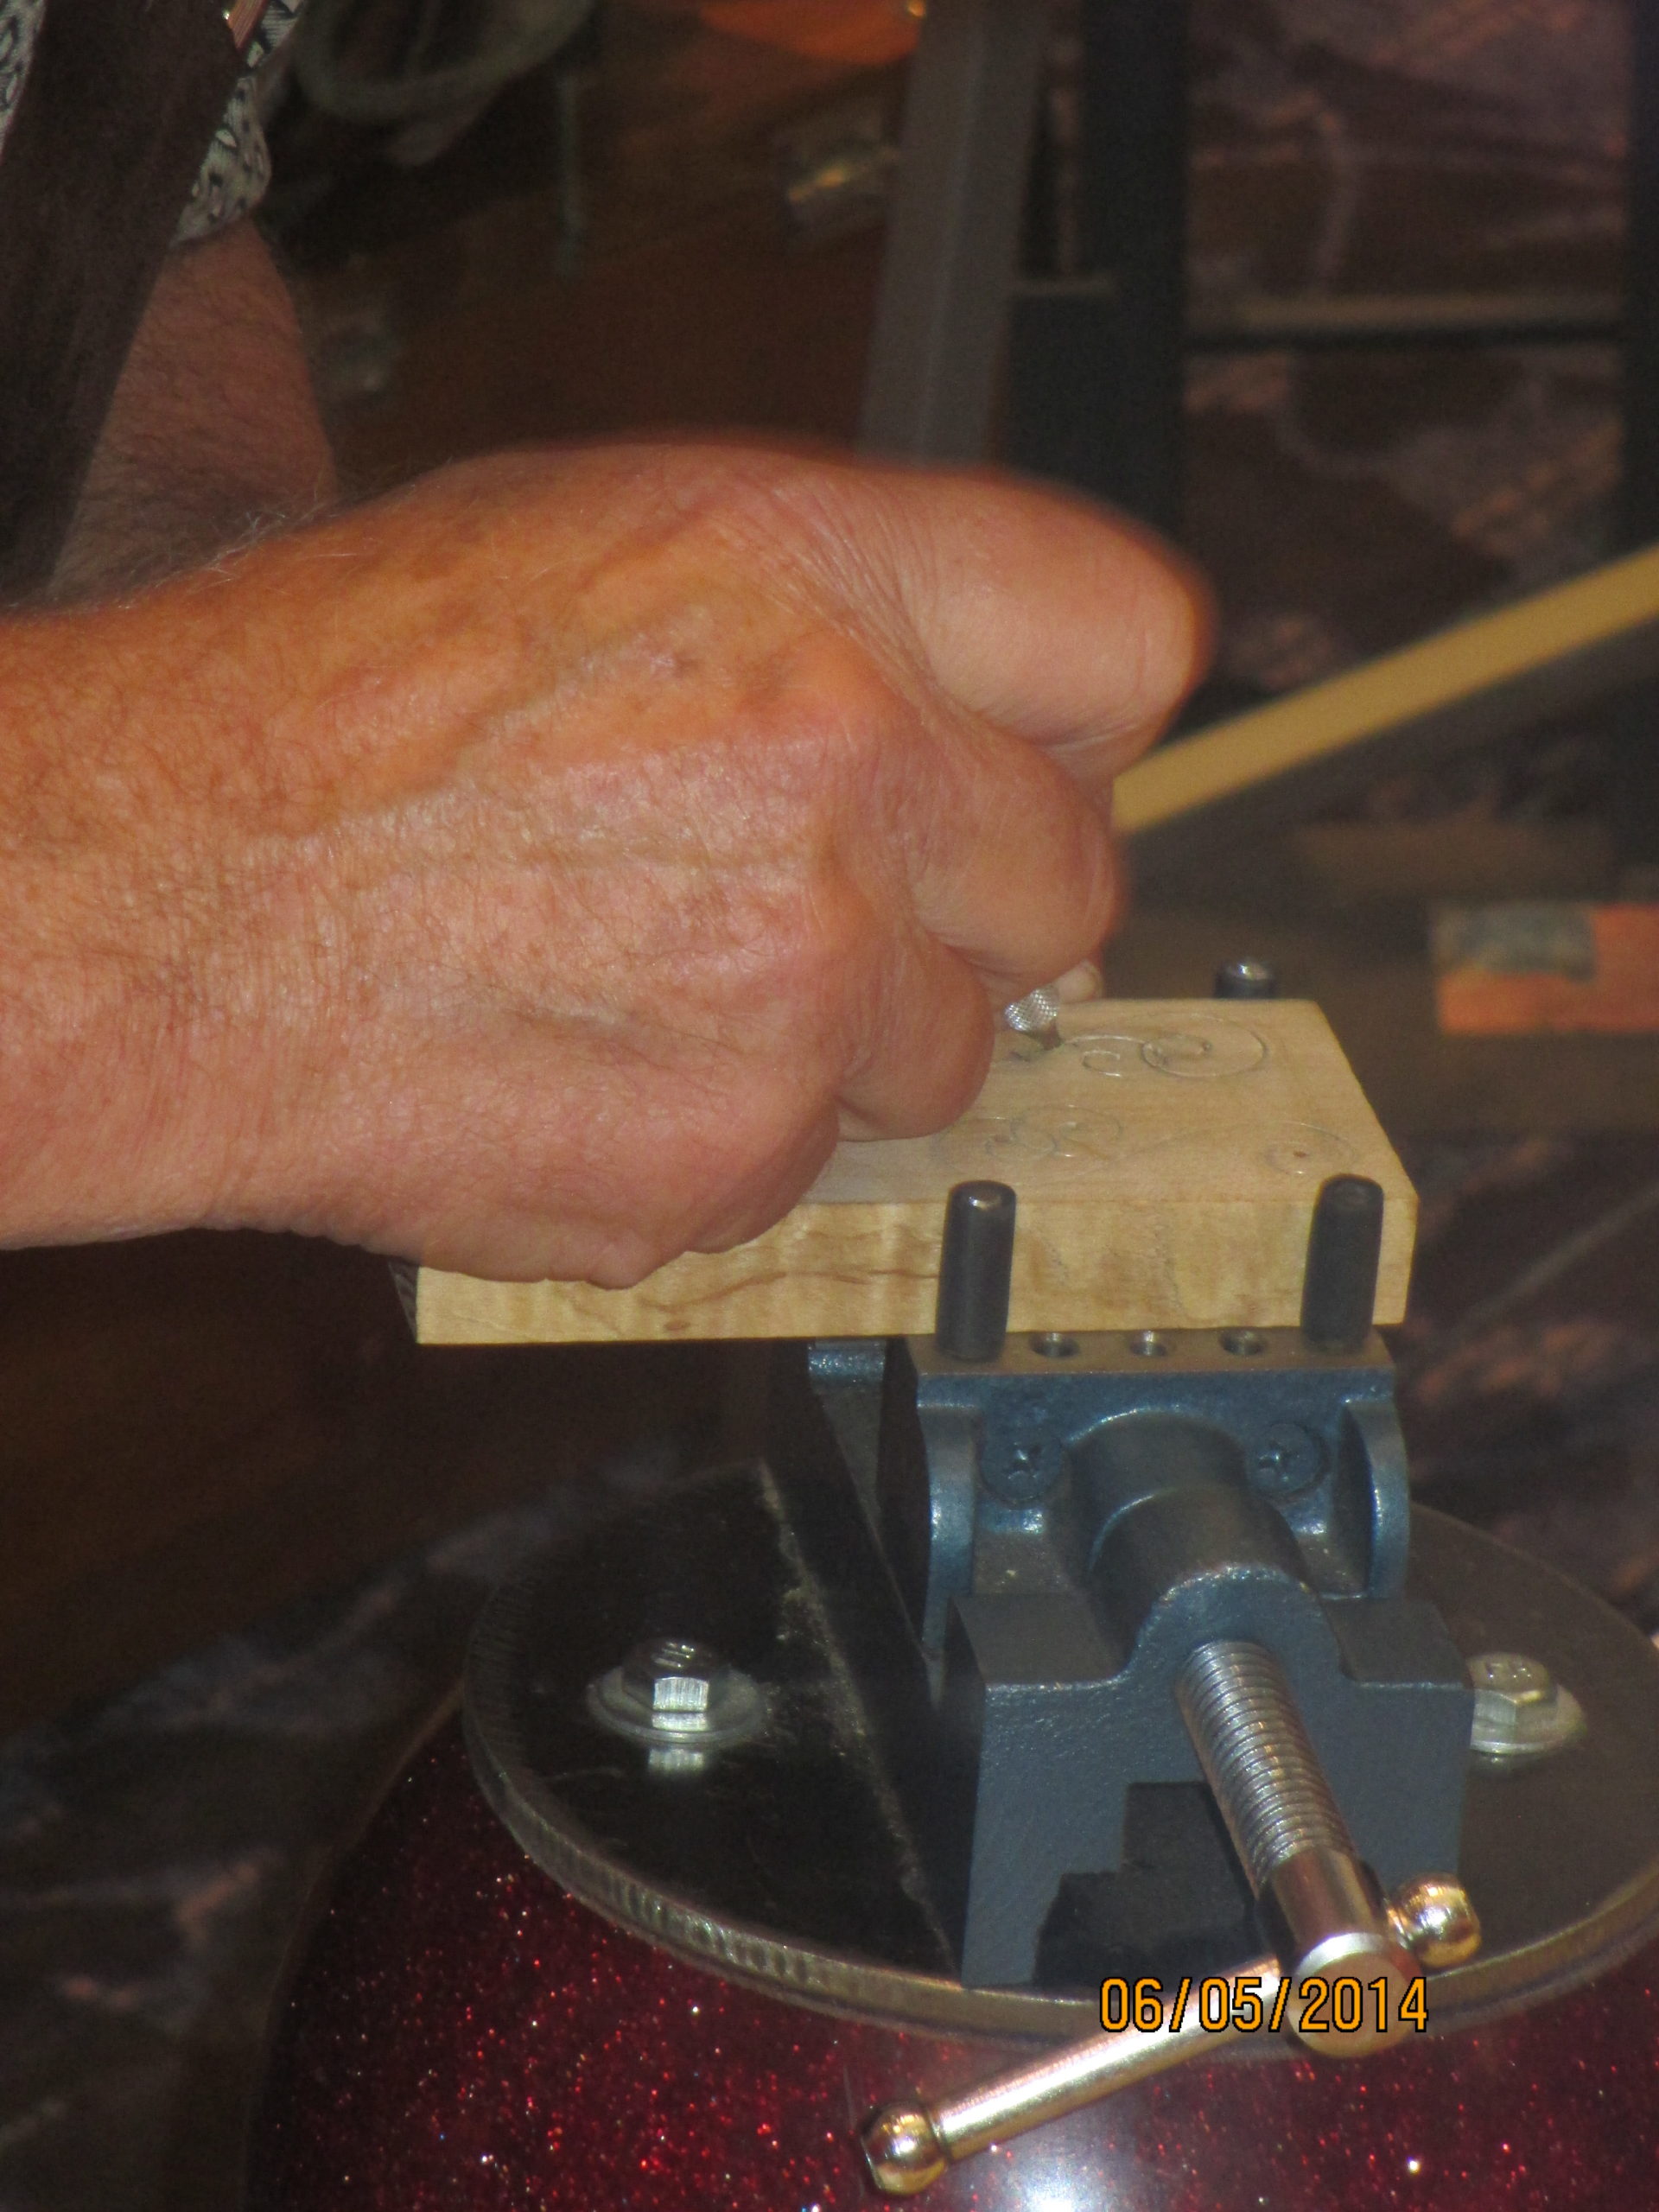
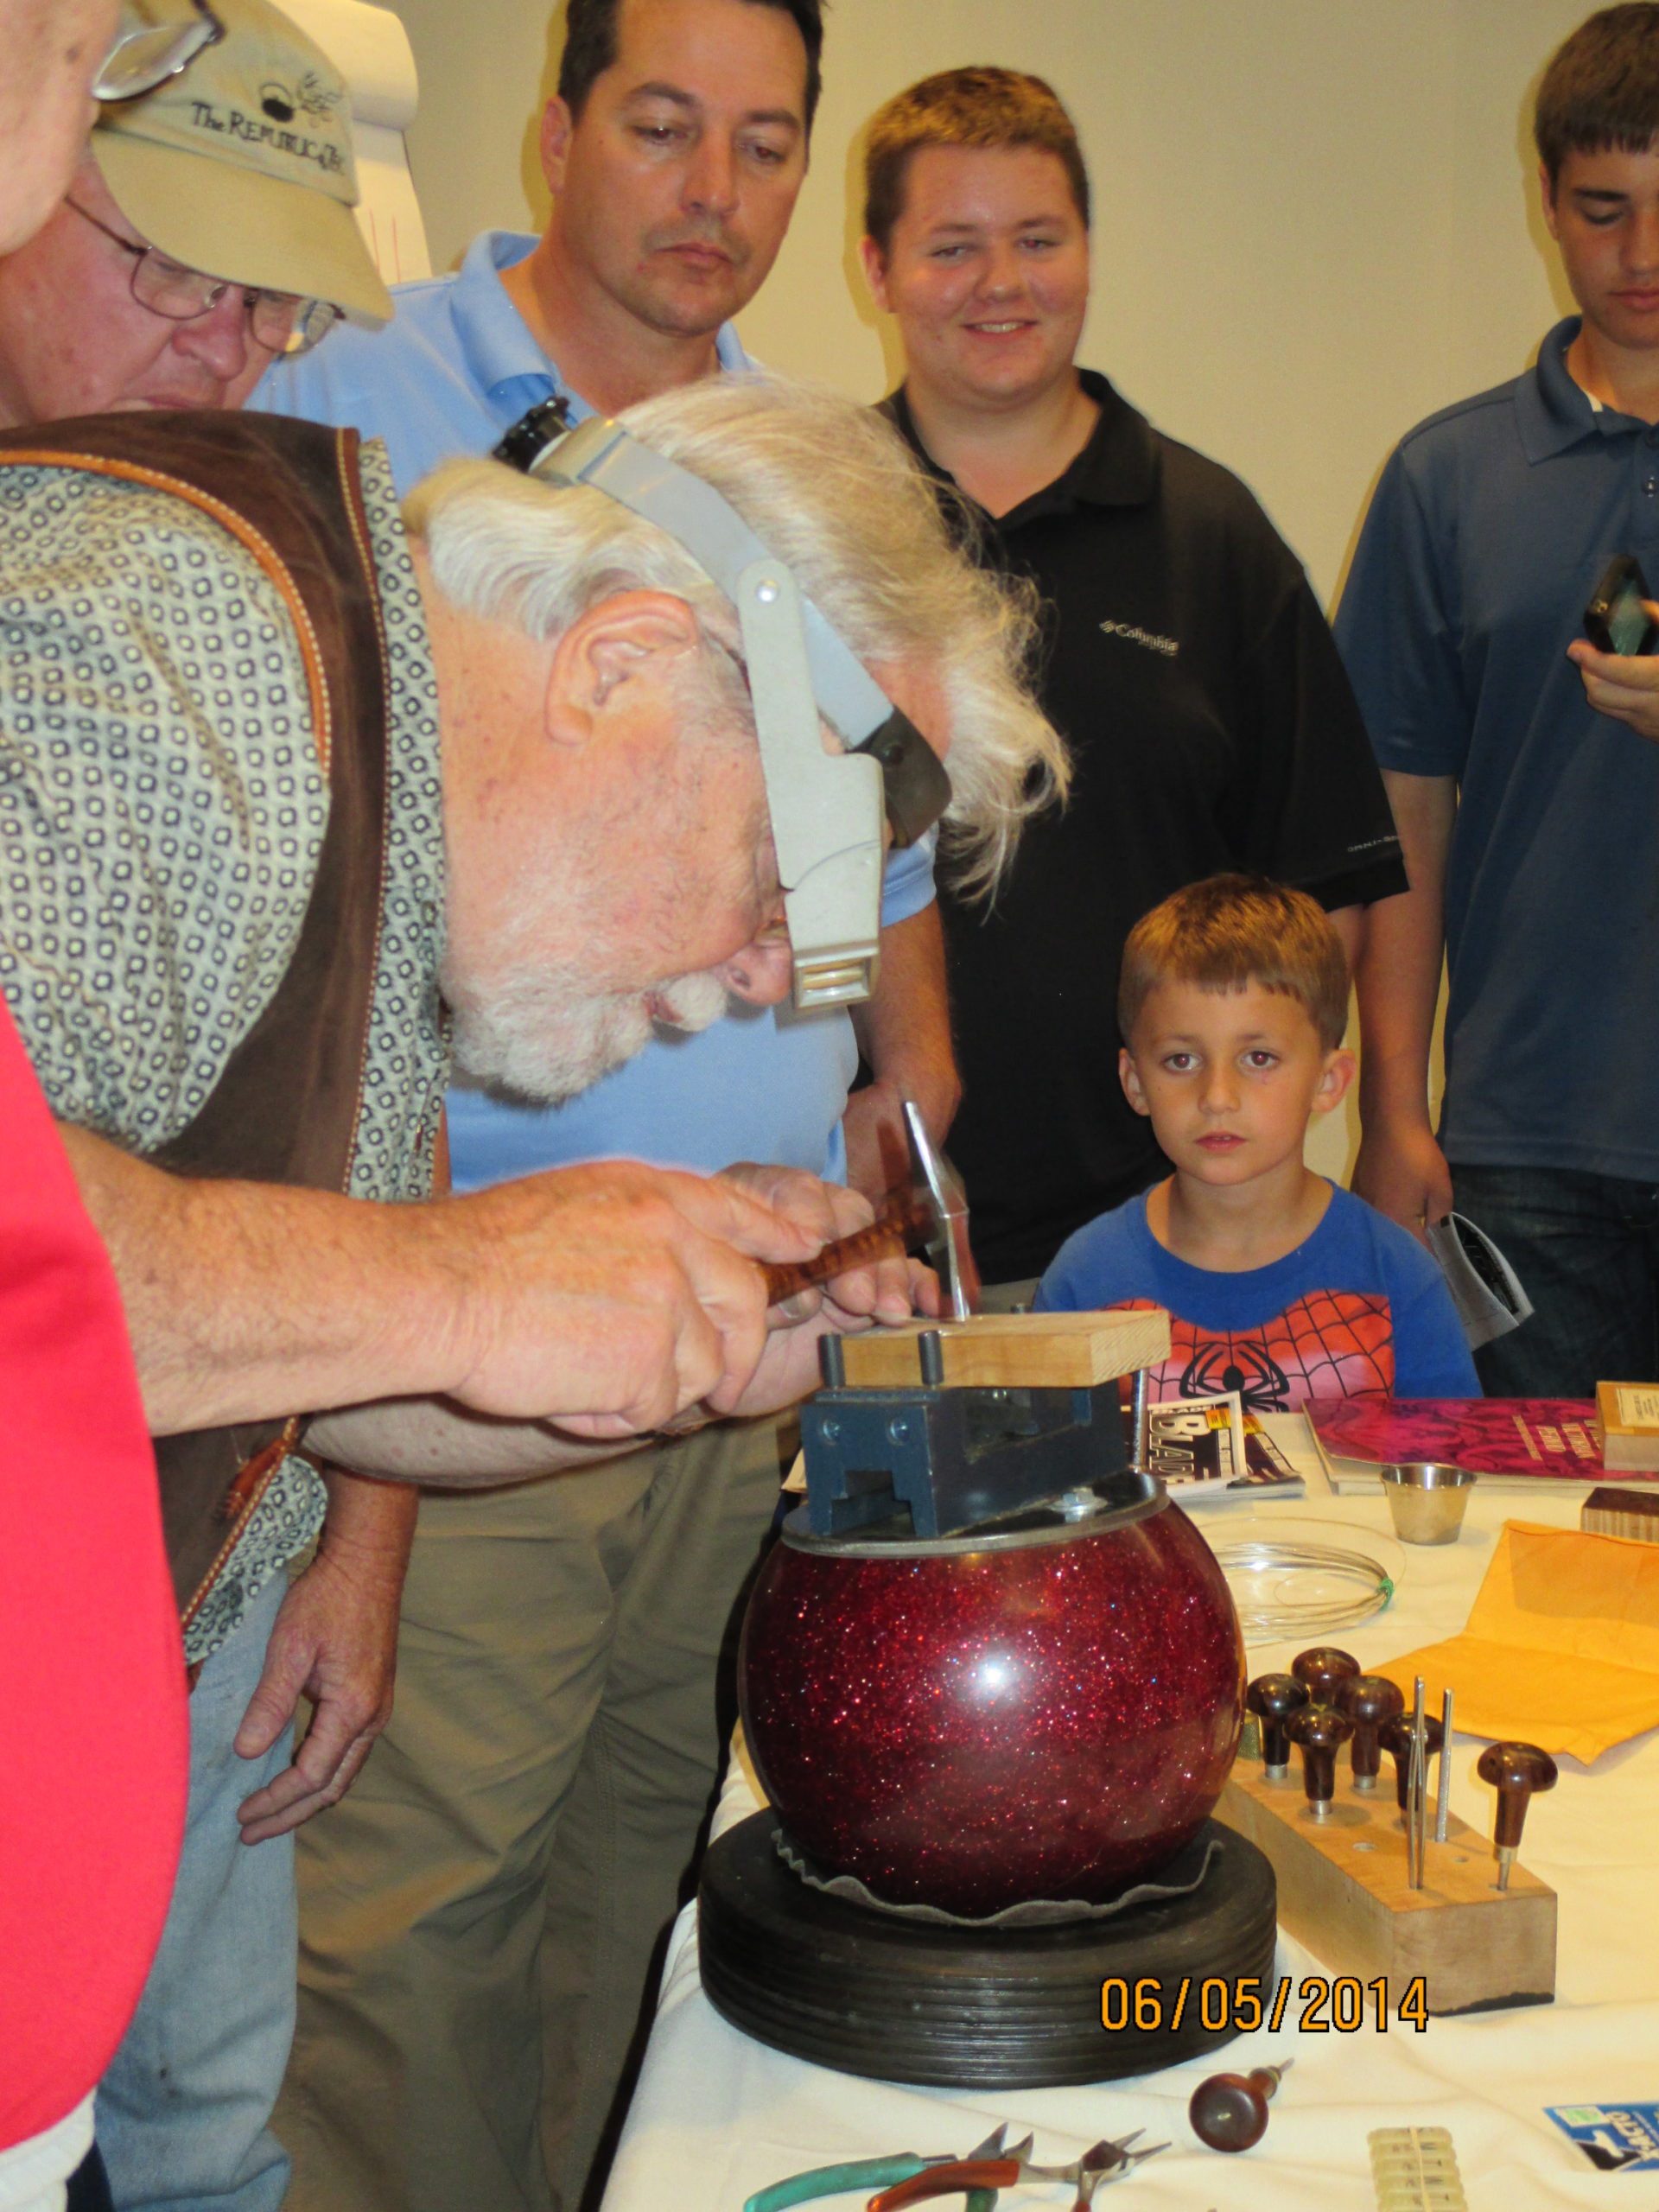
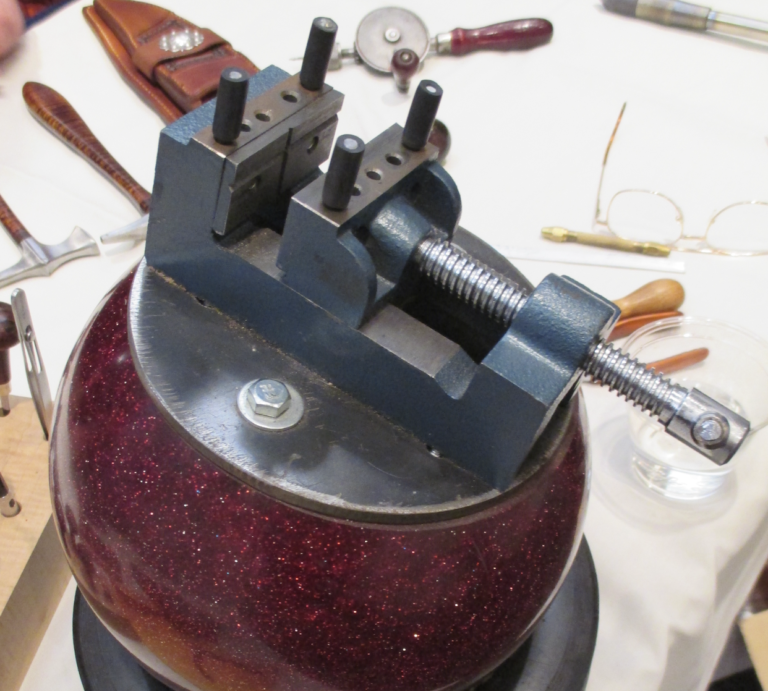
The bowling ball vise makes knife handle work easy and inexpensive

As the old adage goes, “necessity is the mother of invention,” but whoever thought of making an engraving vise out of a bowling ball deserves a medal!

The engraver’s vise, which has a rotating base so the craftsman can position his work at any angle, has been around for many years. Small versions are affordable but one big enough to accept a large knife handle can cost in the $600-to-$700 range.

Enter the bowling ball vise.

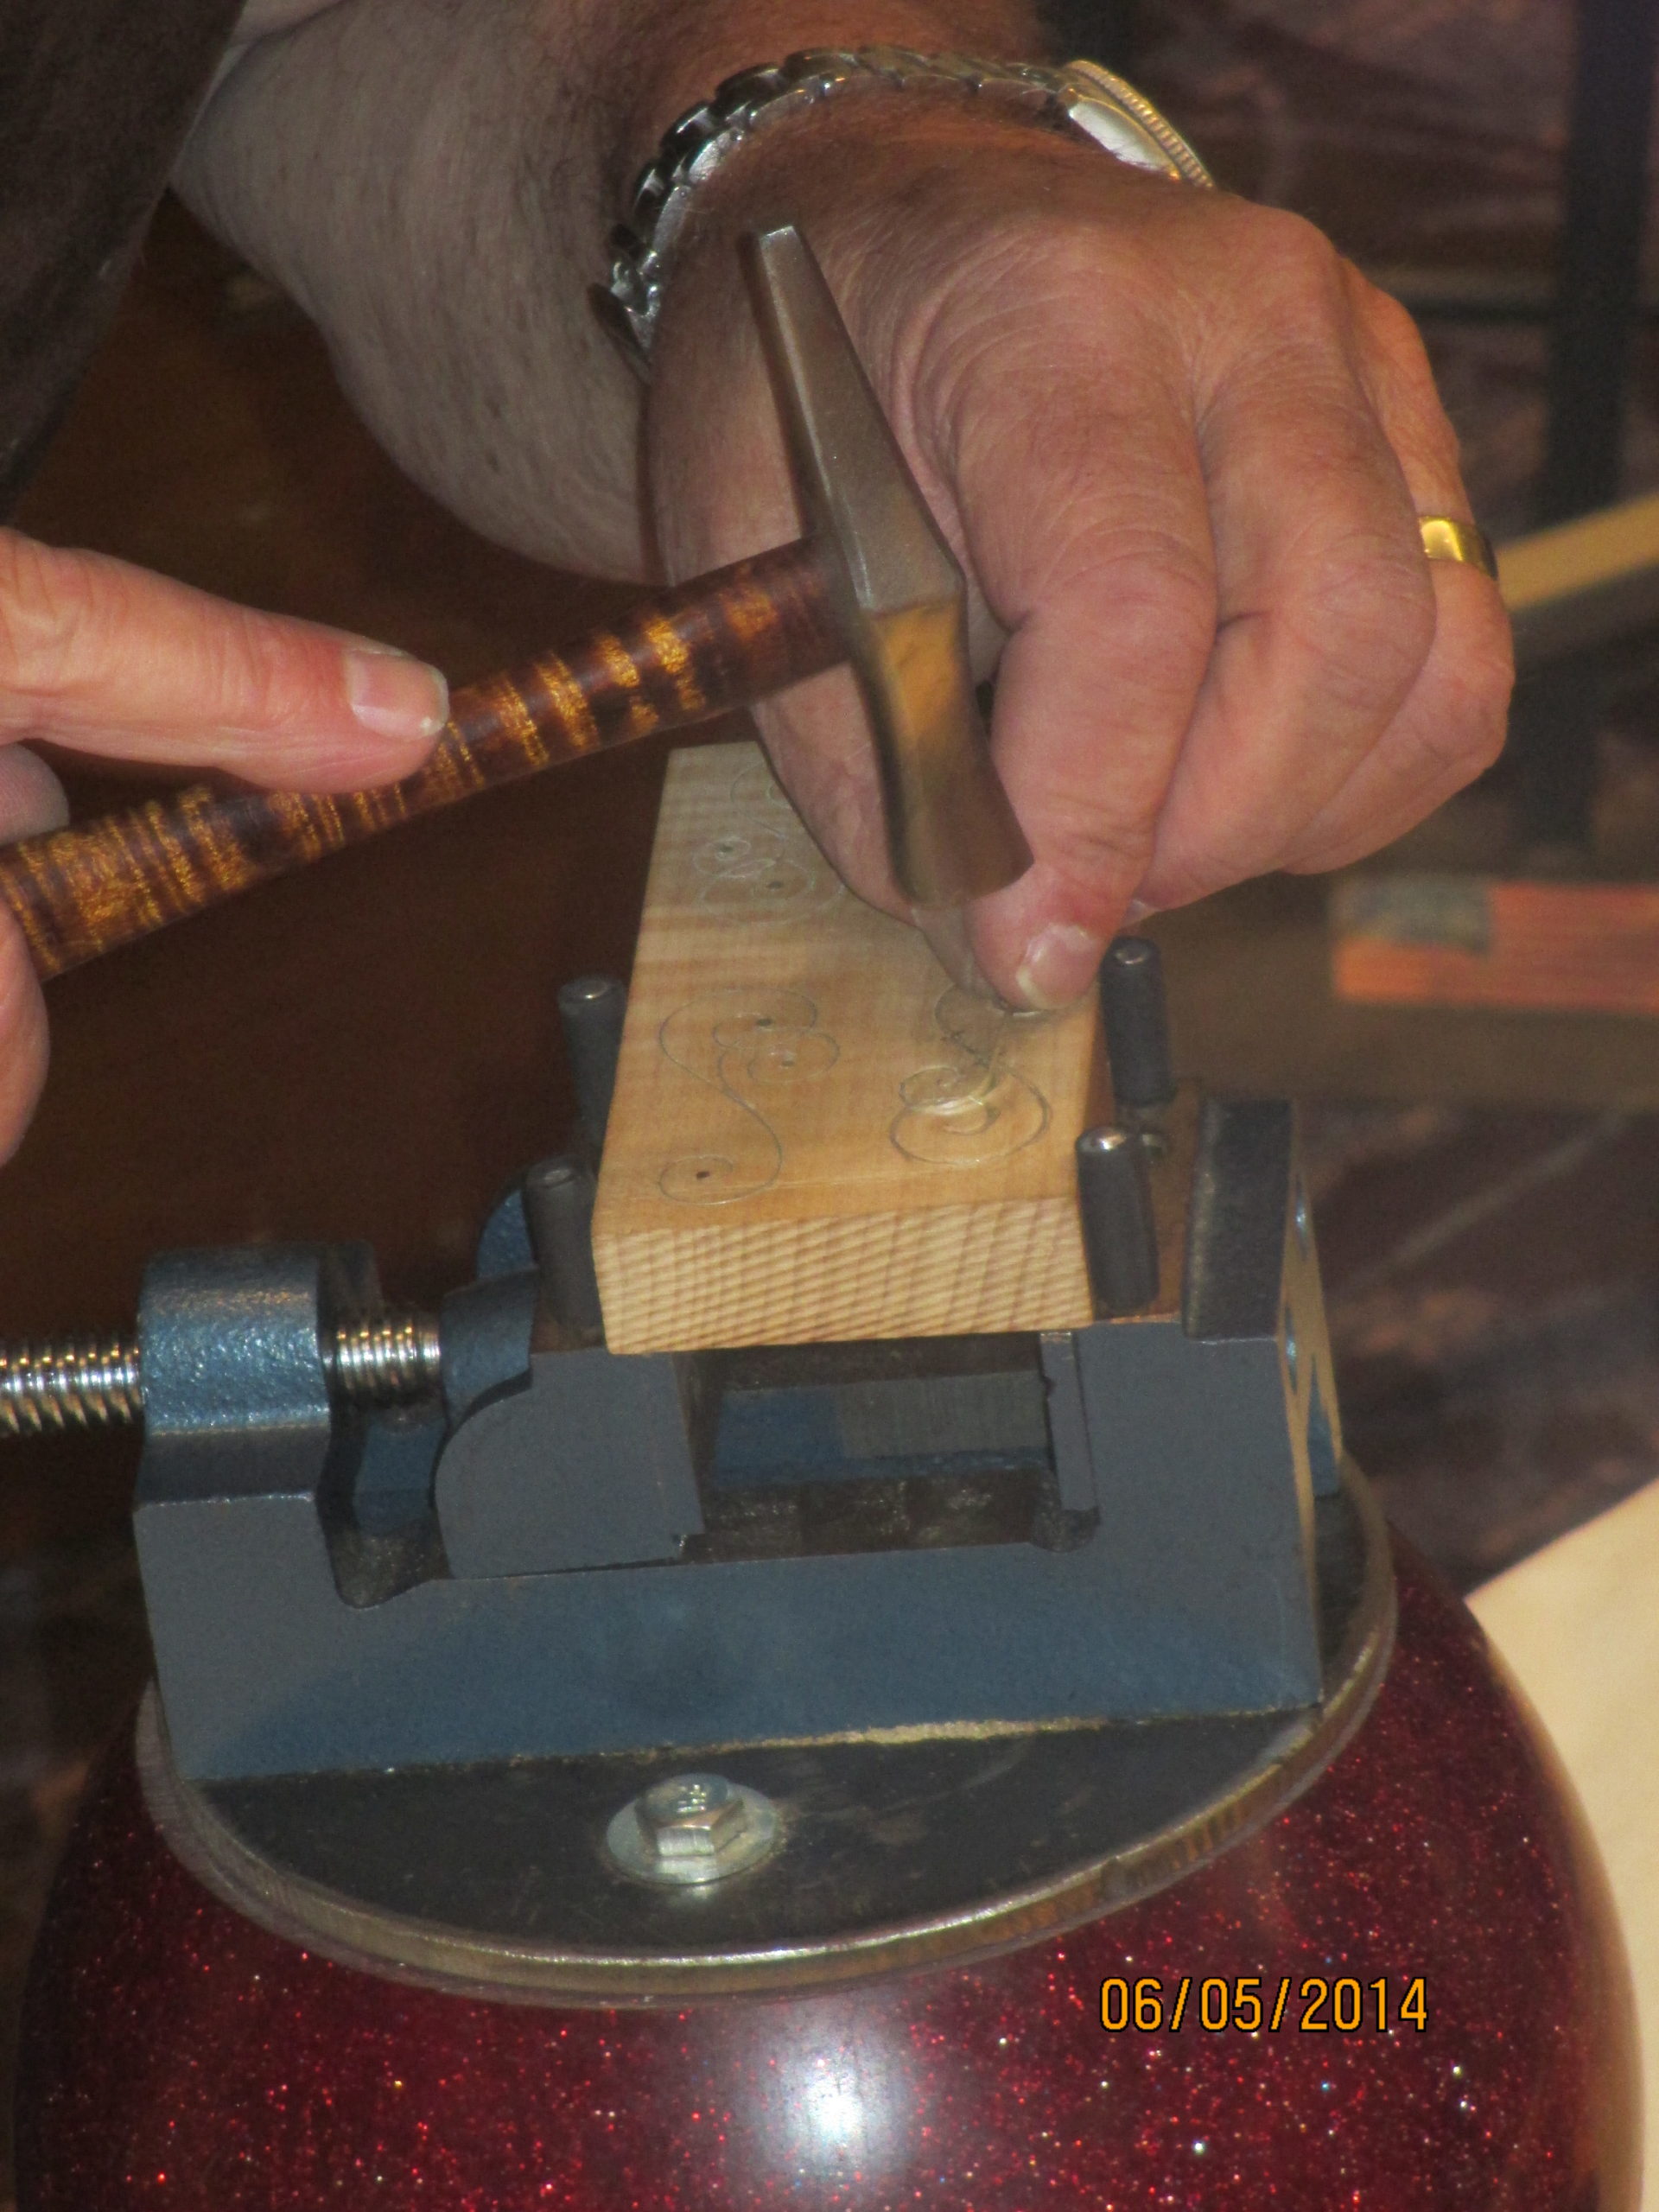
American Bladesmith Society Master Smith Don Hethcoat has made several bowling ball vises, including one for fellow ABS master smith Joe Keeslar. Both makers find the vise particularly useful for inlaying gold and silver wire into knife handles. “I learned about the vise in 1988,” Hethcoat recalls. “I wish I could take credit for creating it, but I first saw it being used by Firearm Engravers Guild member John Barraclough.”

“The first and only bowling ball vise that I ever had was a gift from Don Hethcoat many years ago,” Keeslar says. “In my Kentucky shop I use an engraving ball for my silver wire inlay work, but for my shop and demonstrations in France I use a bowling ball vise. I could not afford to buy a second engraver’s ball for my shop abroad.”

Used bowling balls are cheap, and beyond that the biggest expense to making a bowling ball vise is adding a machinist’s vise on top of the modified sphere. The cost for these items is a fraction of what an engraver’s vise costs, and the rest of the materials to complete the vise are very affordable. Indeed, they can be found around your shop, home or at your local scrap yard.

IMPROVISING WELCOME!

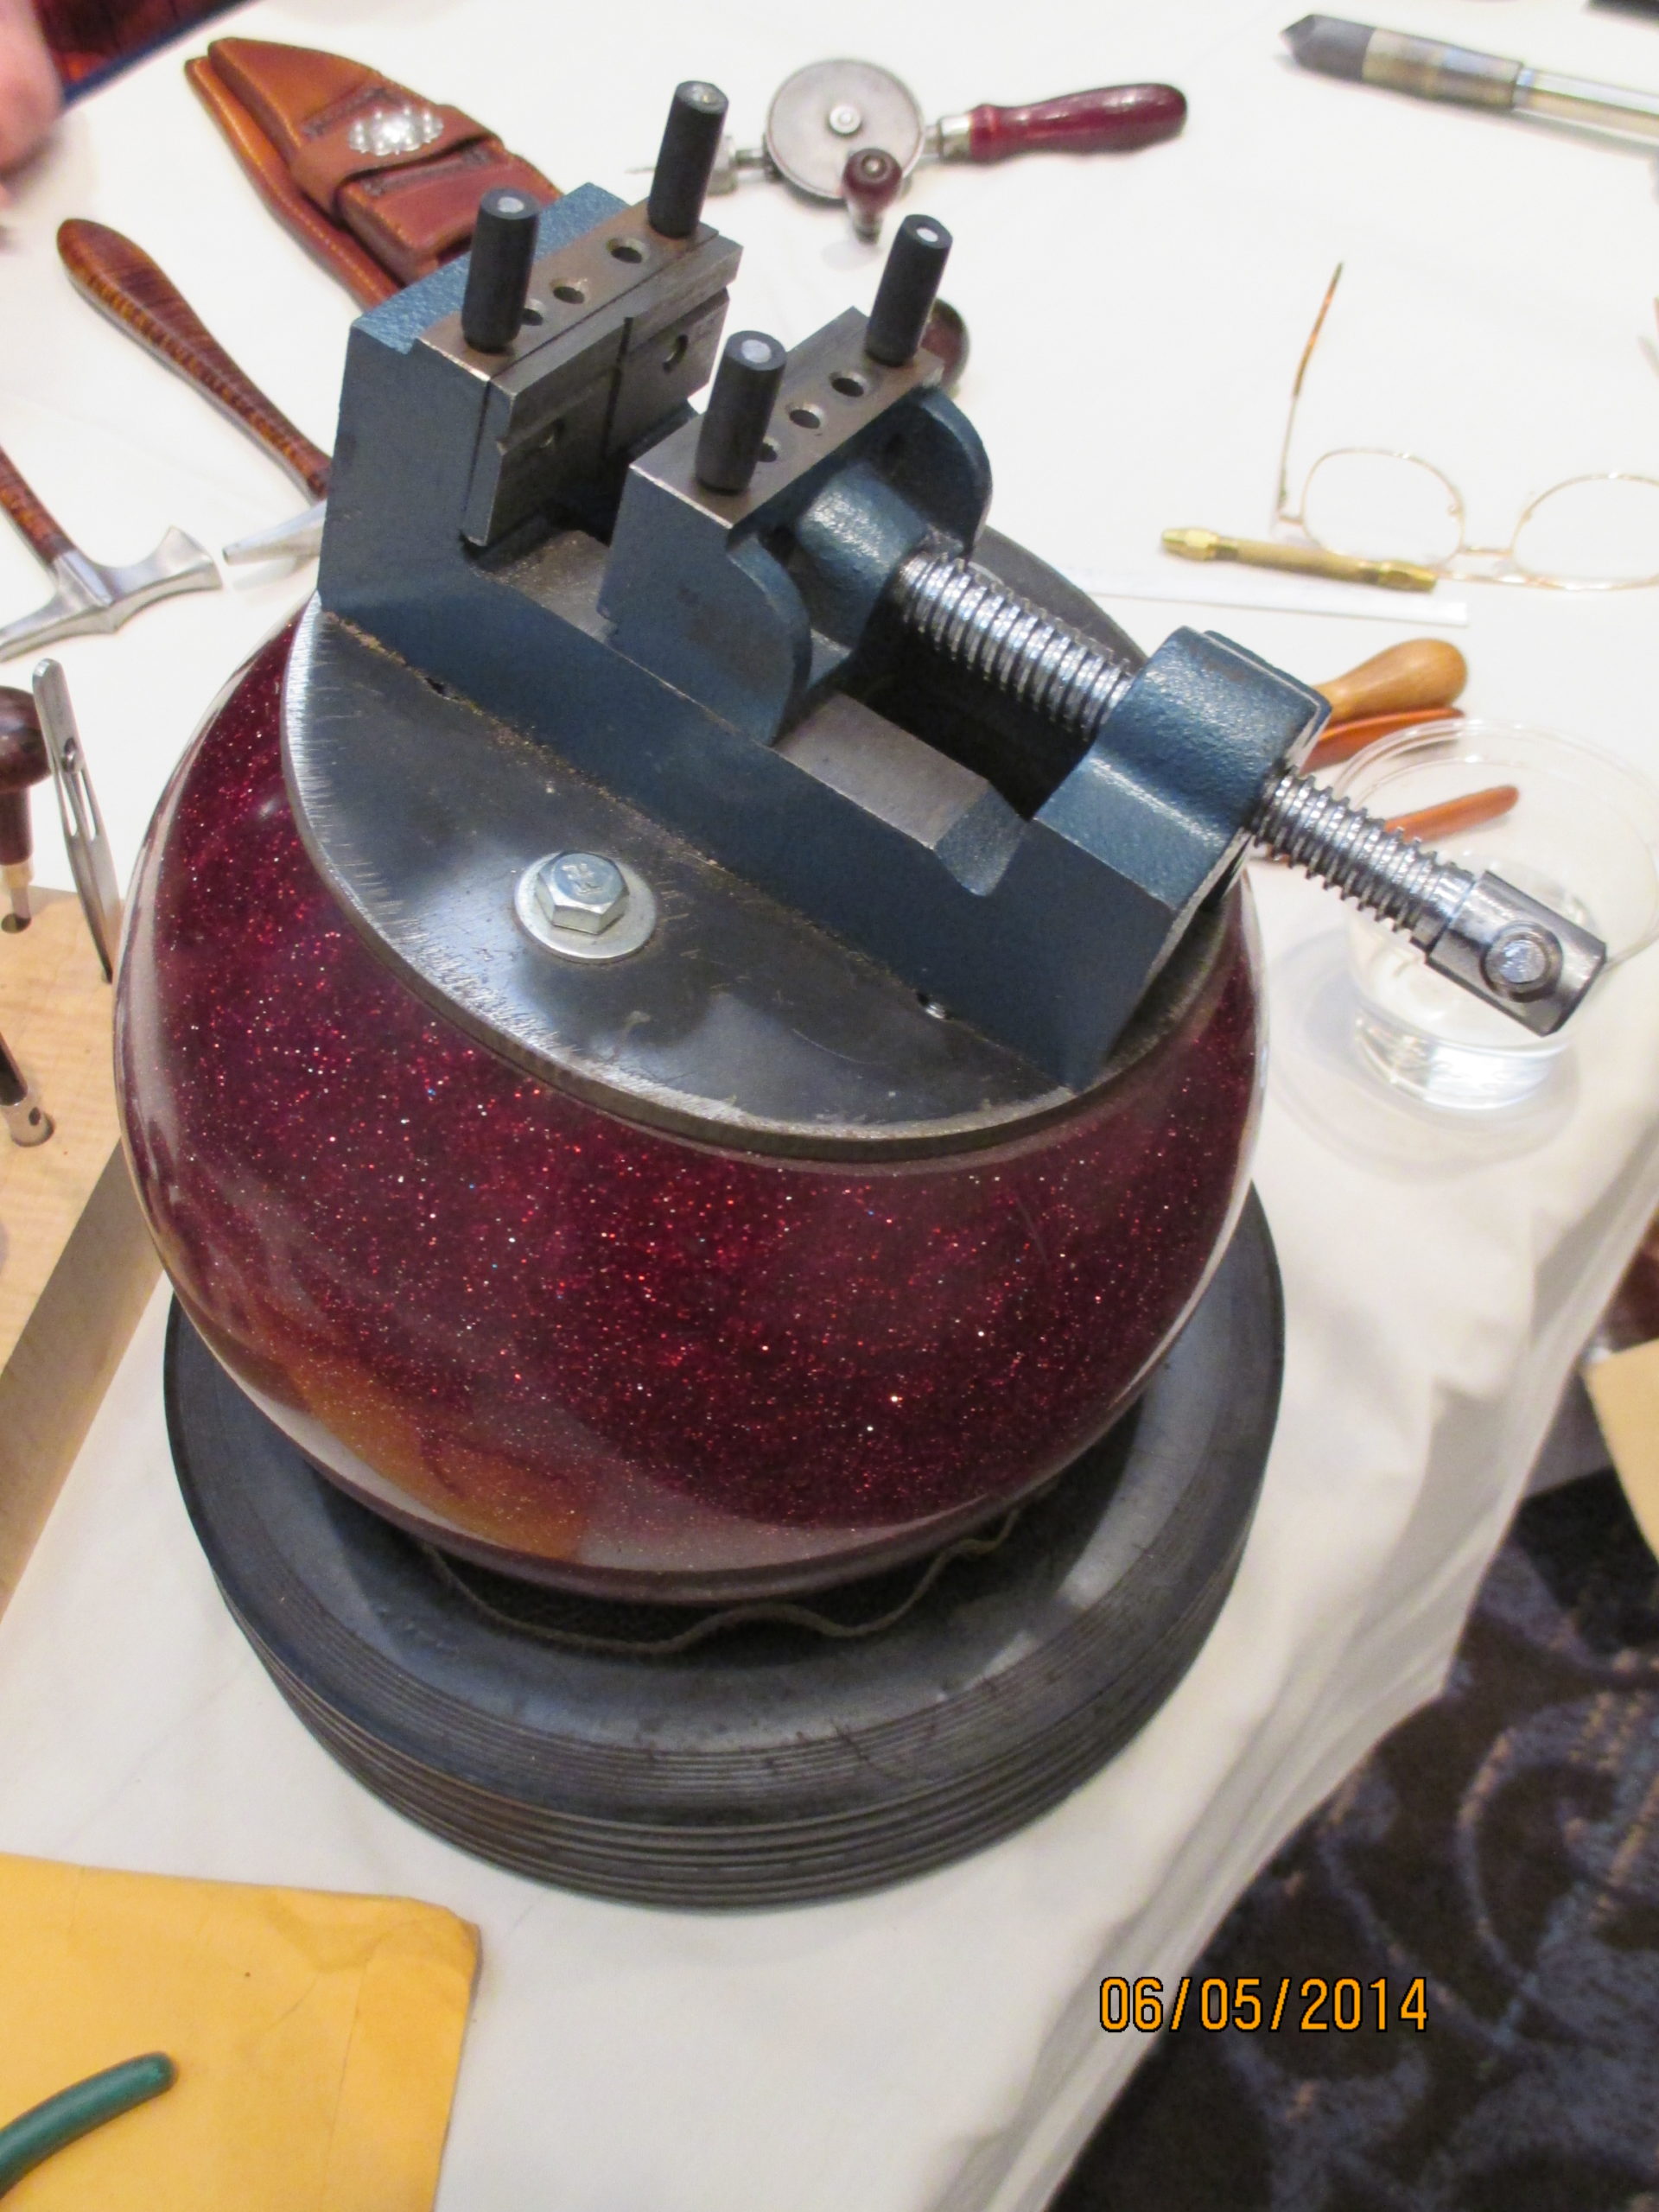
While the basics of making Hethcoat’s bowling ball vise are outlined in the below photo, there’s no reason you can’t add your own personal touches or substitutions. For instance, Don uses a piece of round pipe for the base of his vise, but Joe has a different way of skinning the cat. “My bowling ball sits in a lawn mower tire with the rim removed,” Keeslar notes. “It’s best to have a tire with rim diameter of about 6 inches. If no used tire is available, a new one can be found at a Harbor Freight store.”
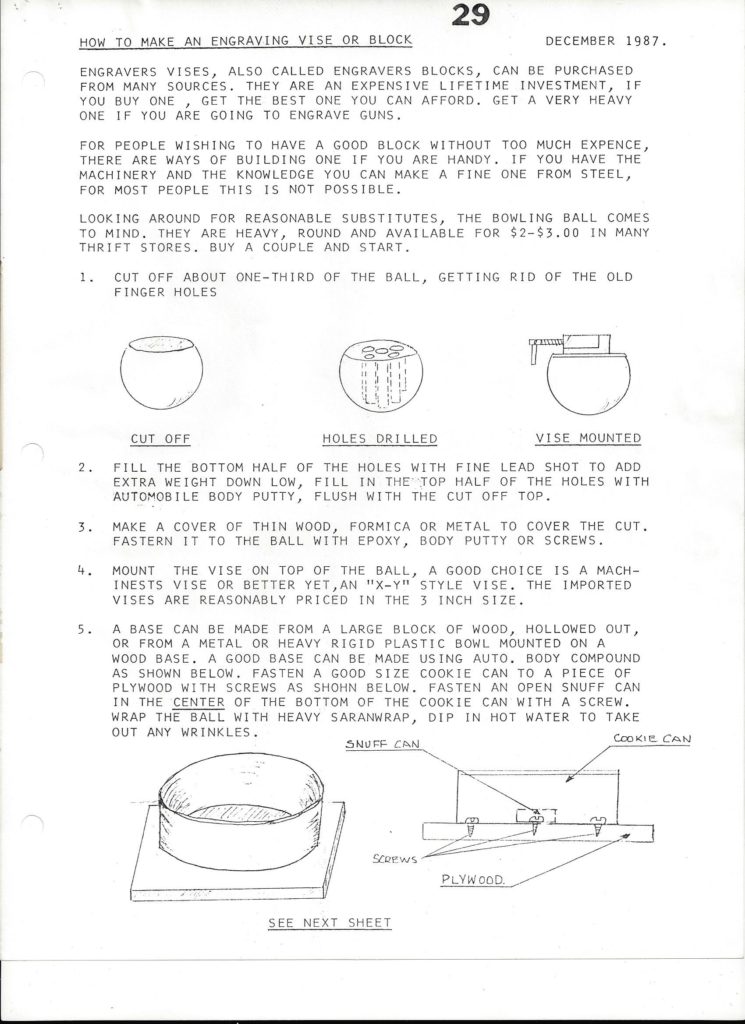
There are other differences between the two makers’ vises. Hethcoat uses a bench-mount machinist’s vise mounted to the top of his modified bowling ball, while Keeslar prefers a low-profile drill-press vise commonly used for drilling and milling. Both vises work fine and your choice may be determined by factors such as your height in relation to your workbench or the configuration of the vise jaws that suit you best.

The jaws of the vise will need to be padded to keep from marring the knife handle. Here again, choose your preferred padding material. Thick leather will work as well as high-density foam—or take a look around your shop and use your imagination.

ROLL on a BUDGET

As a long-time instructor on how to make knives, Keeslar says beginning students may not have the money for expensive equipment, so he uses his bowling ball vise as an example of how they can get started without a huge investment.

“I personally use an engraver’s ball for my silver wire inlay, but the bowling ball vise is very inexpensive to make and affordable to use,” Joe observes. “When doing demos here in the U.S. [and abroad], I use the bowling ball vise to demonstrate to my students an easy way to get started in doing wire inlay. I also show them how to make the stabbing chisels and the like. So much of what is needed to produce knives is expensive and this is one activity that one can do for a small investment.”

It’s all about saving money. The extra cash you save by making a bowling ball vise can be poured into better handle materials—everything from wood to wire. This translates into a more upscale knife for your own satisfaction or, if you sell your wares, a higher price you can get from a customer. You’re a winner either way!

6 Easy Steps to Make the Bowling Ball Vise

According to ABS master smith Don Hethcoat, “Bowling balls make the perfect vise for knifemakers doing inlays and similar close work where you need both stability and flexibility. You can buy an old bowling ball at a flea market or thrift store for two or three dollars.”

In his own words, here are Don’s six steps:

1) “Saw off about one-third of the bowling ball, getting rid of the old finger holes. I used a metal band saw but you may have other means”;

2) “Drill five holes in the flat top of the ball, one at each corner of a square with one in the middle using a half-inch drill bit, then chisel out a cavity in the center of the ball”;

3) “Fill the opened cavity almost to the top with lead shot to add weight, then seal the shot to the top of the hole with automotive Bondo® filler”;

4) “Make a round cover for the flat top of the ball using metal, wood or Formica®. Mount your vise on top of this. Mine is a machinist’s vise using its mounting system”;

5) “Make a base and you’re almost done. I used a round piece of 8-inch pipe cut to 2.5 inches in depth. Fill the pipe with Bondo, cover it with Saran™ Wrap and push the bottom part of the ball into it to make an impression. Clean up the excess Bondo [or, you can use the lawn mower tired described by Joe Keeslar in the story]”;

6) “Cut a round piece of suede to fit inside the round cavity so the ball can rotate freely. That’s basically it! Feel free to modify the vise to fit your own scenario.”
Custom-Made Chef Knife: The Kitchen Integral

0

One-piece custom-made chef’s knives embody strength, balance, line and flow and more

By Mike Haskew

As it does in other aspects of custom knives, integral construction, with blade bolster, tang and pommel forged from a single piece of steel, has its application in the kitchen. ­The high-performance chef ’s knives that result from such a construction provide an excellent opportunity for skilled knifemakers to showcase their abilities. Function is always at the forefront. After all, First and foremost, all knives must cut. So, chopping, slicing and dicing ability, comfort in the user’s hand, edge-holding properties, and easy maintenance and upkeep are prerequisites. To step it up, consider chef ’s knives that blend the basics in their efforts to raise the game. Good looks are indeed a bonus, and the featured models deliver with delicious damascus, tantalizing handles and overall presentation that will keep you in the kitchen just for the sheer pleasure of manipulating them.

FORM & FUNCTION TO CONSIDER FOR CUSTOM CHEF KNIVES

When Gabe Mabry of Norwood, North Carolina, cooked up a kitchen stunner with a 300-layer ladder-pattern damascus blade forged in partnership with Steve Grosvenor, he took the principles of form and function to heart.

“­There’s something about an integral chef ’s knife,” he said. “Forging it connects bladesmiths to their forebears. With all the modern technology, there’s only one way I can think of to manufacture an integral chef ’s knife—and that’s to forge it to shape. A well-executed integral will have impeccable balance and design flow that seems intuitive. Conversely, much toil went into the shape.”

 Mabry’s piece was constructed for a specific client order. ­ The damascus is forged from a combination of 80CrV2, 52100 and CruForge V carbon and 15N20 nickel-alloy steels. ­ e handle of ancient walrus ivory is tapered with a slight curve and accented with the owner’s initial in the butt.

“­The construction of an integral is a labor of love,” Gabe commented. “However, all the work and care of setting up the bolster makes the handle assembly simpler to a degree, with the inclusion of up to an inch of metal in the bolster. ­ is inch of material can be subtracted from the handle material, increasing the options in handle materials. Integral knife construction adds multiple steps and a degree of difficulty as well.”

While the fundamentals of any good working knife must be incorporated into the integral, the construction itself doesn’t apparently add or detract from the user’s experience. Balance, edge, comfort and dexterity, durability and cleanup still matter. And the last attribute is perhaps one where an integral has an advantage.

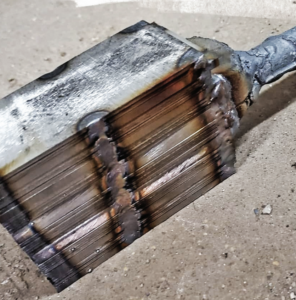
Above: A stacked billet is ready for more forging in Gabe Mabry’s shop. (Gabe Mabry image)

“An integral knife has its benefits,” offered Charlie Ellis of Eagle Crest Forge in Asheville, North Carolina. “And when done well it is very strong, with a minimal number of joints to become problems with material movement or becoming a possible breeding ground for bacteria. Also, it minimizes potential issues with wood movement. Having the joint positioned where there is the least chance of movement and using stable material is a wise choice.”

The HEXAGRAL CUSTOM MADE CHEF KNIFE

Ellis created a beautiful integral chef’s knife with a 10-inch damascus blade of 1095 spring and 15N20 nickel-alloy steels in a radial laddered W’s pattern, and an “S” grind for less resistance in the cut and better food release. The handle is African blackwood with silicon bronze and G-10 fittings. “It’s big but light for its size and balanced perfectly for a pinch grip,” Ellis explained.

The knife is fashioned in a distinctive style Charlie calls the hexagral. “I call this design the hexagral as a nod to my friend [and ABS master smith] Haley DesRosiers, who makes octagonal-shaped integrals she calls octagrals. With the hexagral, the integral bolster is shaped in a hexagon, both in cross-section and, quite challengingly so, on the faces.

“Compared to typical hidden-tang construction that is limited by the spine thickness, an integral can have a truly robust tang. Also, with this knife, the tang runs through to be bolted and capped on the end so that if for some reason the ep- oxy failed, there is a mechanical connection keeping it tight.

“So,” he continued, “while there are some practical bonuses to an integral, I would have to say that what draws me to them, and why I choose to make them the most, is their artistic potential. Seeing the pattern condensed in the bolster and then flowing out into the blade is always one of my favorite parts. Between that and the sculptural aspect of the transition between the blade and handle, there are so many interesting possibilities. I al- ways get excited with each new integral I create.”

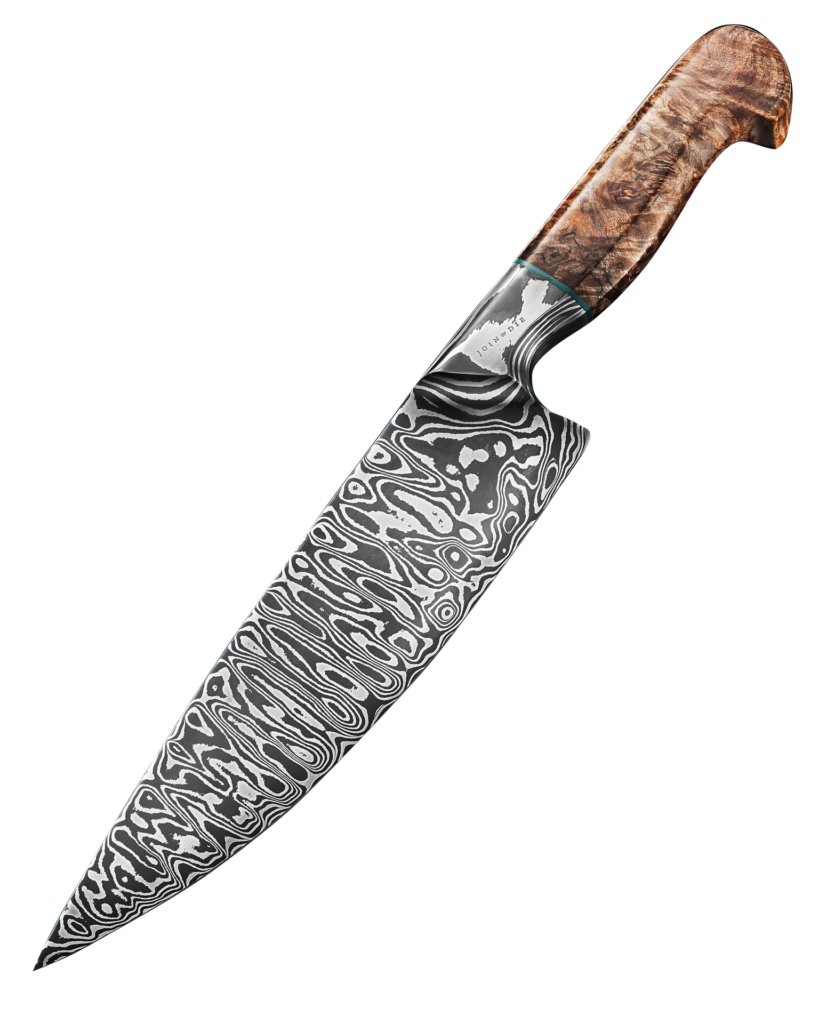
Brent Stubblefield of Join or Die Knives in Richmond, Virginia, finds the challenge of integral construction one of the most appealing aspects of the undertaking. “Integral-construction chef’s knives are special because the production meth- od cannot be counterfeited,” he reasoned. “Standard stock removal processes can- not be used to make them, and machining processes, while an art unto themselves, cannot produce the flowing patterns that a forged damascus blade can.”

Brent Stubblefield’s chef’s knife features an “S” grind with hollow ground “cheeks,” while the cutting edge is flat ground up to about one-half inch above the edge to assist in food release. Depending on the pattern, Brent’s price for a similar knife ranges from $850 to $1,500. (Caleb Royer image)

For Stubblefield, the integral’s functional advantage lies in the flow of the handle, its uniqueness and strength rather than any perceived upgrade in edge performance. Integral construction, he says, should provide a blank canvas for the maker to use any shape or geometry desired. In this case, the style does not inherently improve edge geometry but al- lows for infinite possibilities.

“Larger stock must be used for integral construction,” he explained. “I usually use at least 1-inch round stock and, when making damascus, I leave the stock at 1 inch by 2 inches, plus the desired length. There must be enough thickness to leave material for the bolster and tang as well as drawing them out, and there must be enough blade material to draw the heel back toward the handle. In considering integral. hidden-tang-with-guard and full-tang knives, each has its pros and cons Quality material plus excellent fit and finish bring those differences down to the level of nuance. The standout advantage of the integral is the strength of the seamless connection of blade and bolster.”  

“A WELL-EXECUTED INTEGRAL WILL HAVE IMPECCABLE BALANCE AND DESIGN FLOW THAT SEEMS INTUITIVE.” -GABE MABRY

Brent’s chef’s knife has an 80-layer ladder pattern damascus blade forged from 1084 carbon and 15N20 nickel-alloy steels. The blade features an “S grind with hollow ground cheeks while the cutting edge is flat ground up to about one-half inch above the edge to assist in food release. The Virginia maple burl handle is fashioned in the style of French Sabatier chef’s knives with extra wood at the end to help balance the longer blade. A G-l10 spacer provides a subtle accent.

“Integral knives have fewer seams when built in a hidden- tang fashion, he added. “There are no inside corners where handle or bolster material terminates. So, the integral may be easier to keep clean and free of food particles. Although we do our best to seal our handle material to the tang with epoxy, there is always a possibility of liquid intrusion, So, the more seams around the tang, the more chances of infiltration. I’m building knives with the intention for multiple lifetimes of use, so I prefer any advantage for longevity.”

ADDED STEEL MASS

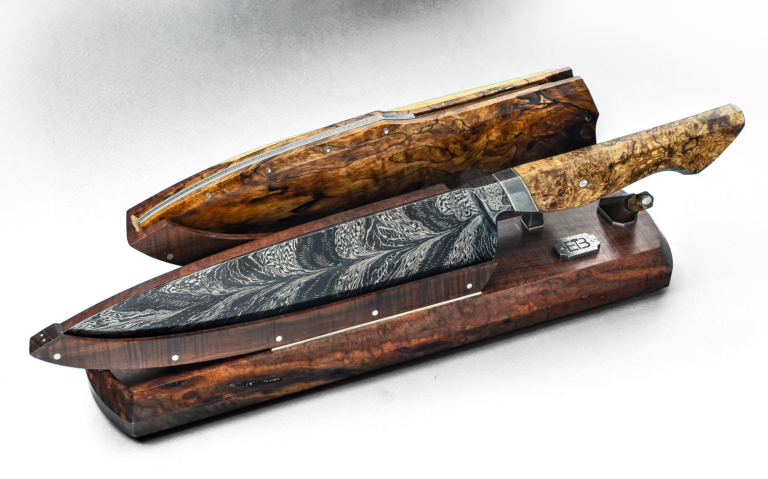
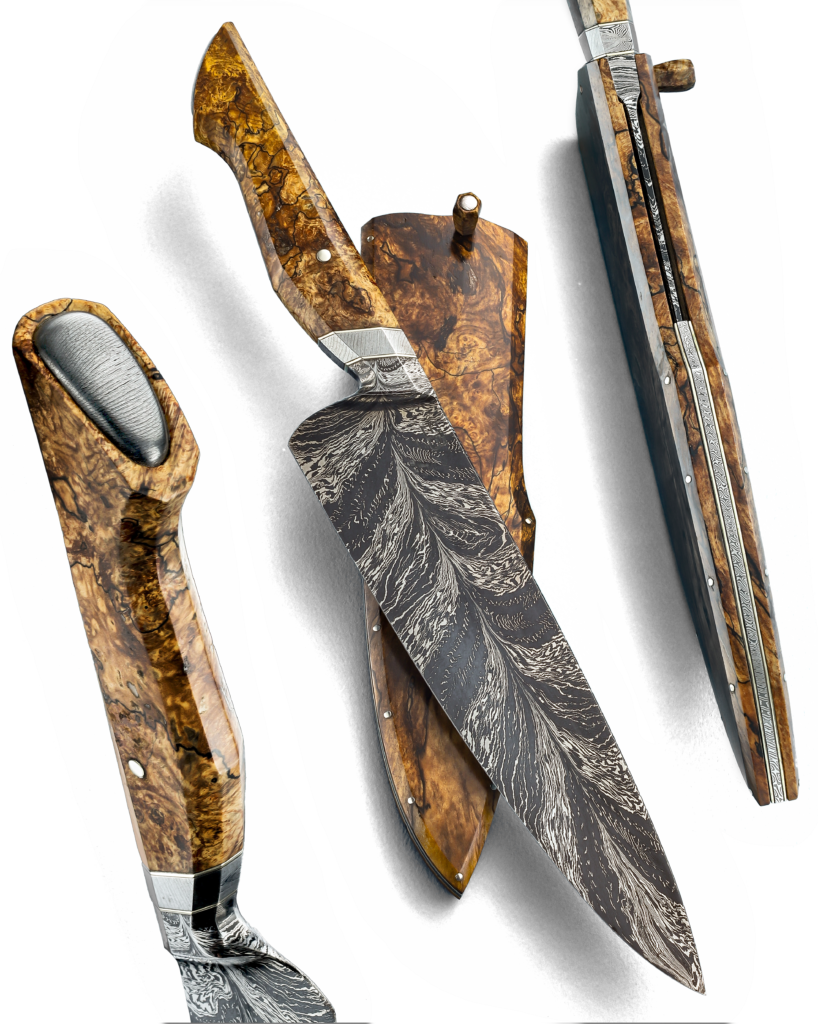
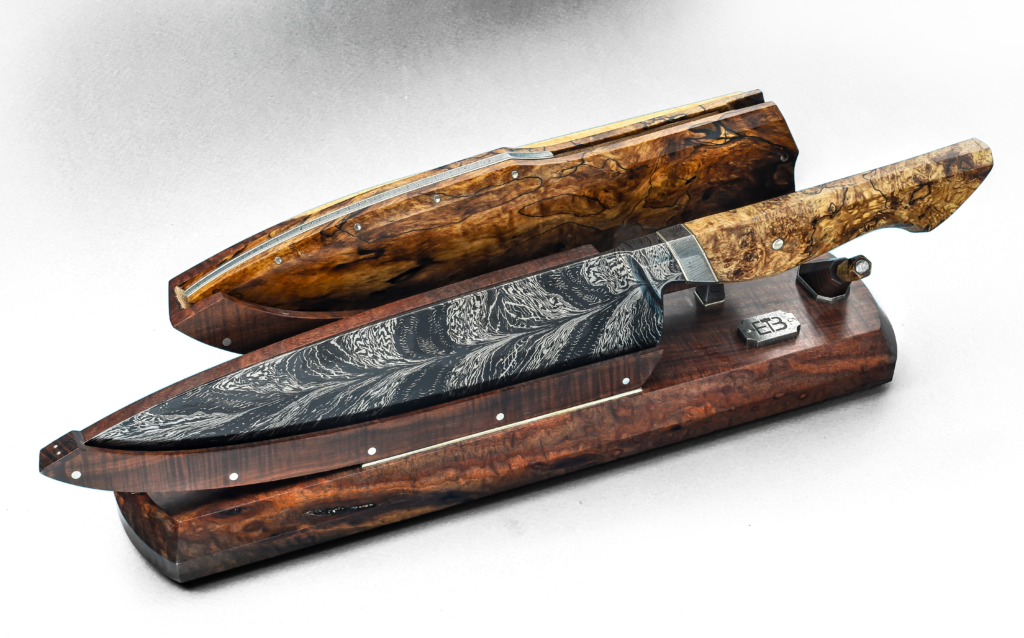
Jason Ellard of Coningham, Tasmania Australia, built a mosaic integral chef’s knife with an 8.86-inch blade of feathered damascus in 1084 and 1SN20 steels, spalted sassafras burl handle with a domed pin and twist damascus inlay, and an accompanying sheath in frame construction and nickel-silver and twist damascus to match the spacer. Overall length: 14.76 inches.

Jason Ellard’s mosaic integral chef’s knife boasts an 8.86-inch blade of feathered damascus in 1084 and 15N20 steels. Overall length: 14.76 inches. Jason’s price for a similar custom made chef knife: $7,000. (SharpByCoop image)

“The forward angle of the bolster- blade transition allows for easier stone sharpening,” remarked Jason. “Handle spacers are made from nickel-silver and twist damascus with broken edges for a nice feel. The handle also has proven edges, which help with stopping a hard ridge at the transition if the wood ever swells or shrinks. I carved out a recess to allow the bolster to fit inside the sheath, and the stand is ringed gidgee with damascus pegs raising the back portion and a nickel-silver plate under the front section. The sheath pin has a twist damascus inlay and its own designated holder on the stand. Lastly, I created a mosaic damascus logo plate pinned onto the base of the stand.”

Ellard approaches integral construction with a full understanding of its difficulty. “It takes a lot of skill in every aspect of creating it,” he observed, “and even more so to do it well. The forging, grinding, symmetry, handle fitting, and hand finishing are all a lot more difficult to do than other constructions, and it’s a major staple of a skilled maker to do this with a high level of quality. I person- ally just enjoy making integral knives a lot more. I find it more pleasing to the eye, and I enjoy the added challenges in creating them, allowing me to show what my skills are capable of.”

The stand for Jason El- lard’s chef’s knife is ringed gidgee with damascus pegs raising the back portion and a nickel-silver plate under the front section. The sheath pin has a twist damascus inlay and its own designated holder on the stand. Jason created a mosaic damascus logo plate pinned onto the base of the stand. (SharpbyCoop Image)

According to Jason, the added steel mass of the integral will always make the knife more solid and heavier than other types. Performance is a key attribute, though other kitchen knives are comparable in many ways. “The performance shouldn’t be affected negatively or positively as long as the knife is made correctly,” he noted. “The lack of a hard 90-degree at the ricasso in a hidden-tang knife can make cleaning a lot more difficult. It also makes it easier for debris or moisture to get into the handle. With the integral construction moving the seam further back, it takes these issues away very well. I’ve also found it easier to get a tight fit against an integral bolster than a hidden- tang ricasso.”
Integral construction in a chef’s knife adds another dimension to the artistry that is custom knifemaking. In fact, an appreciation of the skill and execution of the integral may actually push the chef to new heights of culinary creation.


Knifemaking: How to Make Temper Lines

0

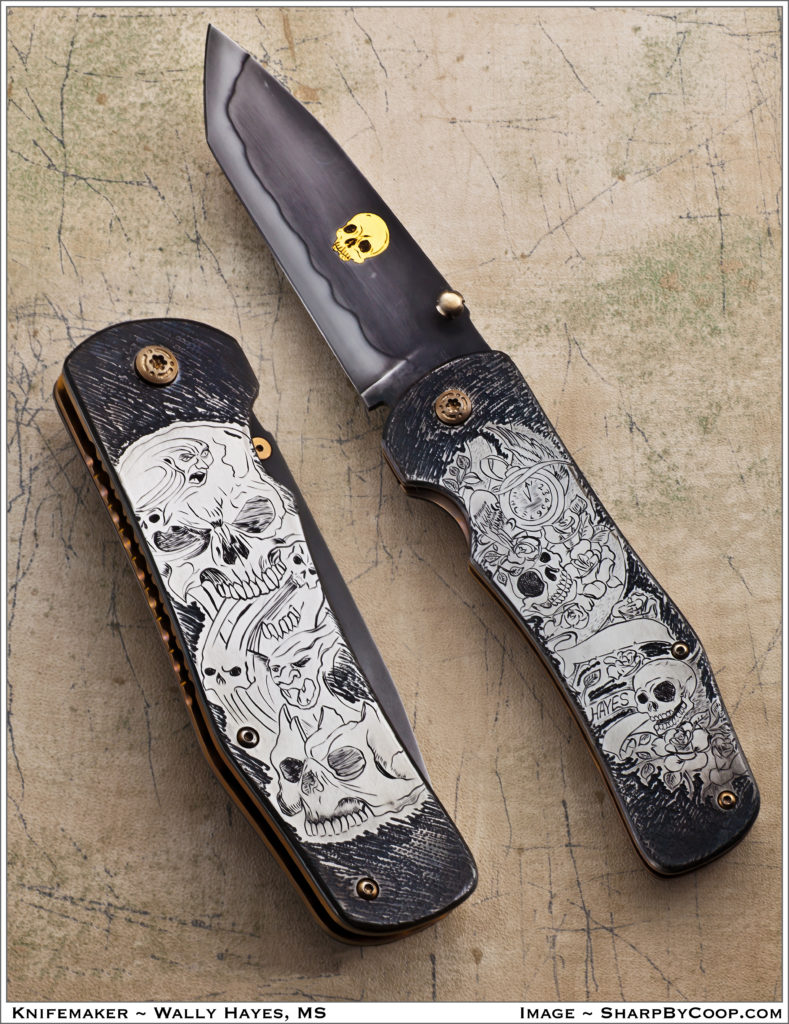
Temper lines—aka hamons—are a very exciting part of knifemaking, and I would like to share with you how I produce cool temper lines on folders. -Wally Hayes


The latest folder exhibiting a handsome temper line—aka a hamon—by the author (inset) is this skull-encrusted model. (SharpByCoop knife image)

STEEL and CLAY

First you need to select your type of steel. You can use 1084 carbon steel or high-carbon damascus, but I prefer W2 tool steel. I get mine from New Jersey Steel Baron because I can get it surface ground to whatever thickness I need.

The W2 is low in manganese, enabling you to create wild temper lines. I grind the blade leaving the edge about the thickness of a dime. The thickness helps prevent your blade from warping in the quench and also helps hold the heat, giving you time to get the blade into the quenching oil.

The clay I use is a stove furnace cement used to repair fireplaces and chimneys. I get mine at the hardware store and it comes in a small tub or a tube like the tubes of silicone used with a squeeze gun for calking.

APPLYING the CLAY

To apply the clay I use a sharpened Popsicle® stick, being careful not to put any clay where the ball bearing in the liner will travel on the tang of the blade. Also, do not put any clay near the pivot hole as you want that area to become fully hard when quenched.

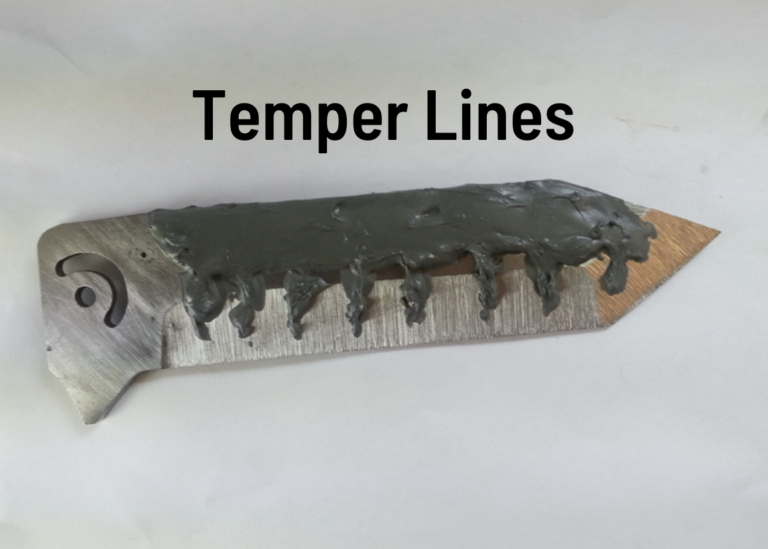
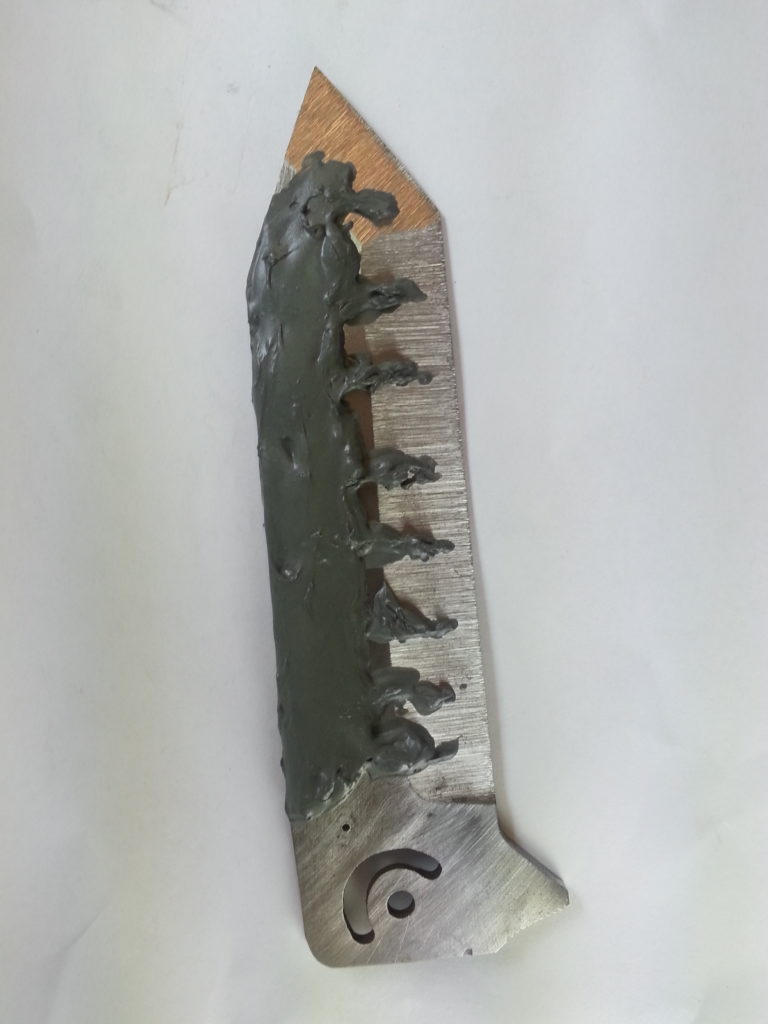
I like a very exaggerated temper line with big waves. You can achieve this by placing short lines of clay every half inch down the blade. Do not carry the clay line all the way to the edge as you want the edge fully hard.

1) The author likes very exaggerated temper lines with big waves. You can achieve this by placing short lines of clay every half inch down the blade.

I put the clay on the blade about an eighth of an inch thick. This seems to work very well. Let the clay dry for about four hours before you heat treat it. To heat treat the blade I use a propane forge. I place a coat hanger through the pivot hole and twist it around the tang of the folder to give me something to hold onto. 


HEAT and QUENCH

Gently heat the blade near the opening of the forge for a minute before placing it into the forge edge up. Watch the blade come up to temperature, placing the tang near the hottest part of your fire. The tang is the thickest area of the blade and slowest part to get up to critical temperature. Heat the blade until a magnet does not stick to it. I use a cow magnet on the end of a pipe and keep testing the blade as it heats up to temperature.

When a magnet does not stick to high carbon steel the steel is at critical temperature, at which point the blade should be removed from the forge and quenched in oil. For steel, I use a fast-quench oil such as the kind from Parker or Fensoil. I have also done many successful quenches in vegetable oil.

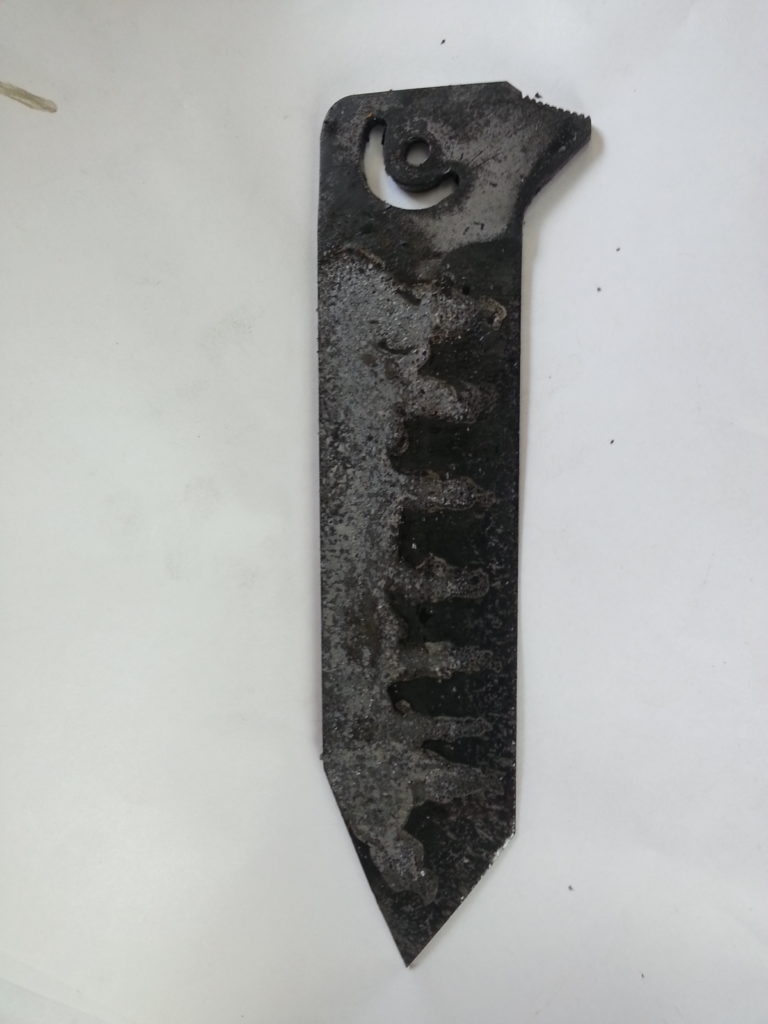
2) Here is the blade after quenching. The author uses a fast-quench oil such as the kind from Parker or Fensoil. He also has done many successful quenches in vegetable oil.

I quench the blade and then leave it submerged for two minutes before removing it. Once its out, I clean the blade with a paper towel. I then put the blade in the toaster oven for one hour at 385°F.

WARP CHECK, GRIND and POLISH

After the blade is cool I check it for straightness on a flat piece of steel. I use a set of parallels for this. If the blade is warped, I clamp it to a slightly curved piece of thick steel, and press the warp out with the twist clamp. Then I place the clamped blade in the toaster oven for another hour’s worth of temper at 350°F. This works really well and is less stressful to the blade when compared to trying to straighten it another way.

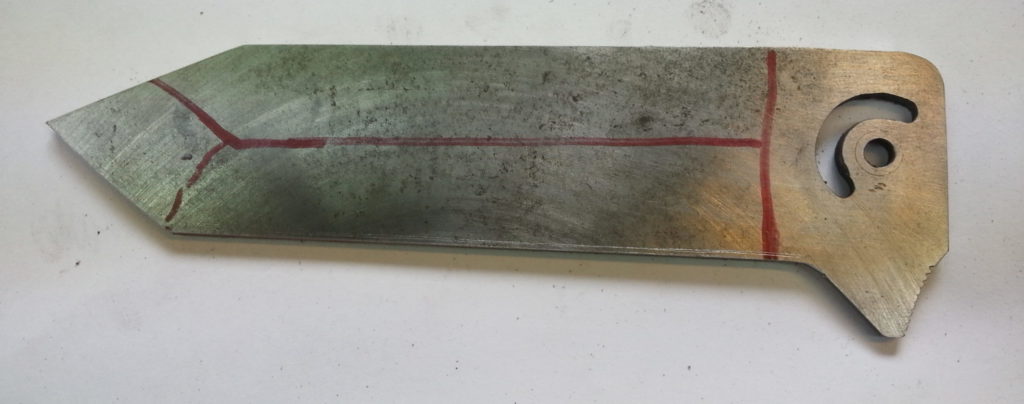
3) The red marks served as guides for the finish-ground blade.

Once the blade is straight it is time to finish grind and polish it up to 2,000 grit. I do the final polishing by hand to ensure every scratch has been removed. After this I sharpen the edge and make sure it is also polished carefully. Finally, I use sand paper backed up by a thick piece of leather and sand very slowly so I don’t cut myself.

The ETCH

Next up: Etch the blade to bring out the temper line. Clean the blade with acetone. Wear latex gloves to protect your hands and to keep oils from your hands off the clean blade. To etch the blade I use ferric chloride diluted four-to-one with distilled water—that is, four parts water to one part ferric chloride. Hang the blade with a cotton string tied through the pivot hole and place it in the acid for 15 seconds. Remove the blade from the acid and spray it with Windex®. This neutralizes the acid and stops the etching. Dry the blade and coat it with WD-40®. Rub a little bit of polishing compound onto the blade to remove some of the residue from the etching. I use Flitz or Peek polishing paste with a paper towel and some WD-40. Polish lightly and be very mindful of the sharp edge. Clean the blade with WD-40 and wipe off any excess oil.

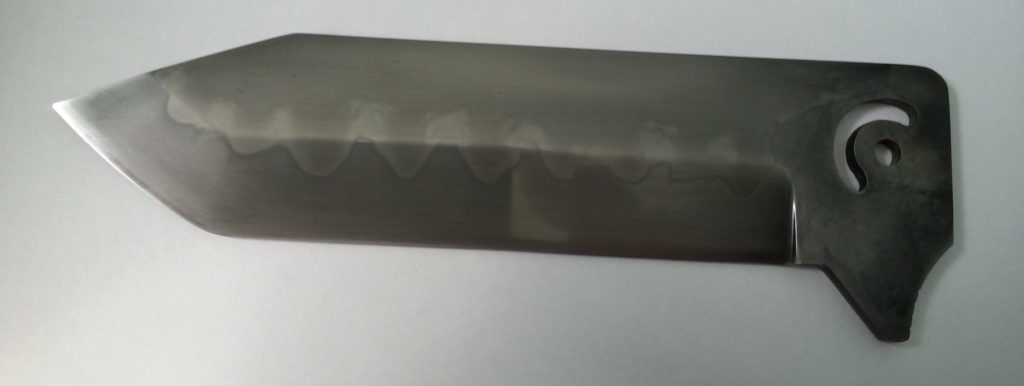
4) Here is how the blade appears after polishing and etching. The temper line is now visible.

To get the temper line white, go over the blade lightly with a piece of 3,000-grit-or-higher sandpaper.

I hope this gives some insight into the fun world of temper lines and more people will experiment with this fun process.

Above: The blade of the author’s finished folder exhibits a temper line with big waves—just the way he likes it.

For more information contact Wally Hayes, 9960,9th Concession, RR#1, Essex, ON, CanadaN8M-2X5 226-787-4289.

How to Do Plug Welds on Knives

0

Plug Welds the David Lisch Way

The ABS Master Smith shows how he puts a plug weld in a damascus blade

On this and the following pages, I will show you how to do a plug weld. Firstly, this is not a new technique. That being said, I would like to think that the way I am using it here is new—or at least it is new to my knives. I’m not showing how I made the damascus pattern as it would take way too many photos. Perhaps I will show that in another story.

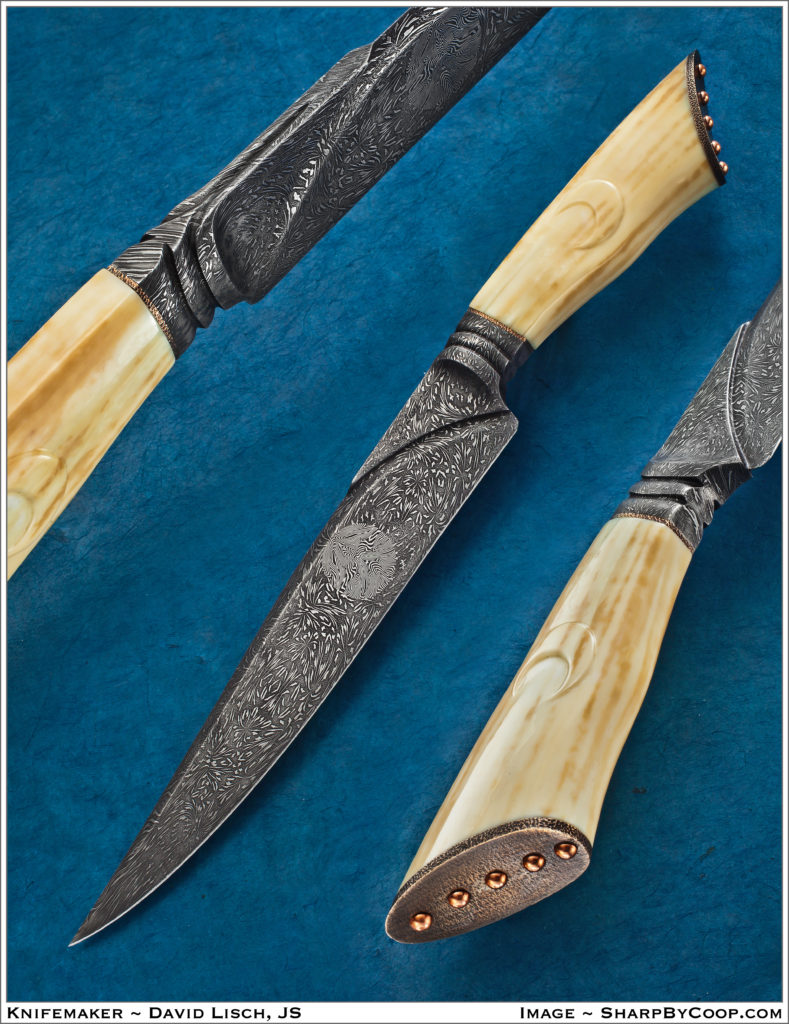
The Moon Fighter is one of two knives I have made in this style. The first one was the Sun Fighter. The Sun Fighter was the first time I made a knife using the plug weld technique. I took an order for a knife like the Sun Fighter. Since the resulting knife was slightly different, therefore I named it the Moon Fighter.

HOW DAVE DOES IT

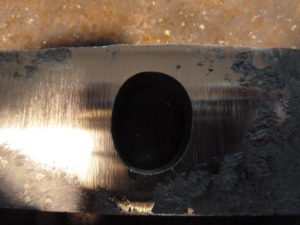
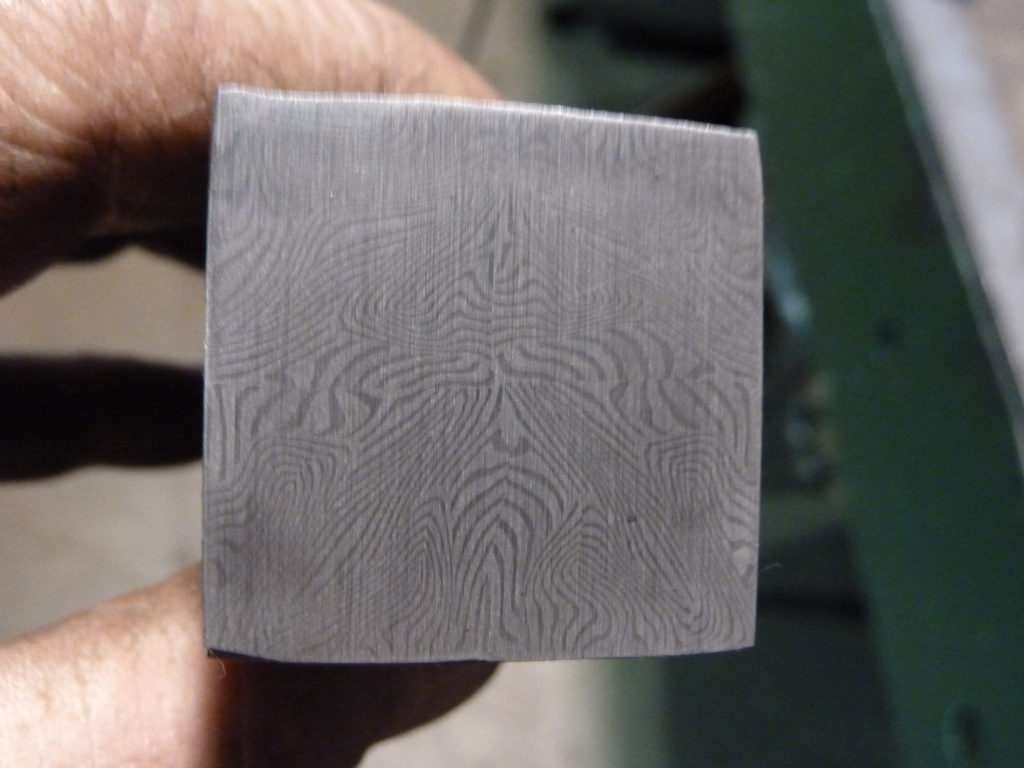
In Photo 1, I am cutting an oval hole into a forged integral blade. I forged the blade from a billet of my Star Night Damascus (Photo 2). It is important that the hole be an oval shape so it will be round once it is forged (Photo 3).

3: It is important that the hole be an oval shape so it will be round once forged.

Blade thickness is just over 3/8 inch. This will give me room to forge the blade once I make the plug weld. Photo 4 shows the end of the moon billet. I will shape the square into the oval to the make the plug for the “moon.”
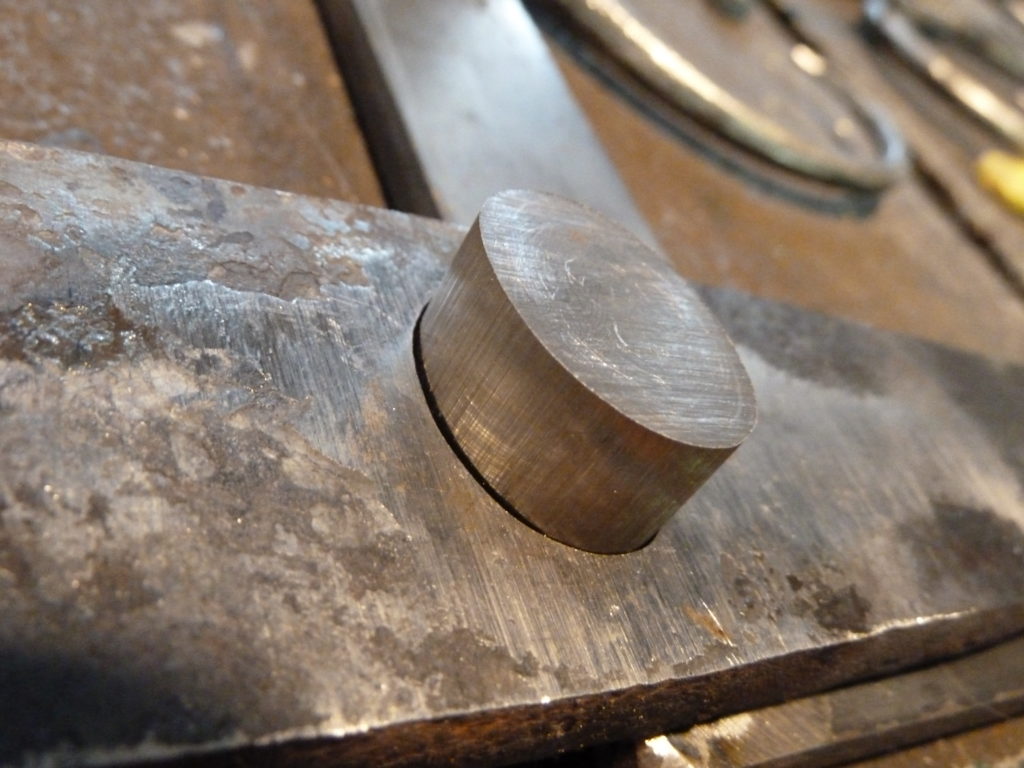
In Photo 5 you can see that the plug is ready for insertion into the hole. It is close to the right size but just a bit big. I put a slight taper on the edge of the plug so it can “find” the hole. The plug is an eighth inch thicker than the blade. This will allow the plug to expand and weld into the blade.
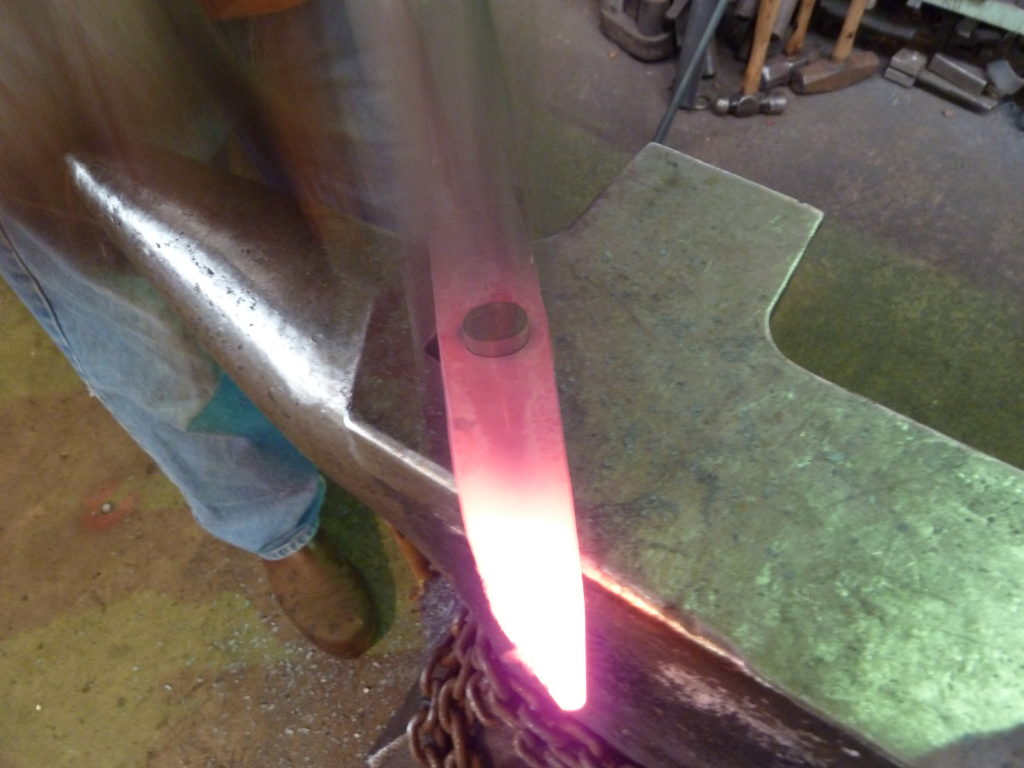
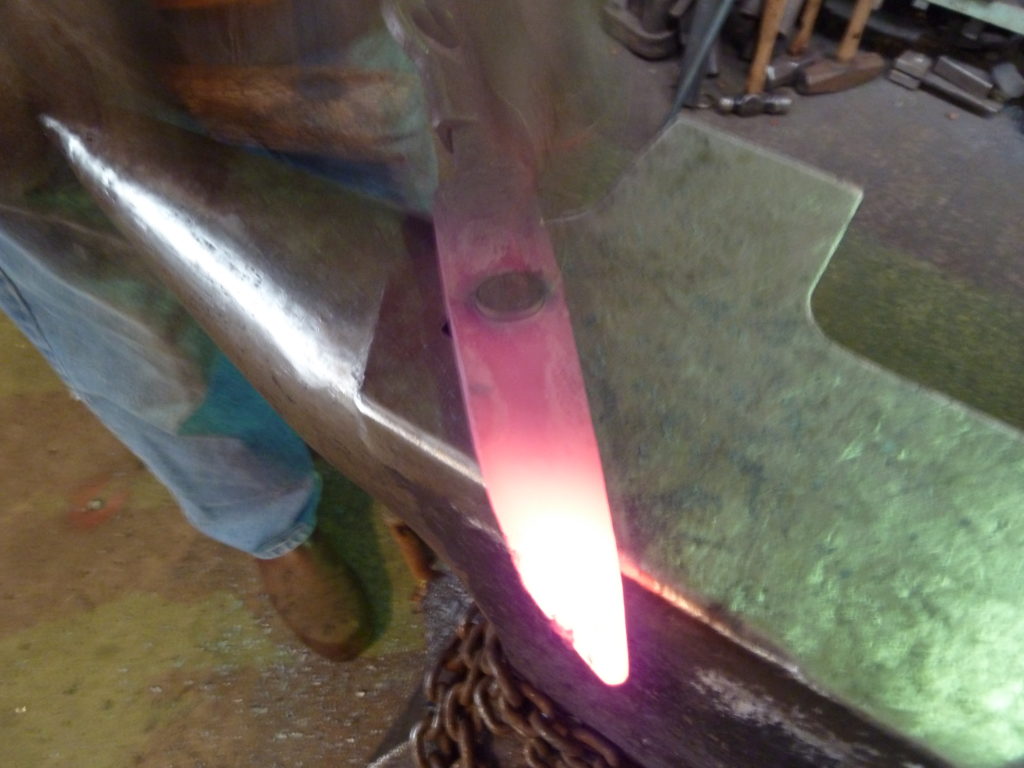
Above Photos 6 and 7: The hammer is a blur as the author pounds the plug into the hole in the hot steel.

With any process there is a learning curve. I learned that to get a really tight fit with the plug, it works best to put a dull red heat on the blade. Place the tapered plug into place and hammer it into the dull red blade (Photos 6 and 7). In Photo 8 the plug is in place. It is 1/16 inch proud on both sides of the blade. Back into the fire to a dull red and add flux.

In Photo 9 I have made the first weld. The moon is still visible. In Photo 10 the moon is still a bit cooler than the blade and is getting a bit bigger. Now is the time for some heat. Photo 11 shows work at the power hammer for some drawing down of thickness and adding length to the blade. It also makes the oval moon round and very hard to see.

In Photo 12 I am forging the blade close to its final shape. In Photo 13 I am drawing out the tip, adding more length to the blade. The moon is very close to being round. After a few final taps under the power hammer (Photo 14), I will finish tuning up the profile by hand.

NO SET FORMULA

I do not have a set formula for this process. It is by gut feeling. I can see how much the steel moves when I forge it. The first time I tried it I put a round hole into the blade and wound up with an oval, so it made sense to start with an oval hole if I wanted to wind up with a round one.

With the Sun Fighter the blade was 480-layer damascus and the “sun” was a very tight W’s-pattern damascus. Once I made the initial weld, the blade was still over 3/8-inch thick at that juncture. I ground in sunrays on both sides then forged up the rays and the sun to its round shape. On the Moon Fighter I wanted the backdrop to resemble shooting stars. This took some trial and error and a lot more time than I thought it would to get a pattern I liked.

The result of the plug weld made to resemble the moon is plainly evident in the center of the damascus blade of the Moon Fighter by ABS master smith David Lisch (inset). (SharpByCoop knife photo)

NO LIMIT

There is no limit to the cool new things that can be done with damascus. I have heard folks say it has all been done before. Well, I don’t believe it. I think new and exciting things are happening in little knife shops all over the world, and the only way to keep things moving forward is to try new stuff and share the new things with everyone we can.

Please feel free to try this process. There are so many different things that can be done with it. When you come up with something new, share it so we continue to advance the art of damascus and knifemaking. Or, buy a damascus knife from your favorite maker and watch for that sparkle in his eye as he thinks to himself, “Cool, now I get to make another knife.”

Marine Vet’s Knife Memorializes the Ultimate Sacrifice of His Iraq Comrades

1 Knife for the Lima Company 11

BY MIKE HASKEW BLADE® FIELD EDITOR

*This article originally appeared in BLADE Magazine Winter 2013

The bond of brotherhood, sacrifice, and selflessness forged by fighting men in combat is, perhaps, the strongest emotion human beings can experience. So it is with Travis Williams.

Having just turned 18, Travis enlisted in the United States Marine Corps In December 2001. He reported for duty the following August and spent the next four years in the service. While he trained, his original reserve unit had already deployed to Iraq, and he was among a few who were reassigned to Lima Company, 3rd Battalion, 25th Marines, another reserve unit, headquartered in Columbus, Ohio.

Travis Williams (second from right, back row) stands proud with his squad mere weeks before the deadly IED strike. (photo courtesy of Travis Williams)

During its deployment to Iraq, Lima Company endured days of patrols in harm’s way, intense firefights, and the ever-present danger of IEDs (Improvised Explosive Devices). With a strength of about 180 Marines, Lima Company lost 24 killed in action, and one in eight of its Marines received the Purple Heart for wounds received or death as a result of enemy action. By late 2005, Lima Company was the hardest hit unit of its size in the Marine Corps. Lima’s battalion lost 48 men killed in Iraq.


AUG. 3, 2005

Considering the tedium and tension that encompassed his time in Iraq, a single day stands out in Travis’ memory. On Aug. 3, 2005, during a patrol near the town of Barwanah, 11 Marines from his squad were killed in a massive IED explosion.

“We were going to start at 0600,” Williams recalled. “We loaded our amtracs, big transport vehicles, and about five minutes before we stepped off, a call came down from higher. For some reason the platoon commander and I got pulled out of our vehicle with 1st Squad and put in a vehicle ahead of theirs with Iraqi forces in it. We headed for town and weren’t going to take any roads in. It was about a month before we were to leave the country, and we had seen a lot of firefights and IEDs.”

After the patrol received word that the road was, in fact, clear, the catastrophic explosion erupted. “We hopped on the road, and right as we made the turn for town I was sitting down in the vehicle,” Travis continued. “Somebody has to stand up to provide security, and I saw the explosion in the glasses of the guy standing up in our vehicle.”

Williams still does not know why he and the platoon commander were ordered out of the vehicle that was hit. He was not injured. Fifteen men occupied the stricken amtrac, and he had known those Marines that were killed for more than a year. Among them was his best friend, Lance Corporal Aaron Reed of Chillicothe, Ohio.

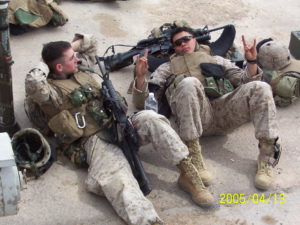
Travis and Lance Corporal Timothy M. Bell Jr., 1983-2005, enjoy some downtime. Bell, 22, was killed by the IED. His awards include the Purple Heart, Navy and Marine Corps Achievement Medal with Combat “V” for valor, and the Combat Action Ribbon. (photo courtesy of Travis Williams)

When Lance Corporal Travis Williams returned home to Missoula, Montana, in August 2006, he brought with him the memories and the scars of his wartime experience. He worked as a private investigator for about five years, and then an opportunity that he could not pass up presented itself. Always fascinated and intrigued by knives, he met custom knifemaker James Behring, Jr.

“James moved to Missoula from Michigan in 2011, and he married my friend’s sister,” Travis said. “I would hang out at the shop and watch what he was doing, and finally he told me that he was looking to hire somebody. I jumped in from there, cutting out blades from bar stock, soldering guards and finishing handles and stuff like that—until I was able to make a knife.”

GOLD STAR FAMILIES

This past February, the Wall Street Journal featured Travis in an article observing the 10th anniversary of the war in Iraq. “They wanted to know how I was doing,” he commented, “and there was a video with it and a guy followed me around the shop while we were making knives.”

A fellow Marine veteran saw the article and contacted Travis, telling him that a benefit was being organized for Gold Star Families in Ohio. These are the families of those who have lost a loved one in battle. “He asked me to make a knife for a silent auction, and the proceeds would go to support the work of an artist that was painting life-size portraits of the guys that were killed from the company,” said Williams. “It was on short notice because the event was going to be in three weeks. I cleared it with James and then contacted Roger ‘Mudbone’ Jones of Waverly, Ohio, to make sure he could make the sheath if I got the knife to him in time.”

Mudbone is an accomplished knife and sheathmaker in his own right. A friend of the Behring family who considers James Behring “like my own son,” Mudbone agreed to make the sheath. His relationship with Travis has grown as well, and he simply considers the former Marine a second son. In fact, it is Mudbone who brought this compelling story to the attention of BLADE®.

“Travis called and said he wanted to tell me about the knife and get some pointers on it and the sheath,” Mudbone remembered. “It knocked me out when he said this was for his friends, and particularly his best friend who had been killed. It turns out Aaron Reed was from my hometown, Chillicothe, Ohio. I had never met the boy, but I knew of his mother, who had been a teacher in a local school.”

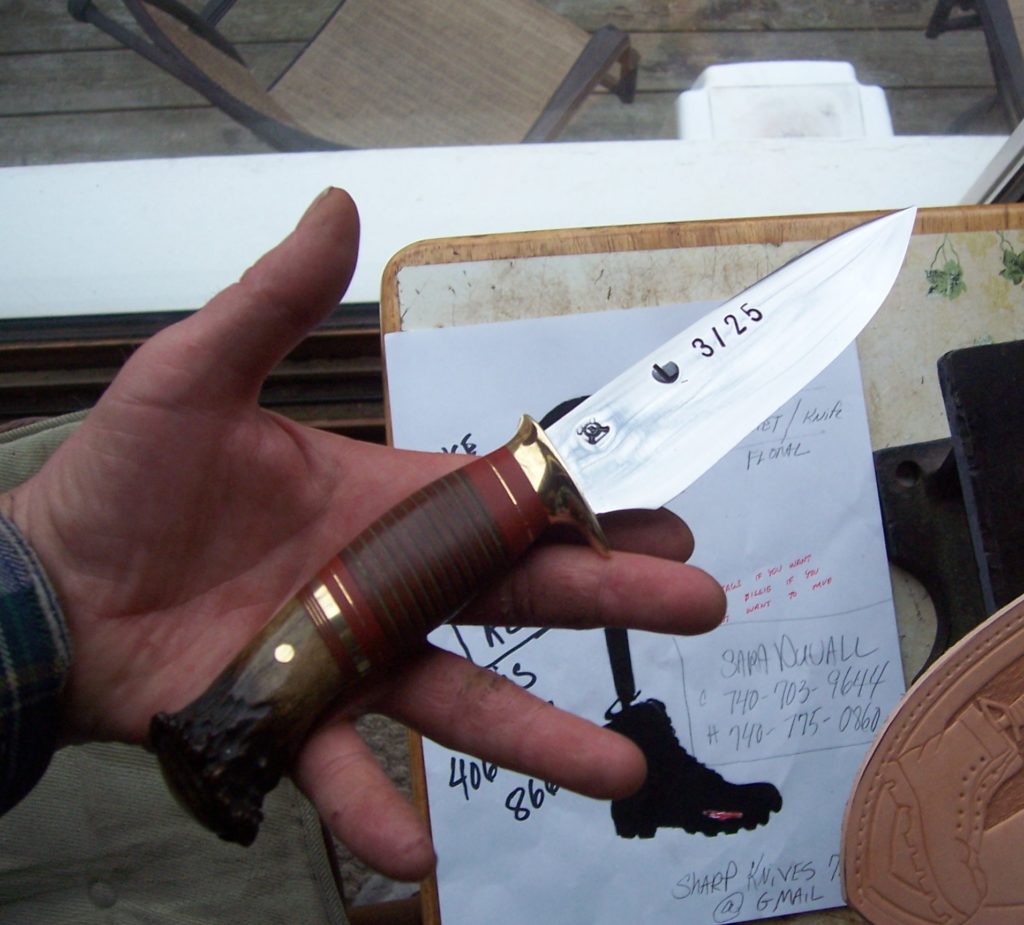
Travis set to work under the watchful eye and guidance of Behring. The finished knife includes a 6-inch drop point blade of O-1 tool steel, a thick brass guard, and a stacked-leather-washer handle with a butt of whitetail crown stag. Inserted between the leather washers is a piece of the nametape, typically worked across the top of the uniform pocket, of each of the 11 Marines killed on Aug. 3, 2005. The letter “L” for Lima Company and “3/25” for 3rd Battalion and 25th Marine Regiment are hot stamped into the blade.

Made by Travis under the watchful eye of Jim Behring, the knife has a 6-inch blade of O1 tool steel, brass guard, and a stacked-leather-washer handle with a butt of whitetail crown stag. Between the leather washers is a piece of the nametape, typically worked across the top of the uniform pocket, of each of the 11 Marines killed on Aug. 3, 2005. The letter “L” for Lima Company and “3/25” for 3rd Battalion and 25th Marine Regiment are hot stamped into the blade. (photo courtesy of Mudbone Jones)

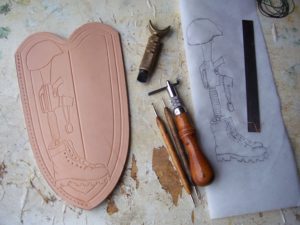
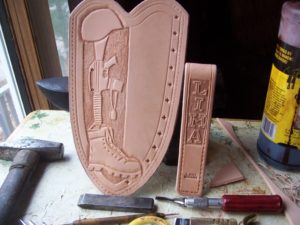
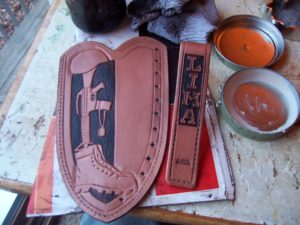
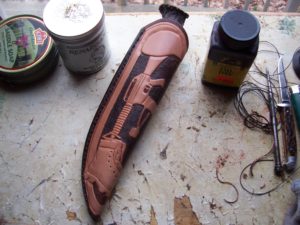
When the knife was complete, Mudbone set to work. With only a week to complete the task, he crafted a leather sheath with the iconic image of the rifle turned down into a boot and topped by a helmet. A dog tag hangs from the weapon. The word “LIMA” is also prominent.

“On the back of the sheath there are 11 four-pointed North Stars,” added Mudbone. “Craftsmen of earlier times stamped these on guns and knives so the owner could always find his way home. They finished the knife on a Saturday. I got it on Tuesday and dropped everything else to get the sheath done. Sometime around 3:30 or 4:30 a.m. the next Saturday, I pulled the last stitch and put the last wax on it.”

Above: Working from the drawing, Roger “Mudbone” Jones employed a Marine theme of helmet, weapon, dog tags and boots to make the knife’s leather sheath, including the Lima Company name. On the back of the sheath are 11 four-pointed North Stars,” added Mudbone. “Craftsmen of earlier times stamped these on guns and knives so the owner could always find his way home.” (photos courtesy of Mudbone Jones)

SOLD for $7,000

The knife sold for $7,000, but not during the silent auction. “Doc” Wentworth, a Navy corpsman who had been assigned to Lima Company, was determined to keep the Lima Knife with the portraits so beautifully painted by artist Anita Miller. The memorial event at the Ohio Statehouse in Columbus was moving and inspirational, and Wentworth succeeded through social media in raising small donations that bought the knife and will allow the memorial to remain together in its permanent home in the statehouse. An accompanying book, The Lima Company Memorial:  A Remembrance of Spirit and Choice, has also been produced.

UNBREAKABLE TIE

Learning the art of knifemaking and continuing to work with James Behring has proven therapeutic for Travis, and he is pleased with his opportunity at Behring Made Knives. While continuing to work in the shop, he attends events that help other veterans adjust to life after active duty. At some point in the future, he may begin making more knives and even taking orders. For now, he is content to continue learning.

“I like where I am with James’ company,” Williams said. “I do everything from heat treating to finishing blades and handles, and have recently gotten into making Kydex. On some of our CNC knives I’m doing the blasting, coating and sharpening of the blades. James is sitting there watching me, and someday I would like to get to the point where I am making knives on my own.”

Today, Travis finds contentment with his work and sees the future with optimism. There will, however, always be that unbreakable tie to his fellow Marines. Meanwhile, with a little help from his friends, he has created a lasting tribute to his fallen comrades.

Travis and his best friend, Lance Corporal Aaron H. Reed, take five. Reed was among those killed by the IED. His awards include the Purple Heart and Combat Action Ribbon. He was 21. (photo courtesy of Travis Williams)

For more information contact Roger “Mudbone” Jones, Dept. BL12, 320 Prussia Rd., Waverly, OH 45690 740-739-4562 [email protected], or Travis Williams, c/o James Behring, Dept. BL12, POB 17317, Missoula, MT 59808 406-926-1193 (shop) [email protected], www.behringmade.com.

IT’S ALIVE! The Living Knife by Jean-Marc Laroche will grab you—literally

“A knife capable of movement and gifted with intelligence …”
—Jean-Marc Laroche

“On fitting your hand into that of the knife, you already feel a strange clasping in response when, suddenly, the mechanical fingers close! You can’t get free! With the same movement, an eye opens and stares at you intensely. It’s awake! Now you are under its control, and the knife is master of you who dared to take it in your grasp.”

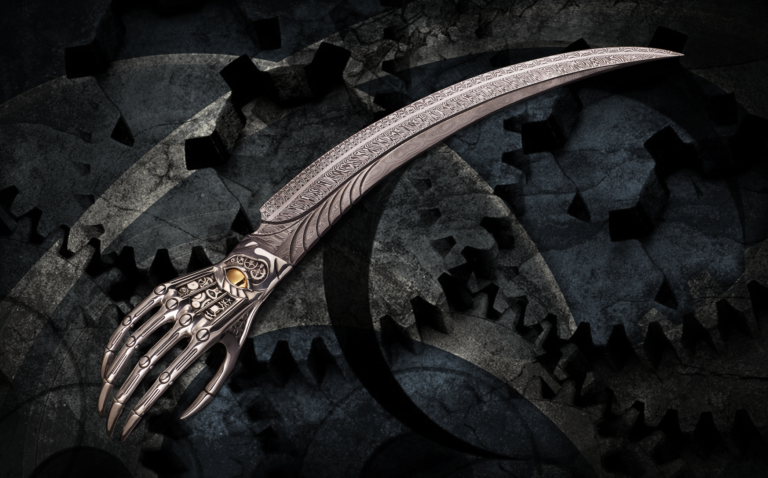
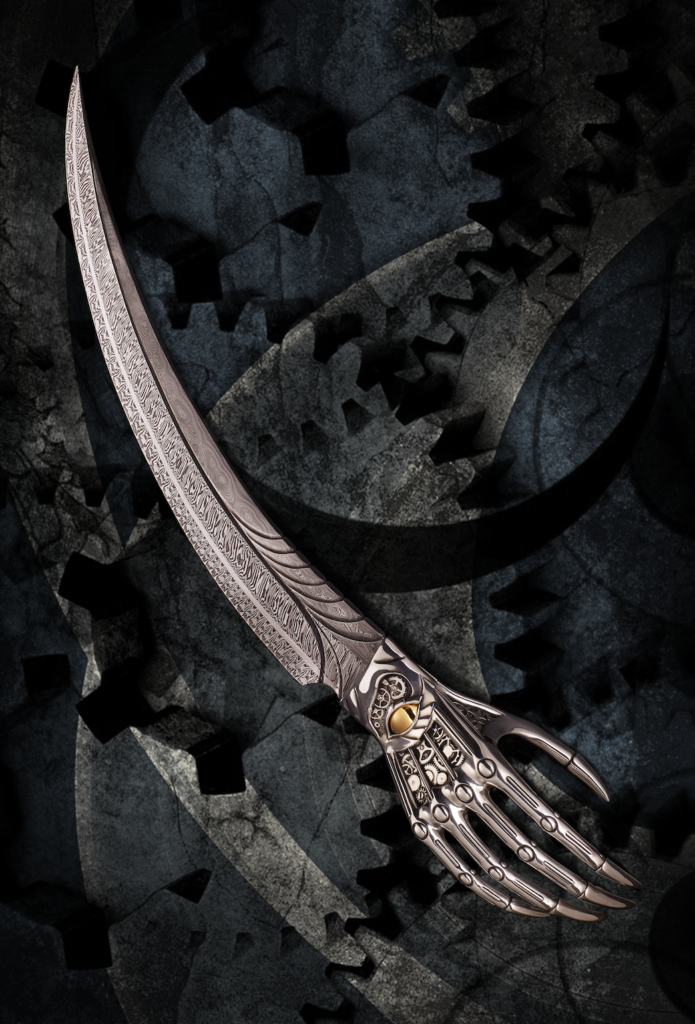
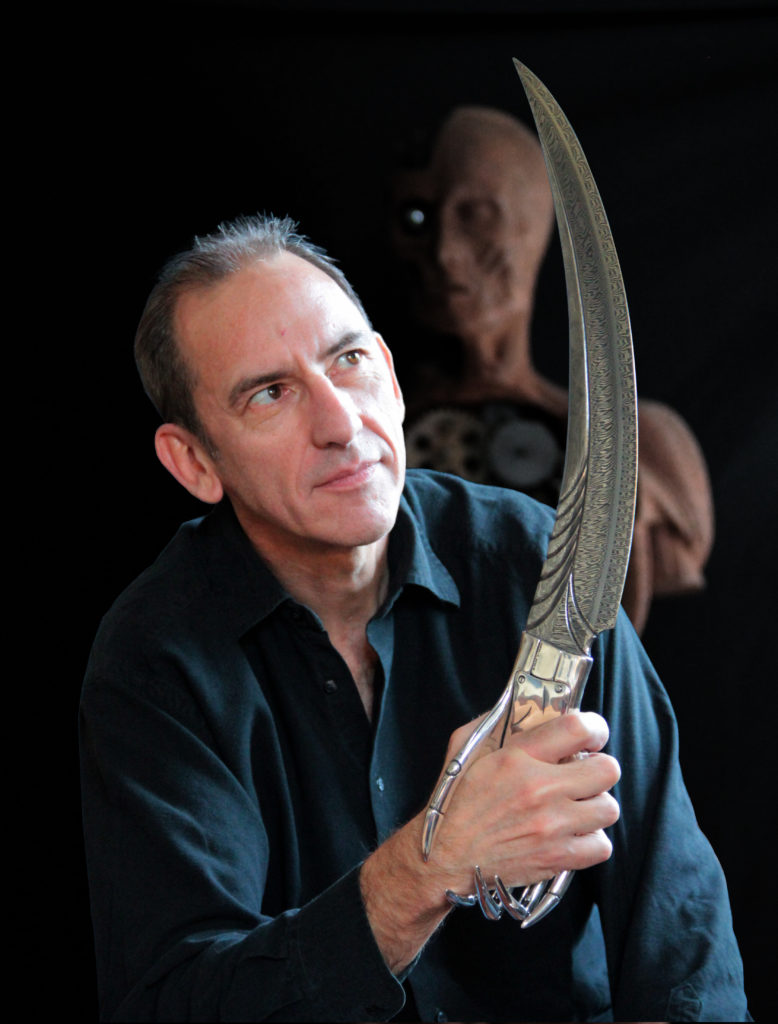
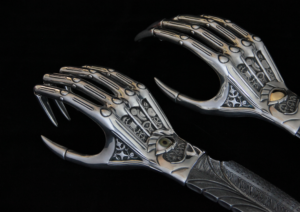
Above: The Living Knife by Jean-Marc Laroche features a mechanical hand for a handle that, as you grab it, literally grabs you back. The damascus blade is a composite of 15N20, 15LM and UHB11 high-alloy nickel and carbon steels in explosion, twist and random patterns forged by Swedish maker Roger Bergh. Overall length: 25 inches. (images courtesy of Jean-Marc Laroche)

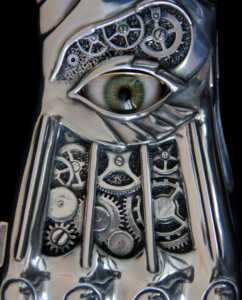
In addition to the above, French knifemaker/artist Jean-Marc Laroche refers to his latest creation—this issue’s cover piece—as “The Living Knife.” Since it has a “hand” for a handle with “fingers” that close, an “eye” and an overall lifelike appearance, who are we to argue? As you grab the handle, the “fingers” actually grab back so that it’s hard to tell who’s holding whom. And, as the fingers grab your hand, the “eye” opens. The hand also is embellished with gears in the Steampunk style.

A close-up of the silver-plated bronze hand shows the detail of the gears in a Steampunk motif. (image courtesy of Jean-Marc Laroche)
The opening eye.

The Living Knife is indeed a most unusual creation—but then Laroche has been making otherworldly pieces for over two decades. Even by his standards, though, this one takes his knife art into uncharted territory.

“It was from the cinema of fantasy films that I drew my inspiration,” he notes. “It took me 12 years to implement my idea, six months to carry it out and a fair number of technical difficulties had to be overcome.

“Yet here it is, like a cunning thing from another time that a mad inventor out of the 19th century would have dreamed up. This biomechanical being activates its workings to move its fingers; it seizes control of the situation with its eye’s intelligence.”

The Living Knife is an assembly of mechanical parts, the prototype having been made in resin. A few rare versions in bronze, gold and silver are in the process of being forged.

“Swedish knifemaker Roger Bergh participated in this project. Indeed, I have been talking to Roger about it for 10 years and he has always been enthusiastic,” Laroche observes. “Roger first forges damascus steel to obtain various types of structures; he then assembles them into magnificent combinations. A world-renowned knifemaker, he has remained down-to-earth and open. Working with him is a real pleasure.”


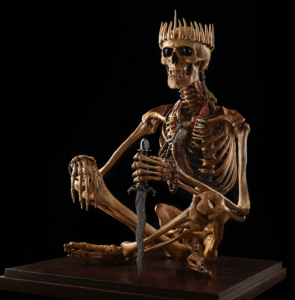
In addition to knives, Jean-Marc Laroche sculpts skeletons on a lifelike scale. An example is his “Warlord,” a kind of Javanese king holding a kris.
The skeleton is resin on a steel structure. The crown is assorted animal bones, the eyes are natural quartz crystal, and the necklaces and bracelets are from “different ethnic tribes.” The knife is made from an old Indonesian kris blade, some teeth and hematite.

KNIFE SPECTACULAR

BLADE® first learned of Laroche at the 1992 East Coast Custom Knife Show, where his knives with “alien-head” handles were a show hit. The alien heads were those of animals he customized and coated with a special resin.

In 1997 Laroche’s “Mother Ship with Fighters”—a set of four knives including one large one and three smaller ones with dagger blades and curved, claw-like guards—was a winner of the annual BLADEhandmade Best In Show Award. His “Byakhee,” a spectacular knife with a handle resembling a large, bat-like bird inspired by the science-fiction stories of H.P. Lovecraft, won Best Fantasy Knife at the 1998 BLADE Show West.

Laroche introduced The Living Knife to an appreciative audience this past June at the FICX, an invitation-only knife show in Paris that also featured a few U.S. makers, including Kevin Casey. It was Jean-Marc’s first knife show since 2002. Since then he had been involved in other forms of sculpture and exhibiting them worldwide.

Actually, The Living Knife is not Laroche’s first attempt at such a piece, his “Devil Hand” predating it. However, the Devil Hand did not have the mechanical grasping capability, the same materials or other select features of Laroche’s newest rendition. Laroche said he also has made two knives similar to The Living Knife, the first being sold to the Instituto Ricardo Brennand (http://www.institutoricardobrennand.org.br/index2.html), a museum in Recife, Brazil.                   

For a video on how The Living Knife operates, watch the video below:

The Best Blade Grinds: What To Look For

0

As with most things knife, one type never fits all.

BY MIKE HASKEW BLADE® FIELD EDITOR

Finding the best blade grind for the job at hand has become the subject of some debate, but most knife users agree that certain grinds are better suited for certain functions. Combinations of steel, knife design and use influence the choice of grind.

“I’m a proponent of the right grind for the right job,” related author/knifemaker Abe Elias. “In small bushcraft knives, a thin, flat grind and a saber grind are hard to beat. It makes sense that clear cuts are best flat edged. Carving chisels have rounded convex edges to go into wood and take small cuts and come out.”

An inappropriate grind may produce drag, a ragged or erratic cut, and generally poor results. “For overall working of wood and good, straight, controlled cuts, you want a knife grind to ride flat against the surface so it cuts past certain levels and growth lines, riding flat on the wood between growth lines,” Elias added. “It’s just physics. That’s all, and nobody can really argue it.”

One of the most popular grinds for bushcraft knives is the scandi grind, and Elias describes it as a perfectly flat grind with no secondary bevel, starting at the shoulder with an angle that is perfectly flat and straight to zero.

One of the most popular grinds for bushcraft knives is the scandi grind. Abe Elias describes it as a perfectly flat grind with no secondary bevel, starting at the shoulder with an angle that is perfectly flat and straight to zero. He used it on the blade of his Woodcrafter model. (Abe Elias image)

“Scandi grinds will go on any steel you want, but there are limitations to them because of the shoulder,” he noted. “It doesn’t tend to go through soft surfaces well, such as processing meat. When the knife enters a malleable surface, it creates too much drag on the blade. Like anything else, the thinner it is the easier it enters into other masses. We run into problems when custom makers make them and factories produce them without following the golden rule of proportion. The angle should be proportional to the thickness of the steel and the design of the knife itself.”

CONVEX MODIFIED

Influenced heavily by BLADE Magazine Cutlery Hall-Of-Fame® member Bill Moran, Bill Bagwell, and Don Hastings, ABS master smith Jim Crowell recognized early in his knifemaking career that the intent was to make a full convex grind from the spine of the blade to the cutting edge. He has adapted those original lessons through the years.

“I’ve found that it’s the edge that needs to be convex, not necessarily the whole cross section of the blade,” Jim noted. “Consequently, I have now, for many years, ground my blades flat from spine to cutting edge, stopping short of going to zero and then rolling the cutting edge on convexly. The trick is to get the geometry correct for the thickness the edge was ground to prior to sharpening in conjunction with the type and heat treat of the steel used.”

Crowell says he believes the convex grind is best for knives in the field, including bowies, fighters, and fillet knives. He uses the convex grind almost exclusively and indicates it allows for an uninterrupted transition from the cutting edge to the full thickness of the spine of the knife. No matter how thick or thin the spine of the knife, with convex geometry it will have the least amount of resistance when cutting through an object.

ABS master smith Jim Crowell has ground his blades in a modification of the convex style for many years, grinding them flat from the spine to the edge, stopping just short of a 0-degree angle, and then rolling the edge in a convex shape. His 15.5-inch bowie features W2 tool steel and walrus ivory. (Chuck Ward knife image)

As for sharpness, Jim gives the nod to the scandi grind. However, he believes that when the cutting edge is, in fact, the grind line as well, the edge itself is more fragile in comparison to other grinds.

“Scandi grinds are great,” he said, “and useful for a lot of small chores. Then there are special-purpose applications like some sushi knives that have specialized grinds. Still, for day in and day out I like and recommend the flat, convex grind.”

COMFORT MATTERS

Knifemakers tend to use the grinds they are comfortable with and which they believe fill the bill for the types of knives they make. The degree of difficulty associated with a particular grind lies more in the experience of the maker than in the grind itself.

“The hardest grind is the one you do not regularly do, and the easiest would be the one you do all the time,” Crowell reasoned. “When I started, I used to hollow grind stock removal blades. You could lay everything out and follow the lines—it is still hard though. When I started forging it was really hard because there were no layout lines to follow, and all the scale and hammer marks made it hard to tell what I was doing. Daggers are generally acknowledged to be more difficult. Some of the Russian and Persian stuff with a ‘T’ spine or center ridge would be tough.”

According to Jim Crowell, the dagger blade pattern generally is acknowledged to be more difficult to grind than most. Michael Jankowsky ground the blade to a double edge on his “Thor” model in Elmax steel and Siberian jade inlay. The engraving is by Kati Mau.(Francesco Pachi image)

“The hardest grind is the one you do not regularly do, and the easiest would be the one you do all the time.”—Jim Crowell

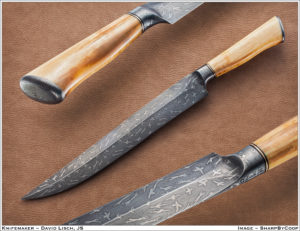
ABS journeyman smith David Lisch—shown grinding the blade of a custom collaboration knife to raise money for the African Wildlife Foundation in its fight to protect elephants from poachers—applied a Persian grind to his 16-inch integral fighter in Thunderbird damascus and walrus ivory. (SharpByCoop.com knife image; image of Lisch courtesy of Mark Knapp)

FACTORY APPROACH

Knife manufacturers gear their grinds for prospective use as well. Hollow grinds are usually the most efficient for manufacturing because both sides of the blade are ground at the same time. Flat grinds are ground one side at a time, and precise machining and good tooling create the even grinds for which manufacturers are known. Convex grinds are usually finished by hand, and such work is the province of a skilled custom maker.

“Hollow grinds are great for slicing,” commented Jim MacNair, new product coordinator and senior designer at KAI-USA Kershaw, “and they create a nice, thin edge geometry, and the panel of the grind stays thinner as you sharpen away the blade over time. These blades will feel very sharp because the grind scoops away more material and makes the blade thinner overall.

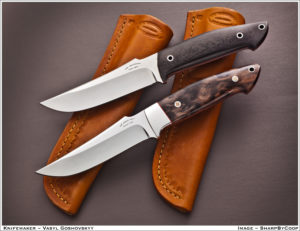
The hollow grind is great for slicing and feels very sharp because it scoops away more material and makes the blade thinner overall. Vasyl Goshovsky employs a hollow grind on his working knife’s 4.5-inch blade of N690Co stainless steel. (SharpByCoop.com image)

“The most obvious benefit of the flat grind is strength and toughness. The wheel is grinding a flat surface rather than a concave one like a hollow grind, and it removes less material from the blade. That added material makes the blade thicker and stronger.”

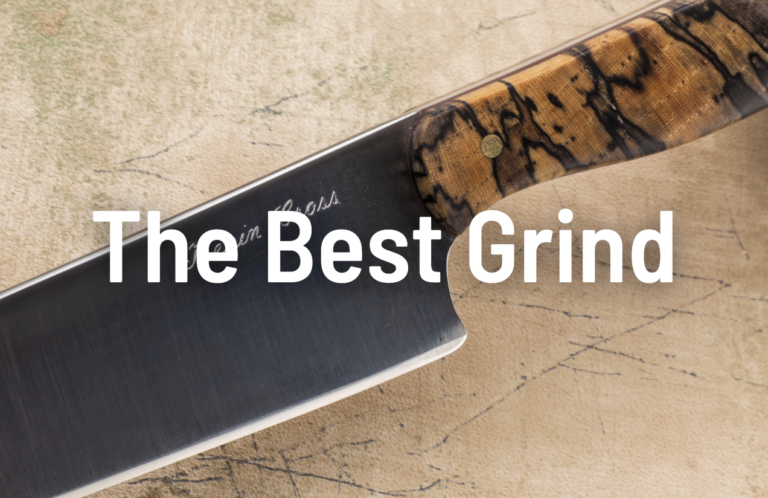
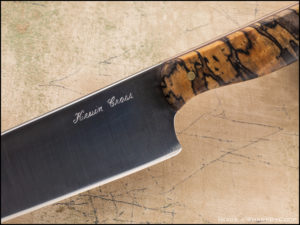
The most obvious benefit of the flat grind is strength and toughness, according to Jim MacNair. Kevin Cross flat ground the 52100 blade of his kitchen knife. The handle is spalted hickory. (SharpByCoop.com images)

MacNair sees compound grinds emerging in the custom market, including blades that feature a combination of flat- and hollow-ground bevels. These are often done to create a “cool” look, and the maker is also providing the best of both cutting options: a thin, hollow-ground edge for slicing and a thick, flat-ground tip for toughness.

Innovation continues to find its way into new and user-friendly blade grinds, while the emphasis on the job to be done is at the center of the decision. Putting the proper edge on the blade for cutting, slicing, skinning, chopping or any other task will always be primary.

SWORD GRINDS HOSTETTER’s WAY

Swordsmith Wally Hostetter focuses on Japanese blades and tailors the grind of each to its anticipated function. He forges the blades and sets up the edge geometry with hand filing.

“A lot of guys do hollow or flat grinds with a machine, but what I do has to be done by hand,” Wally explained. “I hand polish to the cutting edge, and there is no micro-bevel. Some have an appleseed [convex] edge—niku is the Japanese term—and some have the edge slightly rolled in for better cutting. For cutting heavy stuff, the niku comes to a finite edge but runs farther up the blade. There are many subtleties to it.”

According to Hostetter, other Japanese grinds, such as that found on the tanto, are fine and done to a thin edge because they are not intended for hard striking against surfaces. He uses 1095 carbon steel primarily and decides on the appropriate grind based on both the use of the blade and the historical time period that is being replicated.

Advertisement

Must Read Articles

Read this before you make a knife

Knifemaking 101 – Read This Before You Make a Knife

  by Wayne Goddard My experience has taught me that there's nothing like digging in and getting started. I've often said the hardest part of the...
how to forge damascus steel

How to Forge Damascus

Advertisement
Advertisement