Knifemaking

Knifemaking is the building of a knife, which includes the blade, handle and other accouterments. Blades are made by either removing metal from a steel blank via a grinder – known as stock removal – and the forging to shape of hot steel into a blade in the process known as bladesmithing. Other parts, including bolsters, guards, pommels, etc., are needed to complete the finished knife.

Featured Knives – – Knife Collecting – – Tactical Knives – – Survival Knives

Custom Flipper-Folders: Art Of The Flip

Aesthetically and mechanically challenging flipper designs that shine.

The flipper folder is one of those knife designs that continues to delight its makers and its owners with incredible vitality. Not only do the most recent flipper folders fill the traditional bill with great materials, mechanics and mesmerizing beauty, but they further garner high praise with an inherent level of energy.

Combining the attributes of excellence that set standards for custom knives with the sheer pleasure of smooth operation, the latest flipper folders hit the mark in quality and bring attention to their makers amid an ever-growing level of interest in the marketplace.

Scott Gallagher: Feather Damascus
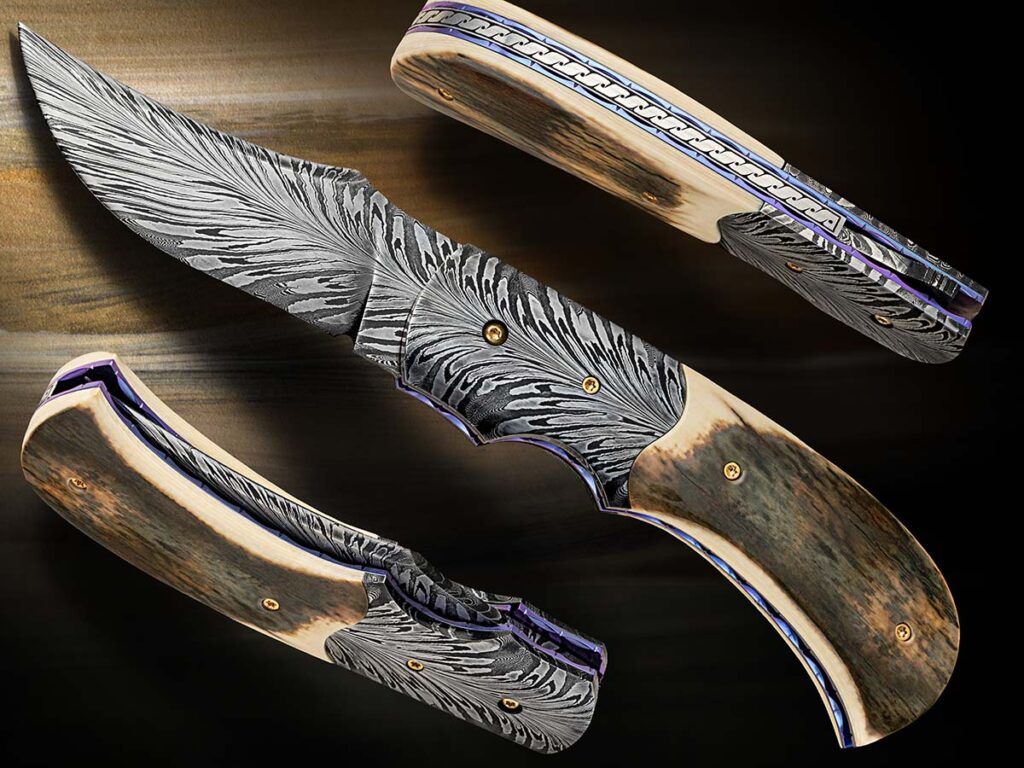
Scott Gallagher says he’s seen an upswing in the interest in flippers in recent years. It makes sense with works like his feather damascus flipper. The feather pattern defines both blade and bolster, and is complemented by a fossilized mammoth ivory handle. (Jocelyn Frasier image)

Scott Gallagher recently completed a beauty with a 3-inch feather damascus flat-ground blade complemented by a damascus bolster and fossil mammoth ivory handle. With an overall length of 7¼ inches, Scott’s flipper folder features an upswept curve for fantastic visuals and intricate filework along the spine.

“I am receiving more requests for flippers right now,” commented Scott. “They have become very popular. I think the reason why is because they’re fun to use, kind of like a widget—they’re functional, they can be embellished and they are easy to carry.”

The single attribute of fun helps set the flipper folder apart from other designs. Anything incorporating fun into the knife equation is sure to gain increased attention. Still, Scott makes his flipper folders with exacting specifications and attention to detail. “A quality flipper should have a blade steel that performs well—good fit, finish and symmetry,” he explained. “The blade should close in the center of the frame. It should be fast opening and close easily without a sticky lock.”

For Scott, achieving the proper mechanics involves a combination of precise construction with materials that work in concert with each other. “Making the flipper tab is a matter of incorporating it into the design of the knife in the design phase,” he related. “In the closed position, the tab has to sit higher than the frame so your index finger can access it. I use bearings on my flippers. They are ceramic and very fast. To avoid pinching the user’s hand, I use a small tab. It’s only exposed enough to open the blade. My flipper tab is hidden in the frame in the open position. I have finger grooves designed into the frame to avoid fingers slipping forward.”

Alan Hollerbach: Spectre
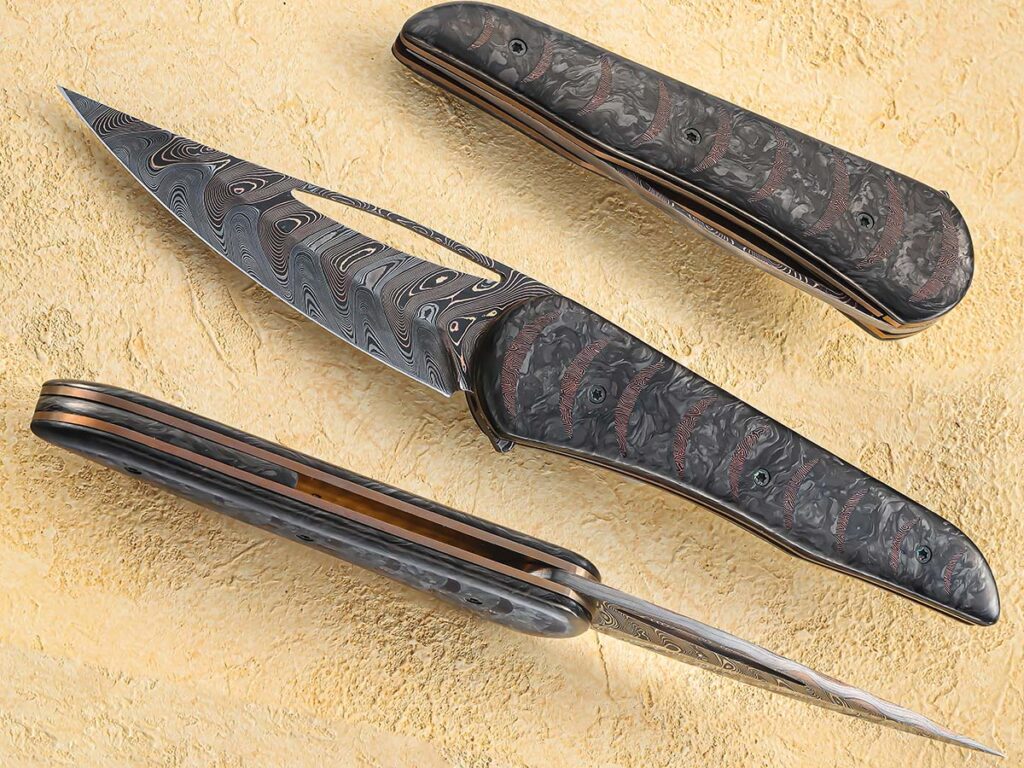
There’s something ominously attractive about what Alan Hollerbach achieves with this knife. Christened the Spectre—an homage to the nemesis organization of James Bond—the wasp-wasted flipper gets right to the point. Baker Forge TigerMai steel for the blade and Fatcarbon Dark Matter scales add to the knife’s dark good looks. (SharpByCoop image)

When customers consult with Alan Hollerbach on the attributes of a quality flipper folder, his response is straightforward. “Look for high-quality materials—hardened washers and bearings, a smooth action and a solid detent,” he offered. “I don’t take orders. I make knives I like and hope others do as well.”

The degree of knifemaker proficiency is tested somewhat further with the flipper folder in comparison to other designs. Alan welcomes the opportunity to put his skillset to the test. “It takes some more designing up front to get the layout and how it looks and the action correct,” he related. “The tab needs to be in a comfortable position for one-handed opening, tall enough to engage easily, but not too tall it looks out of place. It needs to have a strong detent to allow proper pressure to fire the blade and a smooth action with the bearings to allow the blade to open with minimum friction.”

Alan achieves his technical and aesthetic objectives in a handsome flipper folder model he has christened the Spectre, in reference to the James Bond feature film series. This example includes a 4-inch hollow ground blade of Baker Forge TigerMai Chevron damascus steel with jeweled and anodized titanium liners and Skiff bearings with hardened washers. Handle scales are Fatcarbon Dark Matter with 18 inlays in nine different sizes of Space Coral. The backspacer is also Fatcarbon Dark Matter, and the screws are black anodized titanium.

Rising interest in flipper folders is a matter of likes and style, as Alan sees the buying landscape these days. “I think it is a personal preference,” he commented. “I like the flippers for easy one-handed opening, but you can do the same with most other ways. It takes some more designing up front to get the layout and how it looks with the correct action. I like the lines as clean as I can make them, so tabs are just to open the knife, as I try to hide as much as I can when the knife is open, just for aesthetics.”

The addition of a hole in the Spectre blade gets attention as well. “You can open the knife with the hole, but it was designed for aesthetics mainly,” Alan noted. “I wanted to smooth the lines of the knife in the closed position and show with the curves of the cutout it was done on a pantograph by hand.”

Robert Champion: Dark Wind
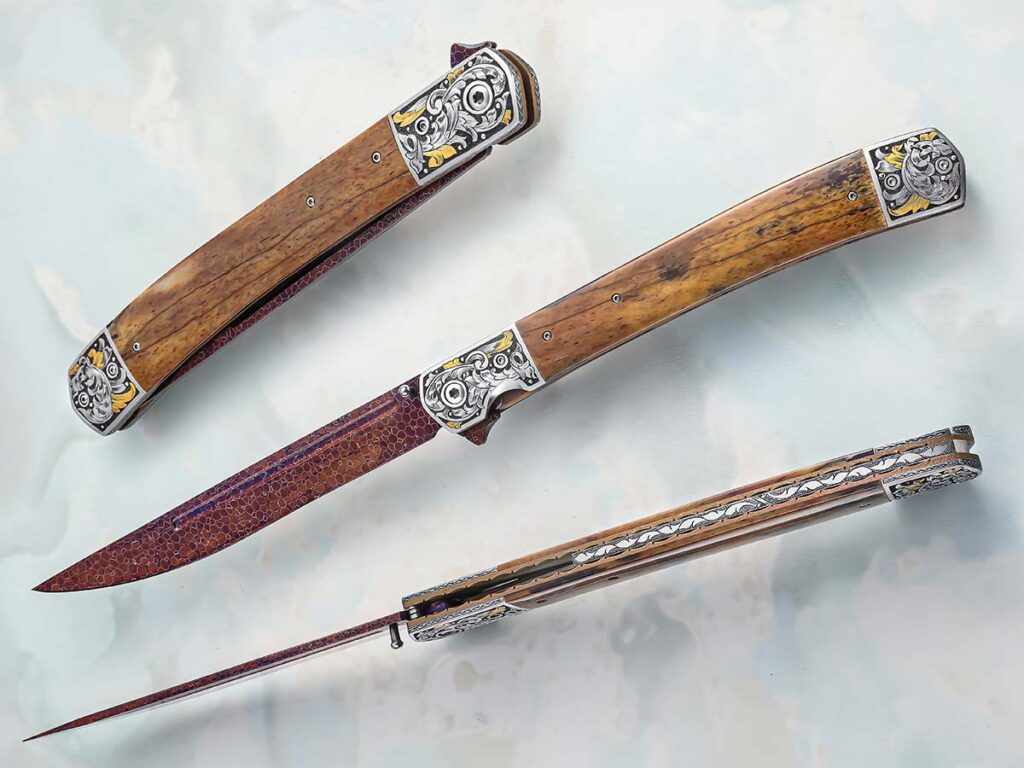
Robert Champion spends plenty of time perfecting the placement of the deployment tab. On his Dark Wind, he employs a low-profile tab to avoid pinching when the blade is deployed. Also noteworthy on this knife, the knock-out engraving by Dale Bass that takes the work to another level. (SharpByCoop image)

Examining the locking mechanism is a must for those contemplating an investment in a quality flipper folder, a tip Robert Champion emphasizes. “A 3-point constraint is better than a 2-point constraint,” he said. “A 3-point will lock the knife more securely in the open position as well as in the closed position. The blade should lock solid, not be loose and never have a sticky lock.”

Robert’s Dark Wind model exemplifies his perspective on the flipper folder. Its 6-inch blade features hollow ground Dragonskin Damascus steel from Shaya Forge, while the furniture is in 416 stainless steel and the handle scales are fashioned from giraffe bone. Dale Bass’ engraving complements the piece in its entirety.

“I’m receiving more and more requests for flippers,” Robert remarked, “especially the more dressed and upscale models. Their popularity seems to be trending up. They’re easier to deploy and in regions where automatics are not permitted, the flipper is a great option. The flipper tab is an integral part of the tang design that is easily roughed in while profiling the blade. Thumb pegs and discs are separately fabricated components that require drilling, tapping and a turning process on a lathe. Then, they are attached to the blade. Tab location is important when designing a flipper. Placing it too far forward or too far back on the tang will cause inefficient deployment.”

Bringing all these components together in proper tolerance with respect to the look and feel of the finished product provides a worthy test for the makers of flipper folders. Like any folder, smooth deployment and ease of carry rise to the top. However, the flipper aspect brings another dimension to the requirements for optimal performance.

“Depending on the size of the knife, I use good-quality stainless or ceramic ball bearings,” Robert advised. “I tend to use stainless bearings on my smaller models, but that is just a personal preference. I also use dry slide oil lubricant. I design a low-profile tab to prevent pinching and currently make single-tab models. In the future, I plan to make flipper daggers that will have more of a guard-type tab.”

John Curran: Alpha 3
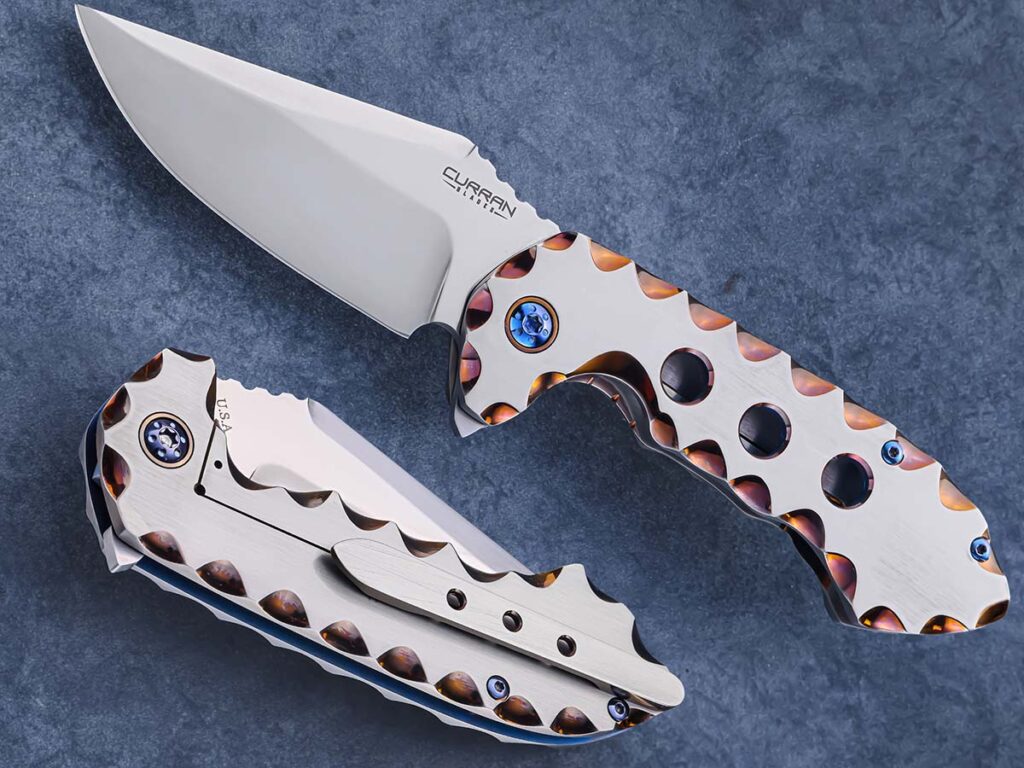
John Curran has focused much of his work on flipper folders and his experience in this design shows in his Alpha 3. Clean and complex, the knife pairs a titanium handle with an Elmax steel blade, featuring caged bearings for absolute, buttery-smooth deployment. (SharpByCoop image)

John Curran created a flipper folder in a model he calls Alpha 3 with a flat ground 3-inch blade of Elmax steel and an overall length of 7½ inches with a titanium handle and frame. The flipper design has been a mainstay of his work for some time.

“I’ve predominantly built flipper-style folders over the years, though I’ve done my share of thumb-stud and thumb-hole deployments as well,” he related. “In terms of trends, I haven’t noticed interest in one style rising or falling dramatically. What I have noticed is that customers are spending more carefully. People know what they want and they are choosing their purchases very intentionally.”

As John tries to fulfill his customers’ expectations, he watches the intricacies of the flipper folders he constructs carefully. “From my perspective, flippers don’t necessarily hold an advantage over other deployment methods,” he commented. “It really comes down to personal preference. Some customers want a classic flipper, others ask for a flipper paired with a thumb stud and some want a hole cut into the blade as an alternative opening method. There is no single best option, just what feels right in the user’s hand.

“The complexity of the build depends on the design more than the deployment style,” John continued. “I spend a lot of time sketching concepts only to discover during mock-ups certain ideas don’t translate well in hand. I typically prototype in G-10 or even wood to check ergonomics, mechanics and overall fit. That stage tells me a lot about whether the knife is going to meet my standards.”

John’s basic components include caged bearings and hardened stainless washers for smooth action. “If a customer wants to keep the cost down, I can build the knife without bearings and use phosphor bronze washers instead,” he advised. “Ceramic bearings undeniably offer the smoothest action, but bronze washers still perform well. It ultimately depends on what the customer values most. Milling pockets for the bearings adds time and labor and is reflected in the final price.”

Design concentrations on clean, reliable opening mechanisms and functional finger guards when the blade is deployed are hallmarks of John’s finished product. The challenge is always in the “tweaking” to solidify the geometry, but the result is worth the investment of time and effort.

The flipper folders emerging in the custom knife market today offer diverse profiles, materials and interpretations along with a wide range of price points. Each of these factors influences the consumer and makes the genre vibrant.

More On Flippers:

Bark River Knives Shuts Down Amid Steel Controversy

Bark River Knives owner Mike Stewart took to Facebook to admit to closure and the use of Chinese steel in Made-in-U.S.A. labeled knives.

Bark River Knives of Escanaba, Mich., has officially ceased operations following a public admission by owner Mike Stewart that the company utilized Chinese steel in blades marketed as American-made CPM 154. The announcement, made via Facebook on March 23, confirmed that the long-standing fixed-blade manufacturer concluded all business as of March 20.

In his statement, Stewart took full responsibility for the deceptive labeling, characterizing the use of imported steel as a measure intended to keep the company afloat. Stewart argued the alternative steel met his internal testing for toughness and stain resistance, with edge retention nearly matching that of Crucible Industries’ CPM 154. He further claimed that because the knife blanks underwent more than five distinct operations in the Michigan shop—including grinding, reshaping and etching—they technically met his interpretation of “Made in the U.S.A.” criteria.

It should be noted, the Federal Trade Commission (FTC) standards mandate a product must consist of “all or virtually all” domestic components to carry the label. Stewart admitted the steel was definitely mis-marked on the following models:

  • Camp Bolo
  • Fox River Trailing Point
  • Highwayman 4
  • Mini-Manitou
  • Gladstone Hunter
  • Bitterroot Caper
  • Select recent Club Knives

The closure follows a period of increasing pressure from collectors and dealers, alongside significant financial litigation, Outdoorlife.com reported. Stewart noted in his post that the shutdown was “long overdue” and should have occurred two years prior.

Stewart announced that his son, Jim Stewart, will open a new, 100 percent independent knife company. Notably, Jim Stewart has agreed to take over the warranties that would have normally been serviced by Bark River. Mike Stewart clarified that he will have no hand in the new entity and intends to exit the industry entirely after 50 years. Mike Stewart emphasized that his dealers, his wife Lesley and Jim Stewart were entirely blameless in the decision to substitute the blade steel.

More On Knife Steel:

MagnaMax and Pop’s ProCut: The Next Super Steels?

Specially engineered for knife blades, the two alloys are at the cutting edge of metallurgy.

Editor’s note: The genius behind MagnaCut—arguably today’s most popular blade steel for both custom and factory knives—the author has helped create two new blade materials that he fully expects to meet with wide-ranging acceptance as well. Following is his story on his latest voyage into his favorite subject.

I pitched the idea of MagnaCut steel to Crucible Steel and Niagara Specialty Metals in 2019. I said I had an idea for a steel that would match the best of the non-stainless powder-metallurgy steels in terms of wear resistance and toughness. This would be a big deal because there has been a longstanding gulf between the performance of carbon steels and stainless steels. My team and I successfully turned the idea into MagnaCut, released in 2021, which had a microstructure like a non-stainless steel while being stainless—offering the best properties of both.

I intentionally sought balanced properties with MagnaCut so it was both tough and wear-resistant, similar to non-stainless grades such as CPM 4V, CPM CruWear and Vanadis 4 Extra. Knife enthusiasts, especially those into folders, often seek higher-wear-resistance steels for maximum edge retention. Instead, I tried to push for a more balanced set of properties so knife buyers could see the benefits of having high toughness in addition to good wear resistance. This can allow knives to be made with thinner edges for better cutting ability, because toughness helps thinner edges resist chipping. In my edge retention tests with the CATRA (Cutlery Allied Trades Research Association) edge testing machine, thinner edges with smaller angles lead to larger differences in edge retention than the steel choice, or even the heat treatment! It seems many knife buyers have seen the light as MagnaCut has gained quite a bit of popularity since its release.

MagnaMax Steel

Nonetheless, I also knew knife enthusiasts would ask for something more wear-resistant. The folder crowd is not as worried about toughness and are seemingly always asking for greater wear resistance and edge retention. However, when the wear resistance gets too high, the steel becomes “unbalanced,” and the toughness becomes a significant issue. I see images of broken folders semi-regularly from the most extreme wear-resistance grades.

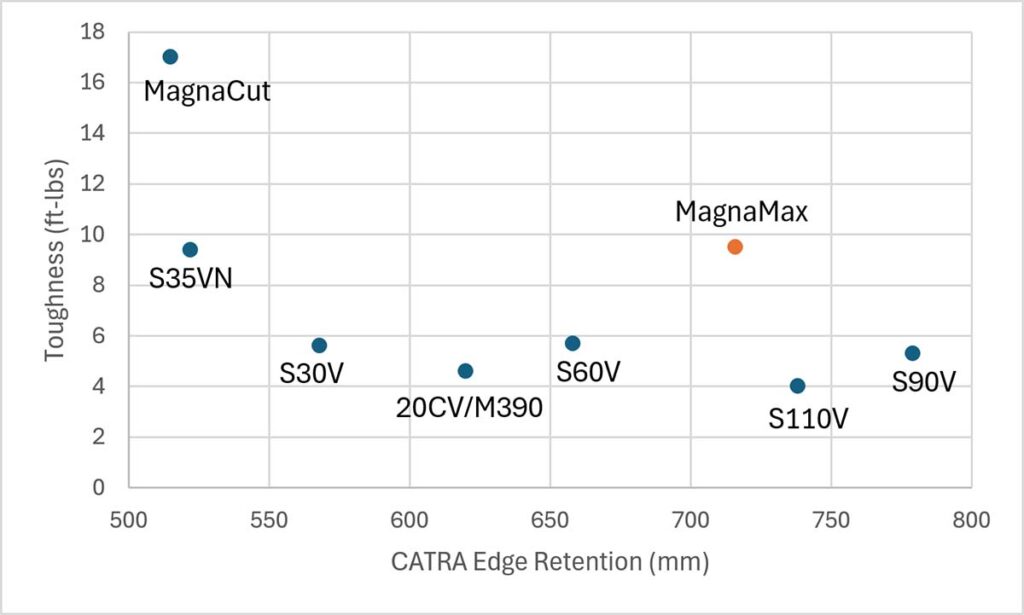
MagnaMax shares the same high corrosion resistance and good hardness potential as MagnaCut, but has higher wear resistance at the cost of some toughness. Because MagnaMax shares a similar microstructure to non-stainless steels, its toughness level for that high wear resistance is excellent.

The “sweet spot” for higher-wear-resistance products seems to be in the family of non-stainless alloys such as CPM 10V, Vanadis 8 and K390. In particular, K390 has been building in popularity through Spyderco knives in recent years for its excellent combination of properties. I had actually proposed to Crucible and Niagara way back in 2019 that, after we were successful with MagnaCut, I had another idea I was calling stainless 10V at the time.

This led to a new product called MagnaMax, a higher-wear-resistance steel in the same family as MagnaCut. It shares the same high corrosion resistance and good hardness potential as MagnaCut, but has higher wear resistance at the cost of some toughness. Because it shares a similar microstructure to non-stainless steels, its toughness level for that high wear resistance is excellent.

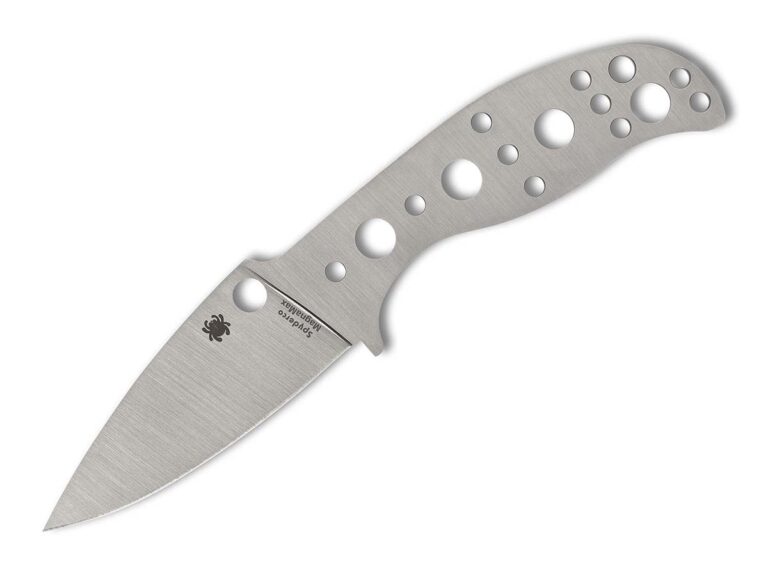
Two of the highest-toughness stainless powder-metallurgy steels before MagnaCut were CPM S35VN and CPM 154. MagnaMax matches the toughness of those grades while being much more wear-resistant. In recent years, one of the more popular folding knife steels has been M390, and MagnaMax has over twice the toughness and substantially higher slicing edge retention. Spyderco used the second prototype heat of MagnaMax in a series of its Mule series knives intended for enthusiasts to try out different steels. A Spyderco Forum member known as vivi said he cut 325 gallons worth of cardboard strips with one of these knives. He reported, “Even without adding the numbers up, I can say this steel has the best edge retention of any steel I’ve tried.”

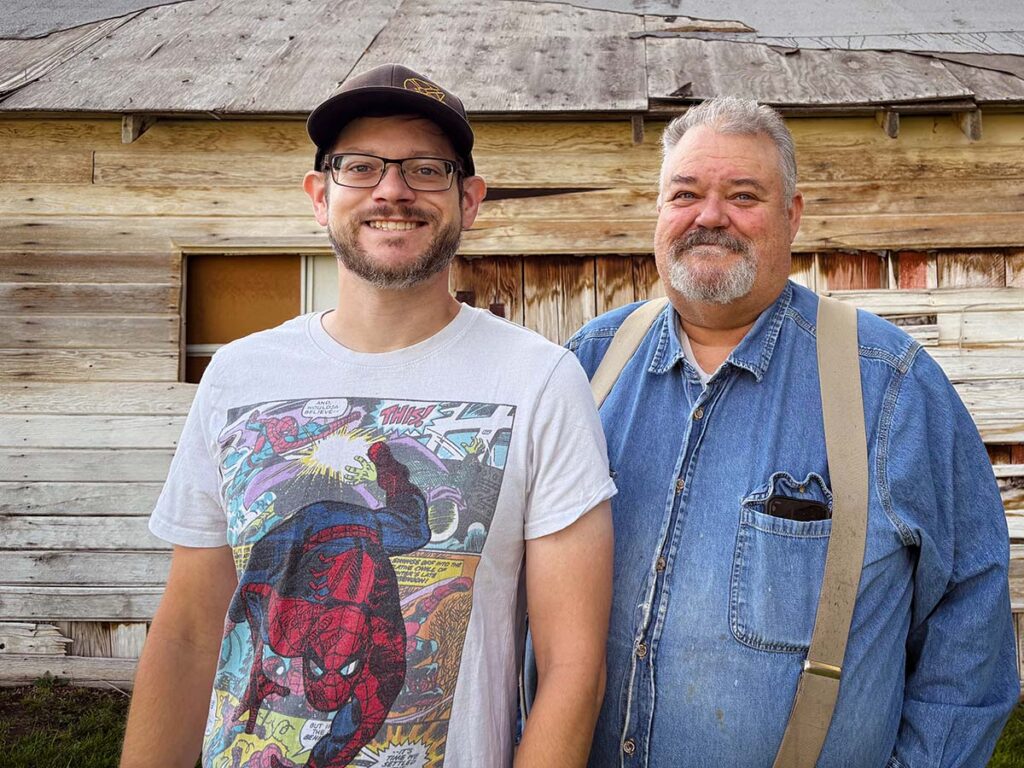
The author (left) and his father, BLADE Magazine Cutlery Hall-of-Fame® member Devin “Hoss” Thomas.

The development of MagnaMax was not without its issues, however. The first two test heats of the steel were made by Crucible, a longstanding U.S.-based steel company that unfortunately went out of business in 2025. Crucible is the company behind many of the industry’s leading knife steels like 154CM, S30V, S35VN and 3V. Crucible is the company that invented powder metallurgy itself, a significant innovation providing the excellent properties of all the “CPM” (Crucible Particle Metallurgy) grades. Crucible went under basically right while it was making the second test heat of MagnaMax. A couple of slabs were even recovered from a pile of scrap after the company was dismantled so my team could test it. We made the first test heat of MagnaMax back in March 2023, and we are just now approaching the product’s wide release.

Niagara Specialty Metals (NSM), the company that hot rolls, anneals and distributes the majority of the leading steel grades, has played a key role in keeping these steels alive. Crucible relied on NSM for hot rolling the high-end, complex grades, as it is the only facility in the United States capable of processing them.

Niagara had already assumed an active role in the knife industry many years before, taking over the distribution of blade steels over a decade ago after Crucible’s first bankruptcy in 2009. It pushed for new grades like CPM S45VN, and without NSM, I’m not sure MagnaCut would ever have been made. Niagara is working with other suppliers of powder-metallurgy steel, including Carpenter and Erasteel, to ensure these grades remain available. My team has been working closely with these partners on the development of MagnaMax, but that also means we almost had to start over after Crucible’s unfortunate demise. The good news is I have been testing MagnaMax made by Erasteel, and the properties look excellent, at least as good as the Crucible-made material. And it’s actually looking a little better.

Pop’s ProCut Steel

Perhaps sometimes I get carried away working on new knife steels that push the boundaries for wear resistance. Some knifemakers are looking for simpler grades that are easy to forge, grind and finish.

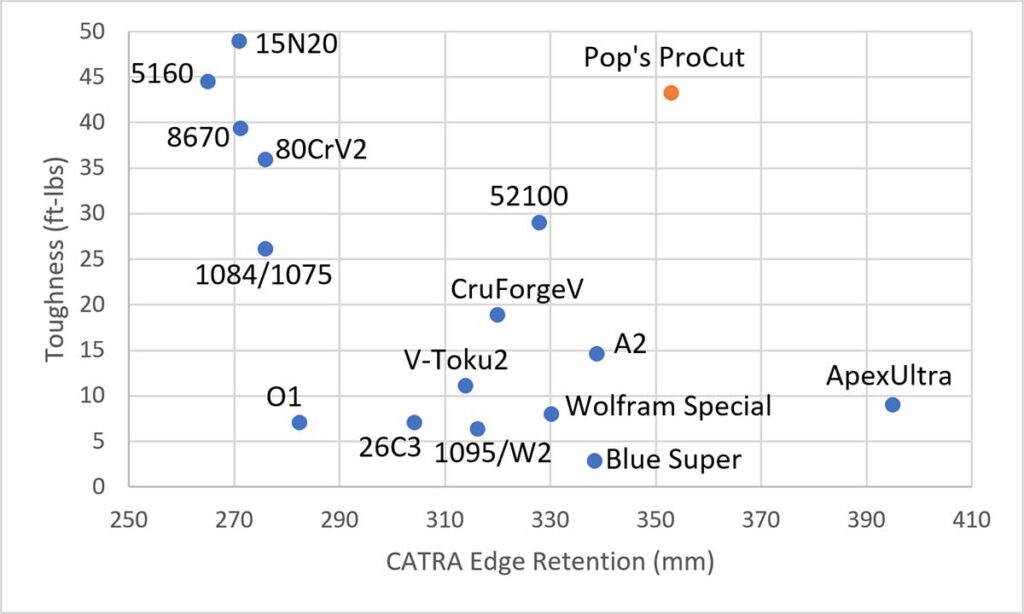
Pop’s ProCut’s toughness matched that of steels like 8670 and 5160, known for their excellent toughness. The edge retention was better than the majority of forgeable grades outside of ApexUltra, a high-performance forging grade.

Joey Berry of Pop’s Knife Supply contacted me in March 2024 asking for an improved version of Pop’s most popular grade, 80CrV2, which is known for being very easy to work, high in toughness and low in cost. I told Joey I would need to think about it because I had no idea off the top of my head what version of 80CrV2 would fill the niche of bladesmiths who want something inexpensive and easy to work. However, I have always enjoyed working with Pop’s Knife Supply, so I gave some serious thought to what kind of steel would be ideal for Joey’s request.

Pop’s is growing rapidly and has been a big supporter of mine, selling copies of my books—Knife Engineering and The Story of Knife Steel. It has been expanding its steel offerings and its steel education base to better serve customers, and I knew a steel along these lines would be a good fit for it. One of the trade-offs with knife steel design is when you add some elements like vanadium in significant amounts, things like forgeability and finishability go down. How could I make something new and exciting without pushing so much it becomes difficult for knifemakers to work with?

I thought about how high-nickel steels like 15N20, L6 and 8670 are known for their excellent toughness—at the top of my charts—but also have very limited wear resistance. I also knew some relatively rare steels like Blue #1, V-Toku2 and Wolfram Special have small additions of tungsten and vanadium for wear resistance. In grades with higher amounts of those elements, I start to see complaints from makers about the difficulty of working with them, though they seem to be at a place where they hit the right balance before forging and hand sanding become issues. These tungsten-vanadium steels are relatively challenging to find, often expensive when you do, and their toughness is much lower than the high nickel grades. As a result, the idea was to combine the high nickel approach for toughness with the controlled additions of tungsten and vanadium for wear resistance.

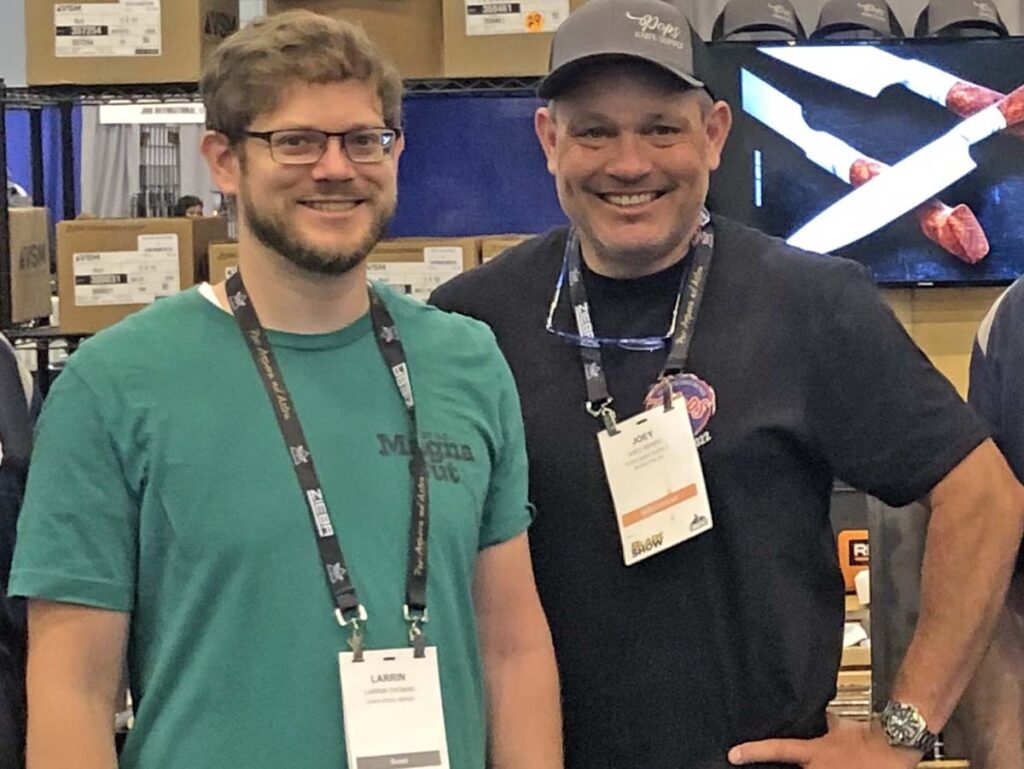
The author (left) and Joey Berry of Pop’s Knife Supply.

Another major factor for this development was the ease of heat treating. Often, steels like 1084 are recommended to novice makers for heat treating in a forge because it is dead simple to harden—just heat it to nonmagnetic and dunk it in oil. However, these grades are also very easy to overheat; they come out hard, but the toughness is greatly reduced. Only a few seconds in a forge past nonmagnetic can lead to a reduction in toughness.

On the flip side are grades like 80CrV2 that have chromium and vanadium additions to limit grain growth, so overheating isn’t as much of an issue. But the chromium also means you must heat past nonmagnetic and hold it there to ensure the carbides dissolve. The chromium slows everything down. However, I thought if we kept the chromium content very low the new steel could still be quenched from nonmagnetic and achieve full hardness, while the tungsten and vanadium additions would create tiny carbides that “pin” the grain boundaries so overheating and grain growth are not issues. This would make the easiest-to-heat-treat knife steel ever. Just heat it past nonmagnetic and quench it, and you will get high hardness and toughness every time.

My team and I got a steel company to agree to try the composition I proposed and waited (im)patiently for the steel to arrive. This was a major investment for Pop’s Knife Supply, and there was no guarantee the new steel would work just because it sounded good on paper. Fortunately, however, when we tested the steel, its toughness matched steels like 8670 and 5160, known for their excellent toughness. The edge retention was better than the majority of forgeable grades outside of ApexUltra, a high-performance forging grade I developed with makers Marco Guldimann and Tobias Hangler. And in testing the heat-treating range, we found it could be quenched anywhere from 1400°F up to 1750°F—over 300°F! This met our target of making a steel that is easy to heat treat.

Reports from makers have been very positive for Pop’s ProCut. They have praised the ease of working as well as the tested performance. Dawson Knives related: “We found it to be an excellent steel that 1) Offers a razor-sharp edge on par or better than other modern steels; 2) Holds that edge cut after cut; 3) Displays excellent lateral strength (it flexed close to 20 degrees in either direction and returned to true); and 4) Extreme impact resistance (edge resisted chipping, cracking or rolling when driven into a piece of steel Unistrut with a sledge hammer). We are able to get our edge hardness to Rockwell C of 62-63 and still retain superb flexibility.”

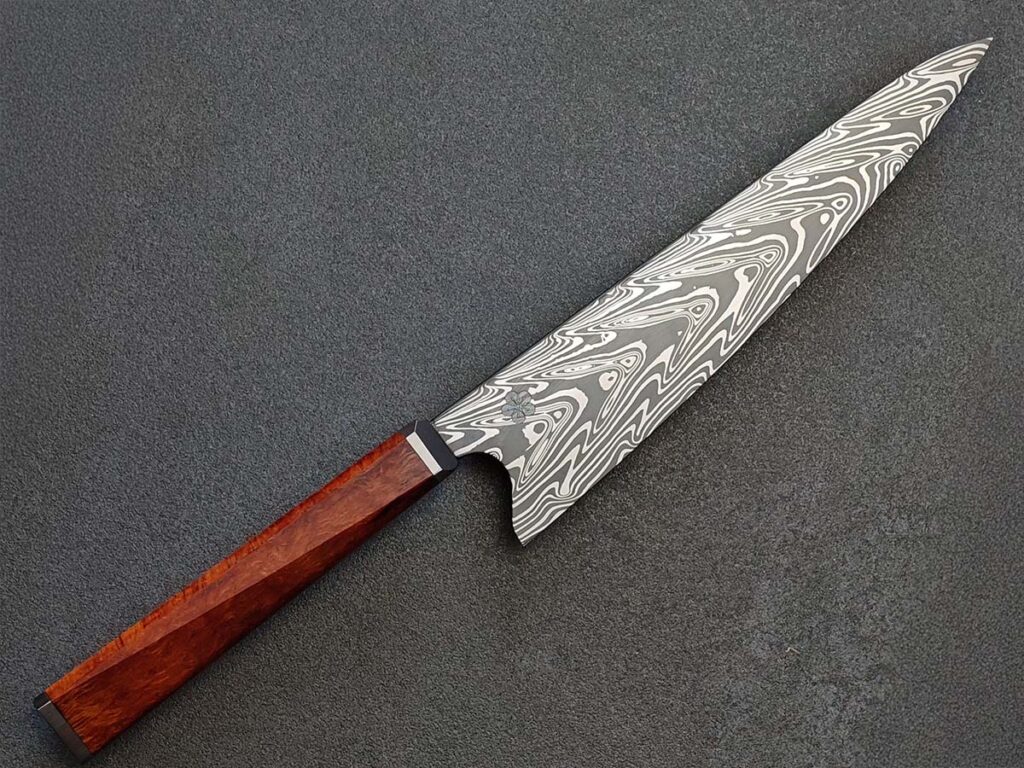
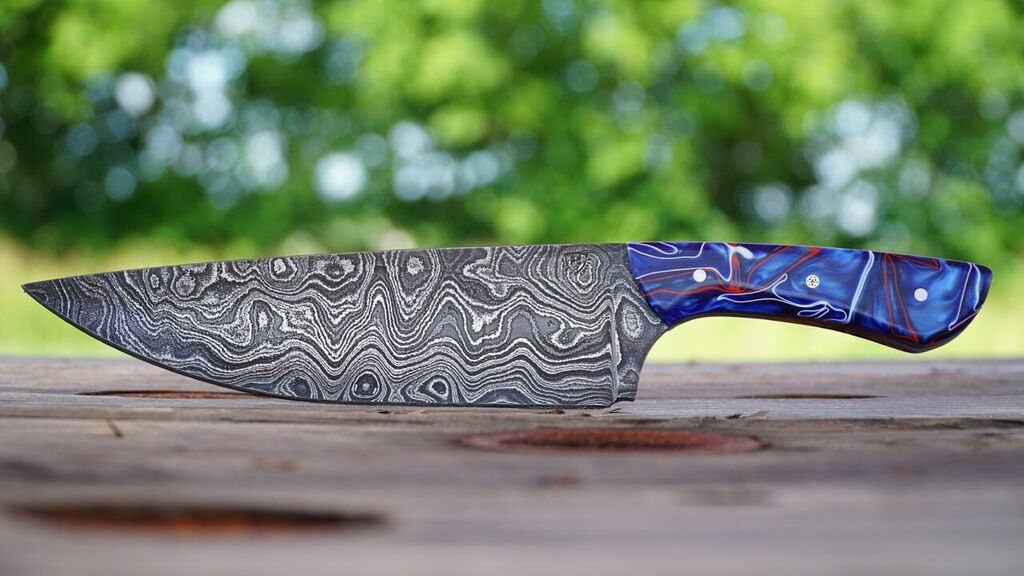
Kurt Glatt forged Pop’s ProCut and ApexUltra steels for the damascus blade of his chef’s knife.

Another exciting aspect of ProCut is the high nickel content (2 percent like 15N20) allows it to be used in pattern-welded damascus as a “bright” layer. This gives a new, higher-edge retention steel for use in damascus. As noted, previous high nickel grades have very low wear resistance. It can even be used in combination with other high-wear-resistance grades to make superior edge-retention damascus. I have seen a couple of knives using both ProCut and ApexUltra for some excellent-looking and performing damascus.

More To Come?

I’m constantly working on new ideas, though it’s hard to predict which projects will pan out or when they’ll be released. It’s been incredibly rewarding to see the steels I’ve developed used by top knifemakers and major knife companies, and to hear from end users who genuinely love them. When my dad, BLADE Magazine Cutlery Hall-of-Fame® member Devin “Hoss” Thomas, took me to my first knife show as a teenager, I never would have thought I would be working on such cool stuff.

More On Knife Steel:

The X-Rhea Experience: A Journey Of Craftsmanship And Connection

Follow the journey of Iranian bladesmith Masoud Hashemabadi, AKA Apurak, as he masters the art of the X-Rhea knife.

In February 2020, after months of contemplation and with the support of my wife, Maryam, I embarked on my journey in bladesmithing here in Iran. And I finally answered a long-standing urge within me—to delve into the world of forging and knifemaking. I was drawn not simply to the act of shaping steel but to the intricate, multifaceted craft of bladesmithing. Bladesmithing demands a convergence of skills: precise forging, material management, heat treatment, bevel grinding, understanding edge geometry, honing razor-sharp edges and more. Handmade knives, though ancient tools, continue to captivate enthusiasts today, representing a connection to human history.

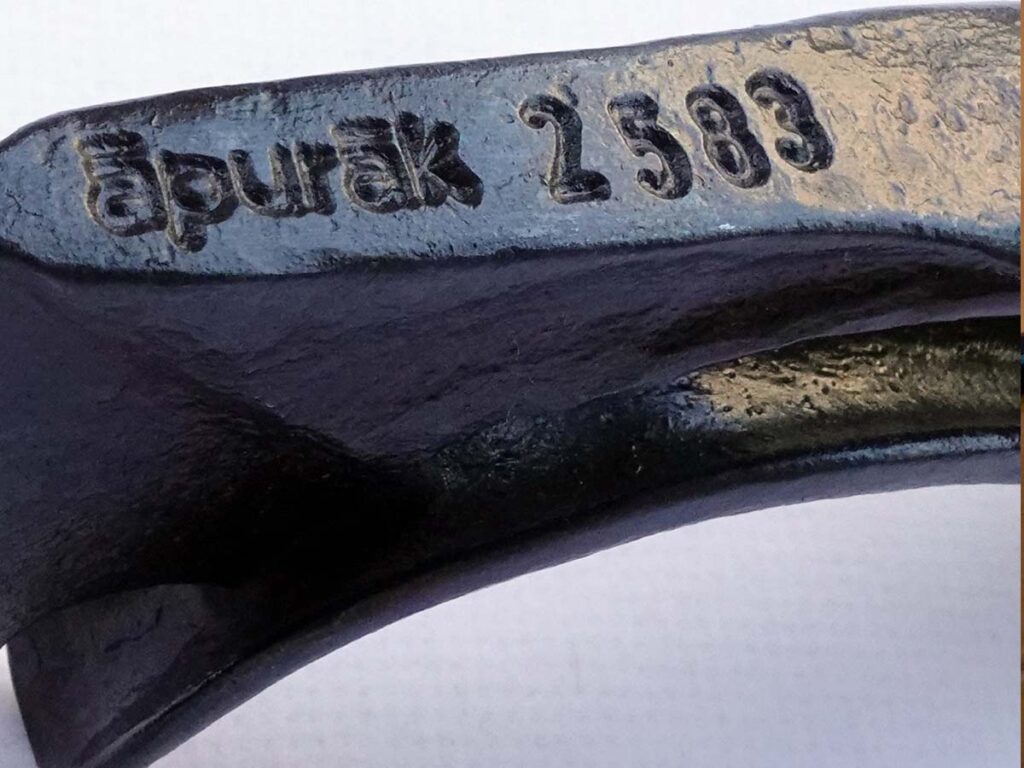
Each of my works bears the mark Apurak, also my handle on Instagram where I go by apurak.co. The word translates to “The Maker” in Pahlavi or the Middle Persian language—an ancient language.

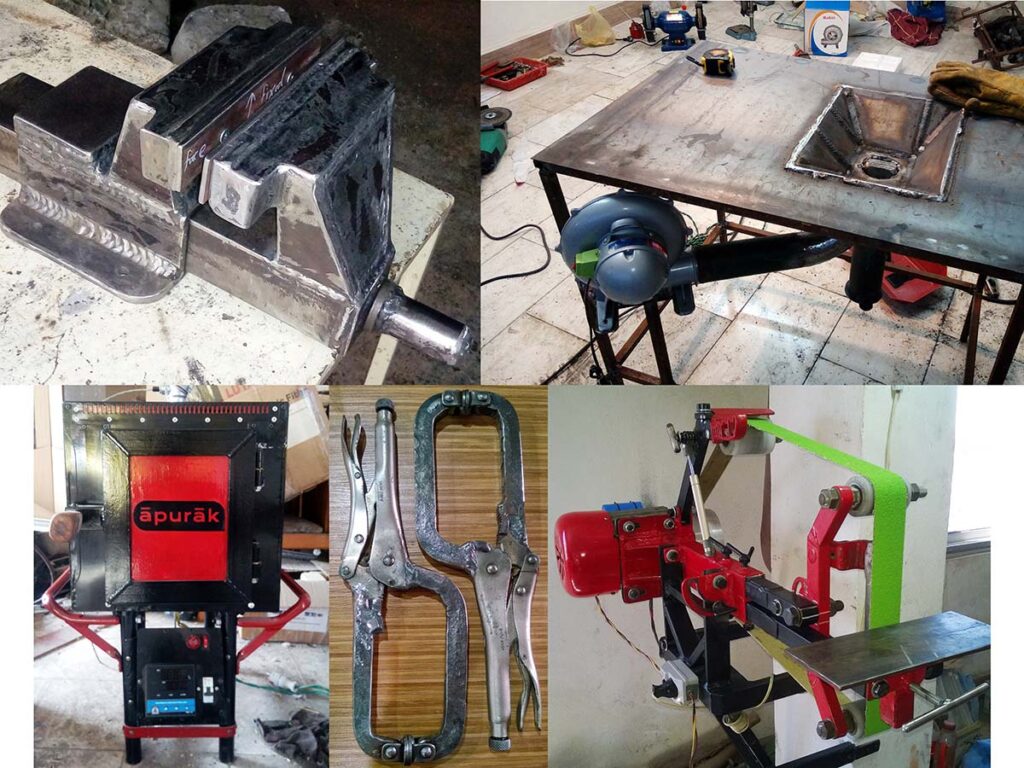
I began forging with basic tools: a steel block as an anvil, a simple hammer, a homemade coal forge, an angle grinder, a hand drill and a welding machine. I spent six months making additional tools and immersed myself in every piece of content I could find on forging. My first knives were rudimentary—simple full-tang and hidden-tang fixed blades. They were decent, but they didn’t fully satisfy me. During this time, I experimented with different designs, including the old blacksmith’s knife (sometimes known as the Viking knife). None of them quite captured my imagination.

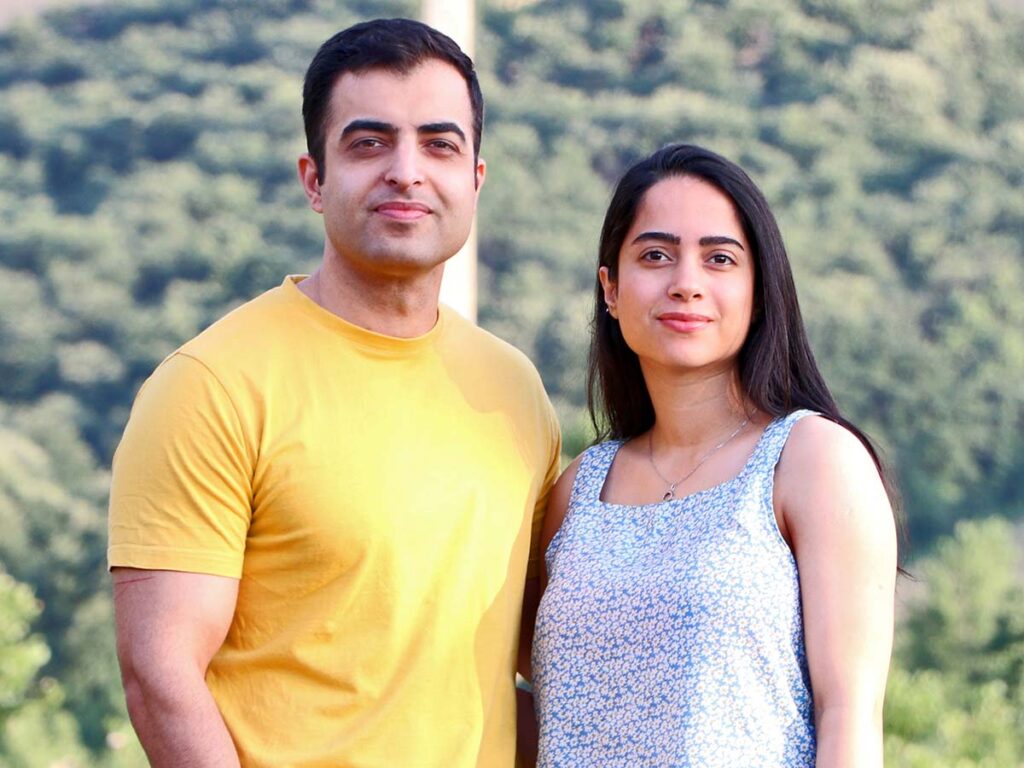
Masoud (left) began his blade smithing journey in 2020 after much contemplation and the support of his wife, Maryam (right). The desire to endeavor upon the multi-skilled craft of making knives had been longstanding in Masoud, he recounts.

Then, about a year into my journey, I came across ABS master smith Lin Rhea’s X-Rhea design on his Instagram account. This design—seamless, balanced and powerful—struck a deep chord within me. I knew I had to learn to forge this knife, so I respectfully reached out to Lin for permission. I watched his videos, analyzed every detail and eventually began my own attempts at creating an X-Rhea. This journey marked a new chapter in my life.

From Inspiration To Learning

No one can create a truly unique knife design early in their career. We all start by holding onto something, following established paths until we understand our own direction in the field. For me, the X-Rhea was this guidepost. My early attempts were crude and far from perfect—out of proportion and visibly flawed. But I was thrilled to make progress. With each X-Rhea, I learned more, not only about the design but about the fundamental techniques of forging. This process fulfilled me in ways I hadn’t anticipated.

Regular feedback from Lin himself was invaluable. We communicated frequently through Whats-App and Instagram, discussing various approaches to forging, hammer techniques, and the finer points of knife-making. Lin became more than a mentor; he became a friend, generously sharing his knowledge and guiding me through my early missteps.

X-Rhea Process

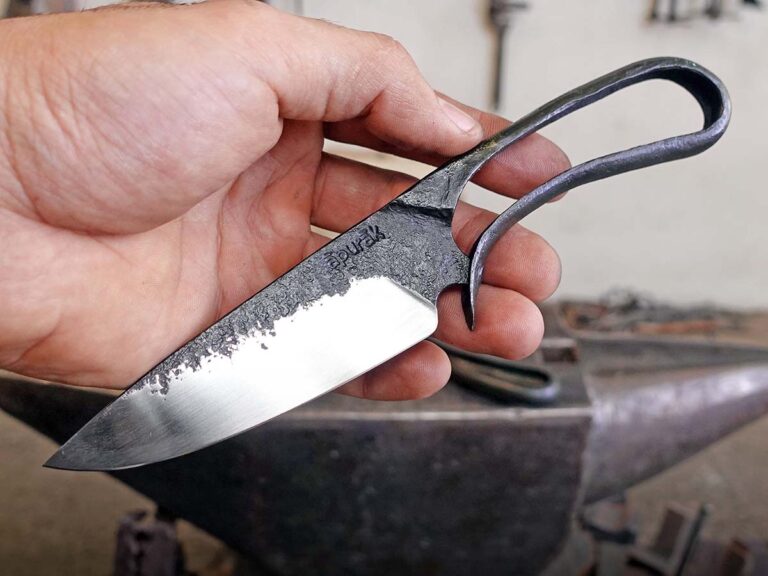
Masoud Hashemabadi maker's mark, Apurak. The word is from Middle Persian and means "The Maker." The numbering, seen on the spine of his work, is the year it was created according to the Cyrus Imperial Calendar.
Masoud Hashemabadi maker’s mark, Apurak. The word is from Middle Persian and means “The Maker.” The numbering, seen on the spine of his work, is the year it was created according to the Cyrus Imperial Calendar.

The X-Rhea has a unique shape, but the process of creating it is what makes it truly special. Unlike most designs, which often involve templates or precise measurements to envision the final product, the X-Rhea requires a different approach. You start with a rough sketch and rely on imagination, skill and a sense of flow to bring the knife to life. Each hammer strike must be deliberate and you visualize the end result throughout. This approach makes the final product feel like a true reward, a direct extension of the maker’s vision and hand.

For me, the X-Rhea became more than a knife—it became a pathway toward mastering my craft. Unlike conventional knives, which can incorporate multiple materials like wood, Micarta or stag, the X-Rhea is a single piece of steel. This simplicity, however, does not mean it’s easy to make. Achieving a knife that is functional, strong, ergonomic and aesthetically pleasing in a single piece requires foresight, skill and an understanding of the material’s properties.

Lin and I often spoke about this unique forging process. He explained how the X-Rhea or one-piece concept demands a cohesive flow of thought, a continuity that aligns with the uninterrupted structure of the knife itself. “There’s no breaking point,” he said. His words perfectly captured what I was experiencing in practice. This concept aligned with my personal philosophy: as makers, we should focus more on our skills and presence than on the tools themselves.

X-Rhea Of Tradition

A look at Masoud's tools he made in his early journey into knifemaking, including (top from the left) a bench vise, coal forge, (below going clockwise) belt grinder, clamps and a heat-treating oven.
A look at Masoud’s tools he made in his early journey into knifemaking, including (top from the left) a bench vise, coal forge, (below going clockwise) belt grinder, clamps and a heat-treating oven.

Throughout history, craftsmen have created extraordinary works with simple tools. When we look at the objects in museums, we see artifacts made with skills and techniques that, even today, seem nearly impossible to replicate. These craftsmen weren’t limited by the tools of their time. They relied on their presence, creativity and mastery, developing techniques that allowed them to reach incredible levels of precision and artistry. With the X-Rhea, I felt a connection to this tradition. Using only the most essential tools, I was able to engage deeply with each piece I crafted.

In today’s world, technology allows us to create faster and with greater efficiency, but it also risks overshadowing the maker’s role. Many makers, when faced with limited tools, may consider certain tasks impossible. Yet through my experience with X-Rhea knives, I found that fewer tools could offer a sense of creative freedom, encouraging me to explore what’s possible with technique alone. Each knife became a unique testament to the skill, discipline and power of traditional craftsmanship.

Working with Lin, I learned to view knifemaking through a different lens. He encouraged me to see the X-Rhea as an art form that goes beyond simple functionality. In his words, this process is like “a physical manifestation of a simple musical tune.” It became a flowing, intuitive rhythm rather than a rigid sequence of steps.

Editor’s Note: This is the first part of a two-part article. The second part of the article will be added to this story once it runs in the May 2026 issue of BLADE Magazine.

Read More:

Cool Custom: Robert Logan’s Tiny Fighter

Robert Logan had a scrap to pull off his Tiny Fighter.

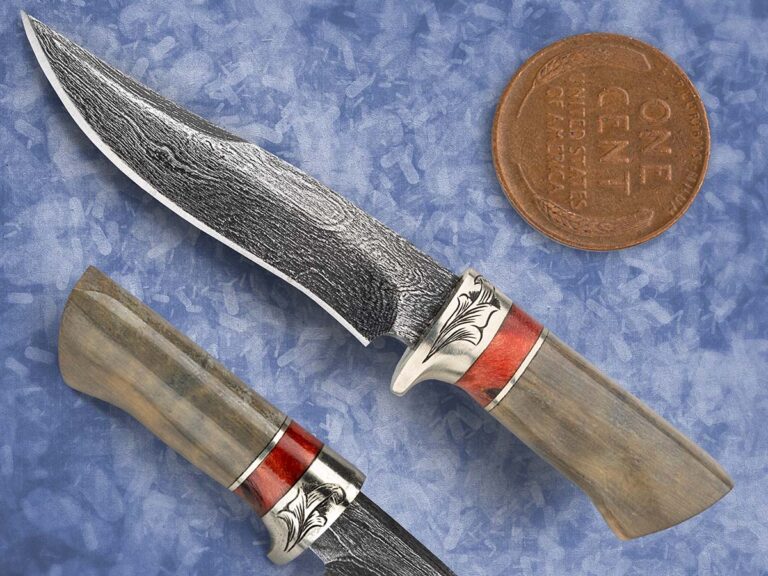
ABS apprentice smith and member of the Texas Knifemakers Guild, Robert Logan, has developed a varied catalog over his nearly nine-year career. His work in kitchen cutlery has raised eyebrows in some corners of the knife world. Yet, his smaller projects are certainly worth consideration.

Such is the case with Robert’s Tiny Fighter, a minuscule fighter whose detailed execution is hard to miss—even if it’s no larger than a penny. The knife measures a scant 2.875 inches in overall length, with a 1.6875-inch damascus blade (192 layer 1084-15n20). Setting it all off is a mammoth-ivory handle and a beautiful guard featuring engraving by Alice Carter.

Robert Logan
Robert Logan

Robert has tinkered with miniatures previously, making a couple of dozen scaled-down versions of his Mini Cleaver Belt Knife. But the Tiny Fighter, he said, was his first crack at venturing deeper than a simple slab handle in a miniature piece. Without special equipment for the job, it was especially tricky.

“Honestly, the most challenging thing about making tiny knives for me is just holding on to them,” Robert confessed. “I don’t use grinding jigs, so just holding on to the thing to grind, it was hilarious.”

More Custom Knives:

Two Generations Of Dennehy Knives Now At The Alamo

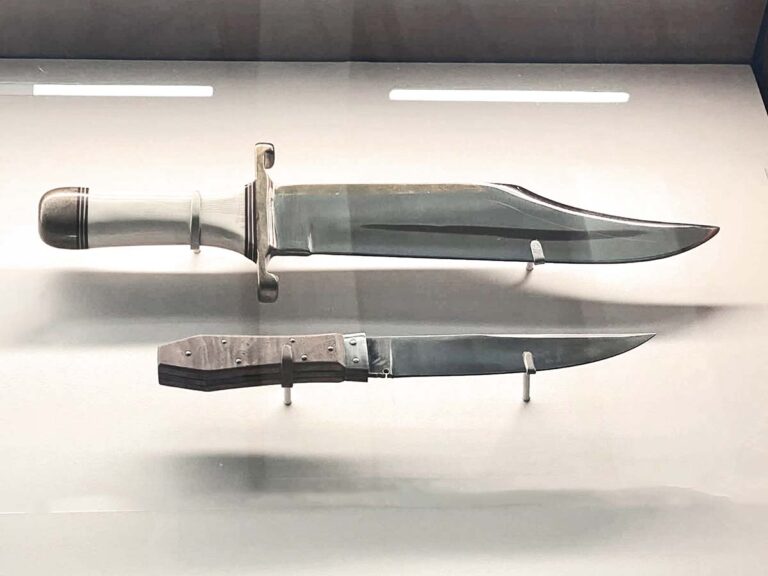
John Dennehy’s replica of his father’s Dan D Alamo Bowie, was accepted by the site on the 190th Anniversary of the historic battle.

We should always remember the Alamo, but 2026 is a particularly good year to keep the battle top of mind. It’s the 190th anniversary of the defining fight for Texas independence, and a fitting backdrop to a father-son knifemaking tale.

When Dan Dennehy donated his custom Dan D Alamo Bowie to the Daughters of the Republic of Texas in 1968, little did he know that a reproduction of the very same knife would be presented almost 60 years later to representatives of Alamo Trust just a few months before the historic anniversary of the Battle of the Alamo.

Made by Dan’s son John, the presentation reproduction is based on the original donated by Dan to the DRT in 1968. Save the engraving on the accompanying brass plaque. John did the entire repro project, which included 5/16-inch O1 tool steel like the blade material on his father’s original Dan D Alamo Bowie, and an embellished oak presentation frame.

Engraved number 5 of 10 by Pearce Richardson, the brass plaque reads: “Commemorative Dan D Alamo Bowie” over “In Honor of Those who Lost their Lives defending the Alamo in March 1836 and to the late Daniel J. Dennehy, Knifemaker, whose Alamo Bowie has proudly been on display at the Alamo since 1968.”

“It’s an honor that we can say we have knives from a father and son in our collection,” Alamo Senior Researcher and Historian Kolby Lanham said. “We are grateful to both Dan and John, two generations of knifemakers who chose to create works of art honoring James Bowie and the Alamo.”

John’s project started soon after his father’s death in 2011.

“The Alamo let me take pictures of Dan’s original knife in the spring right after his death,” he said. “I used those pictures and his knife pattern to make the reproductions. I wanted to jazz up the handle a bit since they are special editions with ivory Micarta and imitation ivory Micarta, along with some brass spacers for bling.”

From his own retelling of the story, Dan was inspired to make the donation during a visit to the Alamo, when he realized the historic site then didn’t have a single bowie knife. The namesake of the blade—Jim Bowie—was among the heroic men who fought and lost their lives at the battle.

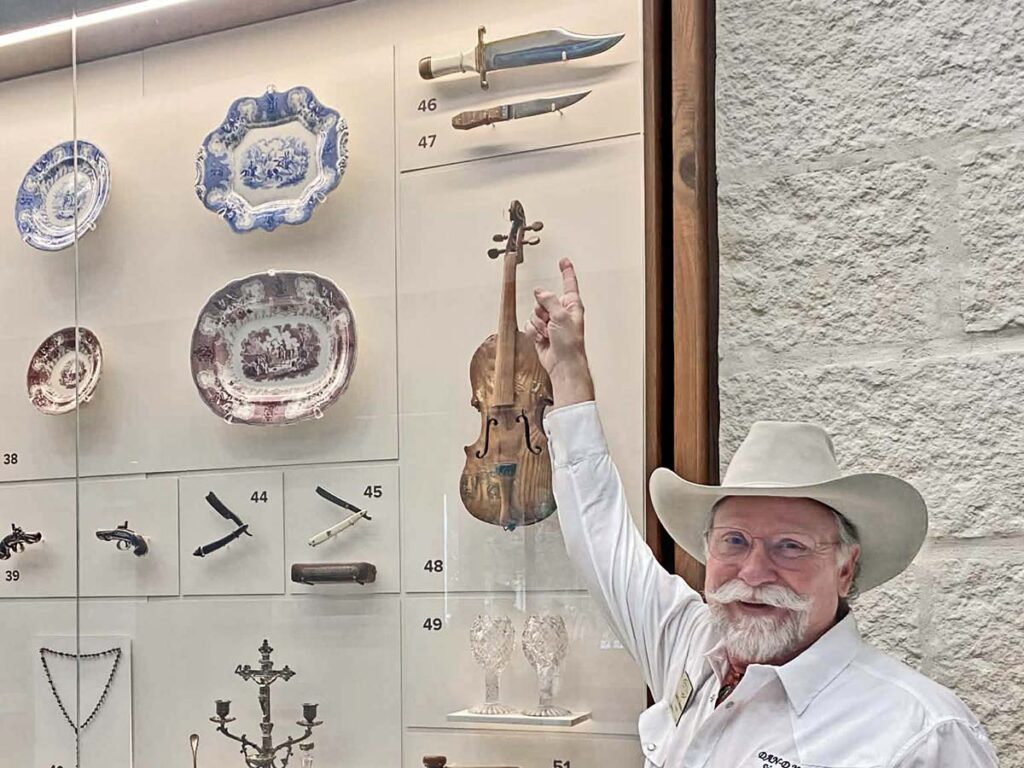
The original Dan D Alamo Bowie is displayed inside the lobby of the Alamo Exhibit at the Ralston Family Collections Center, according to Lanham. John’s knife resides in the Alamo’s artifact vault.

There are other storied knifemakers whose works are displayed at the iconic Texas site, including a reproduction of the Joe Musso bowie by BLADE Magazine Cutlery Hall-of-Fame® member Gil Hibben.

A founding member of The Knifemakers’ Guild, Dan Dennehy was also a member of the Cutlery Hall of Fame and the International Knife Throwers Hall of Fame, and for many years conducted knife-and-tomahawk-throwing demonstrations at the BLADE Show. John makes knives and sheaths and has conducted seminars on how to make sheaths at both the BLADE Show and BLADE University.

New York-born, Dan was always a Westerner at heart, John pointed out, known as “Tex” in the Navy and wearing cowboy boots and a hat most of his adult life. He also loved and revered the history of the Alamo, finding it as sacred a location as native Texans.

“Having one of his knives on display [there] was one of his most cherished accomplishments,” John said.

Read More:

Ed Fowler: Custom Knifemaker, Writer, Teacher Passes

Fowler had a lasting impact on handmade knives and knife writing.

The cutlery world recently lost one of its most steadfast creators and philosophers. Ed Fowler, a man who epitomized the spirit of the custom knife movement, passed away on January 17.

Ed’s journey in the industry began in 1962. Over the following six decades, he became a driving force in the evolution of functional cutlery. While he didn’t invent the use of 52100 ball-bearing steel, he was arguably its greatest champion, popularizing the material alongside his then-controversial methods of multiple quenching during heat treatment. For Ed, a knife wasn’t just a tool; it was an ongoing experiment in maximum performance.

To the readers of BLADE Magazine, Ed was a household name. For over a quarter century, he penned his monthly “Knife Talk” column, which consistently ranked at the top of reader surveys alongside BLADE Magazine Cutlery Hall of Fame® member Wayne Goddard. His writings were eventually compiled into two essential volumes: Knife Talk I: The Art & Science of Knife Making and Knife Talk II: The High Performance Blade. Whether he was conducting demos at BLADE Show or teaching at BLADE University, Ed was always eager to share his findings with anyone who sought a deeper understanding of the craft.

A former ABS master smith, Ed eventually founded the High Endurance Performance Knife Association. This organization was a reflection of his own soul—dedicated to understanding the limits of steel and ensuring every knife reached its absolute potential.

Ed’s voice was unmistakable. In his writing, a knife was never an “it”—always a “she” or “her.” He spent his life in a relentless search for what he called “Excalibur,” his version of the perfect knife. He drew deep inspiration from the legends of the past, including Hall of Famers Bill Moran, William Scagel, Rudy Ruana, and the 19th-century bowies of Henry Huber.

He was perhaps most famous for his insistence on testing. Ed had no patience for makers or companies that didn’t put their blades to the trial, and he was never shy about saying so. This commitment to truth in steel earned him a fiercely loyal following. Many of his readers didn’t just follow his column; they traveled across the country to visit him at his Willow Bow Ranch in Riverton, Wyoming, to spend time in the shop with the man who helped define the modern high-performance blade.

Remembering Others The Knife Industry Has Lost:

Advertisement

Must Read Articles

Read this before you make a knife

Knifemaking 101 – Read This Before You Make a Knife

  by Wayne Goddard My experience has taught me that there's nothing like digging in and getting started. I've often said the hardest part of the...
how to forge damascus steel

How to Forge Damascus

Advertisement
Advertisement