While visiting Sid Suedmeier at the Little Giant shop in Nebraska City, NE he explained the differences between the Old and New style Little Giant Power Hamm…
Knifemaking is the building of a knife, which includes the blade, handle and other accouterments. Blades are made by either removing metal from a steel blank via a grinder – known as stock removal – and the forging to shape of hot steel into a blade in the process known as bladesmithing. Other parts, including bolsters, guards, pommels, etc., are needed to complete the finished knife.
| Featured Knives – | – Knife Collecting – | – Tactical Knives – | – Survival Knives |
While visiting Sid Suedmeier at the Little Giant shop in Nebraska City, NE he explained the differences between the Old and New style Little Giant Power Hamm…
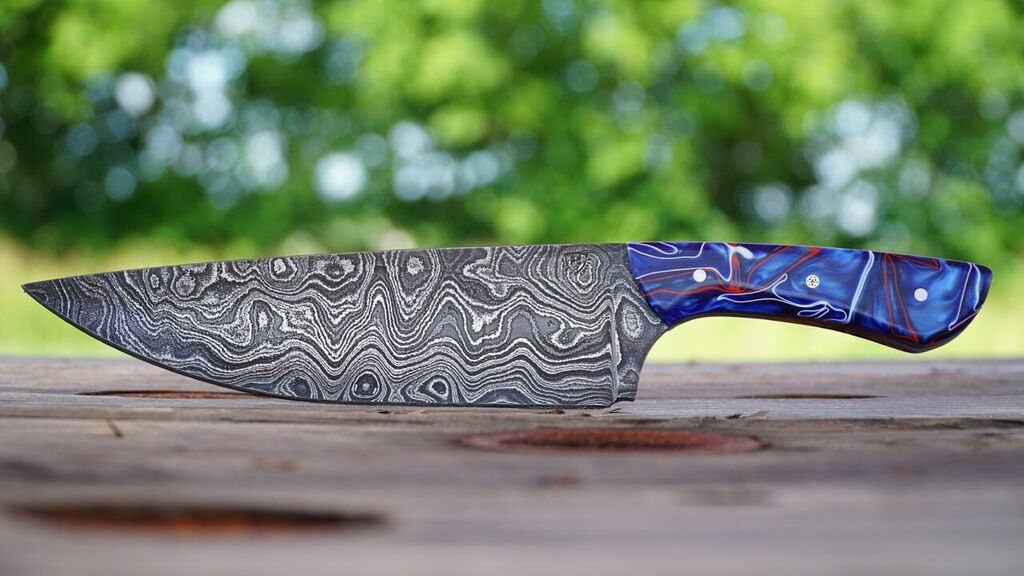
 Darrel Ralph outfits his assisted-opening DDR Gun Hammer 3-D Alpha in a 3.95-inch blade of stainless damascus with a Stellite 6K core by Chad Nichols. The frame is Nichols 3-D-carved Moku-Ti titanium damascus. Ralph’s list price: $3,500. (knife photo courtesy of Darrel Ralph)
Some of today’s alternative blade materials may change the way you look at knives
By Pat Covert
TO MOST KNIFE ENTHUSIASTS, THE WORD STEELis so closely associated with blades it would be hard to describe a knife without it. After all, since its earliest known production about 4,000 years ago, in one form or another steel has ruled the roost not only in cutlery but so many other things that pervade our lives.
Simply put, steel is everywhere. Unfortunately, most versions of it rust.
Progressive thinking in the knife arena has led to a boom in the technological aspects of blades, which includes those of materials that do not rust or rust very little in comparison to stainless steel. (Stainless steel resists corrosion but is not impervious to it.) In the process, cobalt-based alloys such as Stellite®, Talonite and Cobalt Dendritic have received attention. Other materials such as laminates using titanium and carbon fiber, as well as ceramics, also have been used to good effect.
Frost on a Windowpane
 Not a common metal, most of the world’s cobalt is mined in the Republic of the Congo. Today, most cobalt is used in corrosion-resistant “super alloys,” which are particularly suited for gas turbine and jet aircraft engines.
David Boye has been making knives for over 40 years. He offers fixed blades and folders for use around saltwater and other rust-inducing environments. He has used dendritic material exclusively since 1980 because he says he prefers its strength, cutting performance, ease of sharpening, and ability to cast roughly to shape.
(Editor’s Note: For a better understanding of forging various metals into blades, check out The Complete Bladesmith: Forging Your Way to Perfection, pictured at left.)
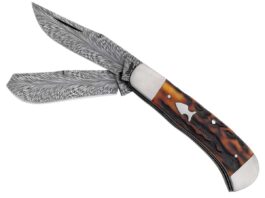
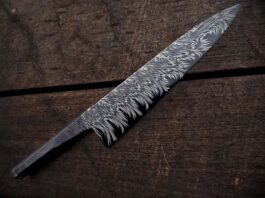
“Dendritic is the kind of pattern [damask] which naturally forms when a carbon alloy cools after smeltering,” Boye explains. “It looks like frost on a windowpane.”
According to many knifemakers, the finer the blade’s grain structure, the better it cuts. Boye supports the opposite view.
“These relatively large, rooted and fully bonded carbides produce microscopic teeth along the cutting edge, and this is what actually does the cutting,” he notes. The combined attributes of extreme cutting performance, no rusting in seawater and being non-magnetic so it does not affect a compass or electronics make the material ideal for the ocean environment. “We have used dendritic cobalt for over 15 years and have received virtually zero chips, broken blades or complaints,” Boye says, “and many customers have raved to me about the blade performance.”
He states that the material’s downside is each knife design requires a set of porcelain molds which are challenging and/or expensive to make, the mold created for each individual blade has to be discarded after only one use, the casting alloy is costly, and the waiting time for blades from the foundry can be lengthy.
Damascus Hybrid
Chad Nichols is a large supplier of damascus to the cutlery industry and has pioneered a new blend of patterned steel using cobalt 6K, commonly known as Stellite, and stainless steel—particularly AEB-L and 304. “The interesting thing about the 6K cored steel is that the cobalt alloy itself does not have to be heat treated to retain edge-hold abilities,” he observes. “The only reason the material needs to be heat treated is for corrosion resistance [for the stainless steels in the damascus] and for etching purposes.”
Nichols outlined several attributes of the hybrid damascus, “The addition of the cobalt-based alloy increases its durability and oxidation resistance,” he states. “The cutting performance of the 6K damascus is great. It’s a workhorse of a steel for cutting and can retain a razor edge even under the most vigorous conditions.” As for the disadvantages of the material, there are two. “The blade material is expensive. You already have a relatively high cost for the damascus and then you add the 6K which, pound for pound, costs more than the handmade damascus,” Nichols says, adding, “It’s not a lot of fun to make, either!”
“Won’t Crack Under Flex”
The book on modern laminate blades using metal bonded to synthetics was co-authored by knifemaker Warren Thomas (also, see page 114, August 2011 BLADE®). He indicates he began making laminate blades in 1991 using stainless steel and carbon fiber. Shortly thereafter he substituted titanium for steel, creating a lightweight, zero-magnetic knife. Thomas says he uses a “trade-secret” chemical bond that positively adheres the two materials.
“My laminates have half the weight of a steel blade, absolute zero corrosion, won’t crack under flex, and don’t micro-fracture under heavy stress along the cutting edge like steel blades do,” he explains. “To improve the performance of the blade, I weld tungsten carbide along the cutting surface to enhance the edge retention. This gives it a toothy edge that improves the cutting performance.
“There is no chance of corrosion using carbon fiber and titanium. Both materials are impervious to common destructive forces like sea salts, body sweat, and other elements that wreak havoc on steel,” he notes. “Steel knives have a very hard time cutting some synthetics, such as Kevlar™. My knives actually cut these materials quite well due to their ability to saw through them.”
Laminated blades do have their disadvantages. “In very rare circumstances, the blade can delaminate. I’ve had this happen approximately a dozen times in 20 years and have always corrected the problem for the customer,” he says. “Due to the direct cost of the state-of-the-art materials involved and the time spent fabricating the laminates, there is a higher cost for my blade over steel. However, you get what you pay for.”
That’s Edge Retention!
 Ceramic blades are made by taking zirconium oxide—also known as zirconia—powder, compacting it under intense pressure, and heating it in blanks at high temperatures in the 1,400° Celsius range. The blades are much more common among kitchen knives, and for good reason. For straightforward slicing and dicing they are extremely effective, but for lateral blade movement with torque, such as for prying, they tend to snap or shatter.
Boker Knives has never shied away from thinking outside the box, and its ceramic knife line not only includes kitchen knives but tactical and everyday carries as well. “If used as intended, ceramic blades will outperform steel,” Boker USA CEO Dan Weidner says. “In an independent lab test performed comparing ceramic to steel, technicians measured the amount of pressure required to cut through a standard piece of cardboard. After 1200 cuts the pressure required to cut using the ceramic blade was the same as the first cut, while the identical task using a steel blade showed decline after 400 cuts.” Now that’sedge retention!
Ceramic blades also have other benefits over stainless steel, including corrosion resistance. “This is one of the prime advantages of ceramic,” Weidner opines. “It cannot rust, which is why it’s used so often in maritime and military saltwater environments.”
There is also good news on the economic front. “Initially the cost of ceramics was on the high side, but now there are sufficient manufacturers producing the material to put the price point in the same range as good, quality steel,” Weidner says. Moreover, ceramic blades are non-magnetic.
Is One For You?
The strange brews in blade technology are not for everyone, but they offer a wide range of features, including either no rust or a huge reduction of same, zero magnetism, weight reduction and enhanced edge holding. Granted, there are downsides in some instances, though apparently not enough to discourage enough buyers of the blade brews outlined herein.
Is there an alternative blade in your future?
For more on alternative blade materials such as Spyderco’s H1, Strider Knives’ Nitinol, and Bohler-Uddeholm’s Vanax 35 and 75, see page 68 of the April 2011 BLADE®.
Also be sure to check out BLADE’s Guide to Making Knives.
For more on the latest knives, knife legislation, knifemaking instruction, knife trends, knifemakers, what knives to buy and where and much more, subscribe to BLADE Magazine, the World’s No. 1 Knife Publication. Subscribe to BLADE magazine.
Great knives, knifemakers, tips on knife collecting and much more are in the offing at venues across the country and abroad today and tomorrow, April 28-29.
The Solvang Custom Knife Show is in Solvang, California, today ONLY. Some of the world’s finest custom knives and knifemakers are there. For more info click on www.nordicknives.com.
The 30th Annual NCCA Extravaganza Knife Show is at the Hilton Hotel in Mystic, Connecticut, today and tomorrow.
The Wolverine Knife Collectors Show is in Novi, Michigan, today and tomorrow at the Suburban Collection Showcase.
The ABS Spring Piney Woods Hammer-In is today and tomorrow at the Texarkana College/Bill Moran School of Bladesmithing in Washington, Arkansas. For more info click on www.americanbladesmith.com.
The 13th Annual Knifemakers Show is at the German Blade Museum (Deutsches Klingenmuseum) in Solingen, Germany, today and tomorrow. For more info click on www.messer-macher-messe.de.
And finally, today is the final day of the Mason Dixon Knife Club Annual Show at the Best Western/Grand Venice Hotel in Hagerstown, Maryland.
For more on the latest knives, knife legislation, knifemaking instruction, knife trends, knifemakers, what knives to buy and where and much more, subscribe to BLADE Magazine, the World’s No. 1 Knife Publication. For subscription information click on http://www.shopblade.com/product/blade-magazine-one-year-subscripti…?r+ssfb042812#BL1SU.
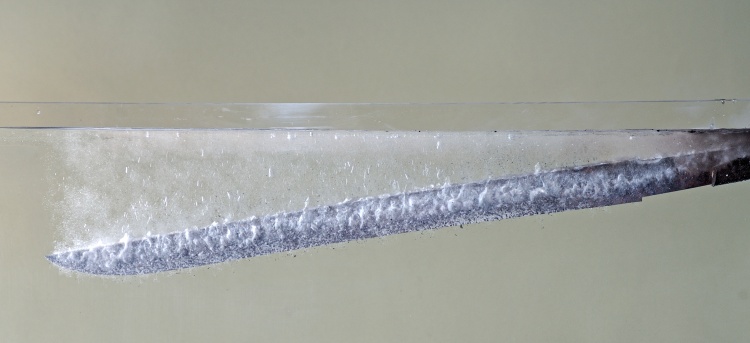 A tanto is plunged into the water during the hadaka-yaki process—yaki-ire, or heat treating, with no clay coating on the blade. (Yoshikazu Yoshihara photo)
Reader questions BLADE® story description of Japanese-style heat treatment
By BLADE staff
Question: Regarding part three of the “HAMON!” series, page 46, in the November BLADE®: Bladesmithing articles written by observation sometimes lack accuracy. To heat treat tool steel you anneal first, then harden and then temper to change hardness into toughness. That temperature is usually 400°F to 435°F and it is called tempering for about 30 minutes.—Bob Rupert, Pittsburgh, Pennsylvania
Answer: The author of the series, Leon Kapp, was kind enough to provide the following comments on Mr. Rupert’s letter:
I described the process exactly as Yoshindo Yoshihara and other swordsmiths in Japan do it (and as I have done it myself). The process is at least 1,200 to 1,400 years old in Japan. It was developed and used for tamahagane—a raw steel made of Japanese iron-bearing sand that requires extensive refinement—and works beautifully for that steel. However, I think a main difference between tamahagane and modern steels is that tamahagane contains only small traces of anything except iron and carbon. Manganese or other elements in the steel might require changes in this process. If done right, the Japanese process hardens the blade all the way through the hamon, and not just near the surface.
In fact, since all my experience is with Yoshindo and Japanese swords, I am very surprised and do not understand the technical reasons for the complex hardening methods I read about in BLADE or hear about from modern U.S. makers. It appears that Japanese-style yaki-ire (heat treatment) is a relatively simple process, but it does take years of experience to get it right.
After yaki-ire, the blade is annealed by heating it in the forge, again as described in the story (that is, yaki-modoshi). If that is not done, the blade will be very brittle and even very difficult to polish.
I think this is a reasonable answer to Mr. Rupert: The article is a detailed description of the process exactly as used in Japanese swords. The process and the steel are both very old and traditional in Japan, and it is done exactly as described—but the yaki-ire process was developed specifically for tamahagane steel.
Anthony Dicristofano (page 12, September BLADE®) has experimented with yaki-ire (Japanese style) for both tamahagane steels and for modern knife steels and told me he can see the differences. (Anthony works with Yoshindo in our backyard forge often during Yoshindo’s visits.) I think an important point to take from this is there are many ways to obtain great results with variations in materials and techniques.
Oh, and one more point: There is another goal in Japanese and Western hardening. The Japanese method is designed to specifically harden only the edge region. As far as I know, the Western approach usually seems designed to harden or heat treat the entire blade. If yaki-ire were used to harden the entire blade, Yoshindo says the thin Japanese blades would crack or shatter immediately in use.
Question: How much forging is enough? Is there a point of no return, or even a negative return? I typically start with 1-inch-diameter O1 drill rod for my knives, which I first must reduce to a flat piece of steel in the basic knife shape I want. This takes three-to-four heats to accomplish, and sometimes more depending on the size of the finished knife. Once the basic shape is attained, I then start working in the bevels.
Is the reduction from 1-inch round to a quarter-inch flat going to give me all the benefits from forging that can be gained? Is the bevel forging simply gratuitous at that point? It occurs to me there must be a point in the process when additional heating and forging causes enough carbon loss to start degrading the steel rather than improving it. (Joshua States, a letter via e-mail)
Answer (graciously provided by BLADE® field editor Ed Fowler): Starting with a 1-inch round bar should get you up into the 80-point rate of reduction range, depending on the size of the blade. This rate of reduction can definitely get you into the high-endurance performance realm, providing the steel you are using is of decent quality and you do not exceed a temperature of 1,725°F while forging. Forging at low temperatures equals fine grain and no measurable loss of carbon below the surface of the blade—about .002 inch, which is scale that comes off anyway. Forge the blades a little oversized and leave the edge of the blade about the thickness of a nickel for the heat treat (hardening and tempering).
In our work at my Willow Bow Ranch, we have forged and tested to destruction many 5160 blades from 1-inch round bars (John Deere Load Control Shafts), and can get within 10 percent of the high performance of the blades forged from larger round bars.
The more forging heats under 1,725°F, the better the performance potential of the steel. I take my bars to only 1,625°F to provide a margin of safety to prevent grain growth. Most of the benefits of forging will come from the round bar to quarter-inch flat bar. Merely forging the bevels only adds another two or three points if you are practicing reduction by forging. You are better off leaving the blades thick to protect the best edge, which will lay under the surface of the “as-forged blade.”
When I start grinding, I take about the thickness of a dime off the edge of the hardened and tempered blade. The edge surface goes through a lot of thermal cycles and sometimes the best edge lies under the surface.
As far as I know there is no “point of no return,” but the potential benefits between an 80-point rate of reduction and 99-point rate of reduction are not as significant as a difference between a 10-point rate of reduction and a 30-point rate of reduction. In other words, there is a decreasing rate of benefit, but always a benefit. Picture an ant crossing a table. The first trip he goes only halfway, second trip he goes half the remaining distance and the third trip he goes only half the remaining distance. How long will it take him to get to the end of the table?
The answer is never. He will always be half the remaining distance to travel to the end, but the length of his trips becomes less each time.
Send your question to “Ask BLADE,” c/o BLADE, 700 E. State St., Iola, WI 54990, or e-mail [email protected]. We will not print your name if you request it. If your question concerns the value of a knife, please understand it will be almost impossible for us to determine a value from a picture or e-mail image without being able to examine the knife from all angles in person.
For more on the latest knives, knife legislation, knifemaking instruction, knife trends, knifemakers, what knives to buy and where and much more, subscribe to BLADE Magazine, the World’s No. 1 Knife Publication. For subscription information click on http://www.shopblade.com/product/blade-magazine-one-year-subscripti…?r+ssfb041912#BL1SU.
The 2012 ABS Journeyman Smith Knife of the Year is by Karl B. Andersen, JS. It is part of the 2012 at the ABS Knife Auction set for June 9, 2012 at the Blade…
The 2012 ABS Master Smith Knife of the Year is by Jon Christensen, MS. It is part of the 2012 ABS Knife Auction set for June 9, 2012 at the Blade Show in Atl…
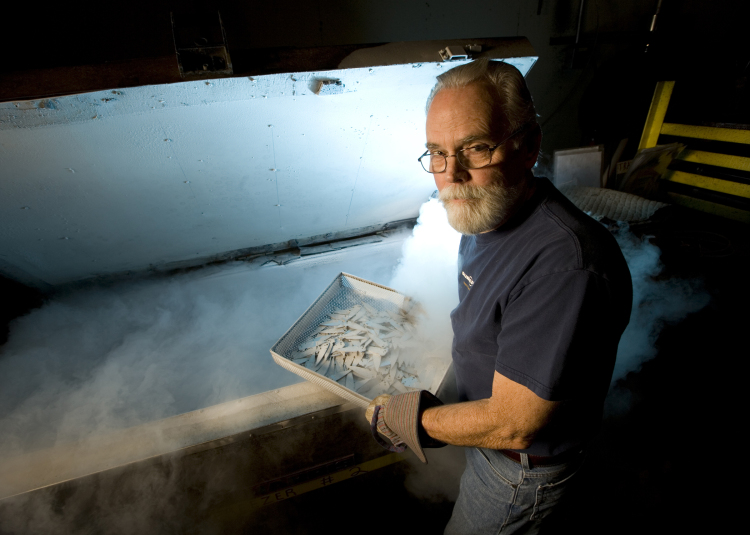
Cryogenic quenching may be performed on a single blade or hundreds at a time. Blade Magazine Cutlery Hall-Of-Fame© member Paul Bos said he may do a single blade or put a large quantity in a basket for immersion at one time, and control the rate of cooling and return to room temperature precisely. (Buck Knives photo)
Given the right steels, cryo treatments can enhance overall performance as well as aesthetics
By Mike Haskew, BLADE® field editor
Whether called cryogenic quenching or the probably more correct cryogenic treating of the steel, the process of freeze treating to help make a steel the best performer it can be is nothing new. Since the U.S. military became involved in cryogenically quenching steels during World War II and required it in the manufacture of various defense-related products, several methods have been evaluated with the same goal in mind: optimizing the amount of martensitic iron in the structure of the steel while minimizing the residual amount of austenitic iron. In turn, the qualities most sought in a knife blade are enhanced, particularly edge holding.
“There are different ways that cryogenic treating is performed,” explained Scott Devanna, vice president of marketing and product development for Carpenter Steel, “but all methods are designed to accomplish the same goal, although the methods sometimes attain differing degrees of transformation from austenite to martensite. Cryogenic treatment is not a different type of quenching method but is an additional treatment normally used after quenching. It’s used after the quench in an effort to achieve more complete transformation of austenite to martensite [martensite being the hardest of the transformation products of austenite].
“Most tool steels actually develop their hardened structure, or martensite, during the quench,” he continued. “For various reasons, however, in some cases transformation to martensite may not be complete even at room temperature. In such cases, some of the high-temperature microstructure, or austenite, may be retained after normal heat treating.”
A2 and D2, as well as other high-alloyed tool and specialty steels, may contain as much as 20 percent austenite after normal heat treating. Cooling the steel to cryogenic temperatures furthers the conversion to martensite. However, the process is specialized and requires close attention to actual temperature, levels of exposure, and the time intervals involved in raising and lowering the temperatures of the steel itself.
“The newly formed martensite is similar to the original as-quenched structure and must be tempered,” Devanna warned. “Cryogenic treatments should always be followed by tempering. Often the cryogenic treatment is actually performed between normally scheduled multiple tempers. Technically, cryogenic treatments are most effective as an integral part of the original quench, but due to the high risk of cracking, it’s recommended that tempering or a snap temper be performed before any cryogenic treatments.”
The cryogenic quench itself is performed primarily in two ways: shallow and deep treatments. In the shallow treatment, the blade steel is brought to approximately -112°F for five hours, while in the deep treatment it is reduced to roughly -321°F for about 35 hours. This is most often accomplished through immersion in liquid nitrogen.
“The term quench tends to imply that there’s a rapid change in temperature,” noted Spencer Frazer of SOG Specialty Knives & Tools. “In the case of cryogenic treatment, the quench term is quite misleading. Due to the severity of the temperature involved, quenching the material would cause it to crack or fracture. For that reason, cryogenic treatment is performed using computer-controlled temperature changes. At SOG, we use a version of deep cryogenic treatment, and some adjustments were made to the standard method to best suit the knife steels SOG uses. We consider it a supplementary process that helps improve the wear resistance of the blade steel.”
Blending In The Clumps
Blade Magazine Cutlery Hall-Of-Fame© member Paul Bos began heat treating knife blades in the 1950s. Back then he worked in the aircraft industry and treated a number of components. He said he also has seen the cryogenic process produce higher performance in guitar strings, women’s nylon stockings, gun barrels and engine parts.
“I figured if the military wanted it done, then it would be good for knives,” Bos said. “Originally, it was there to get rid of austenite in martensitic steel. Austenite makes steel brittle, and under a microscope you can see what looks like little clumps of carbon. The cryogenic process is like putting stuff in a blender with clumps and pretty soon everything is mixed in a fine solution. Once you do the cryo on a steel, then the austenite dissipates and you are left with a fine grain structure.”
Bos does a snap temper on high-carbon tool steel and then the cryogenic process at -280°F for about eight hours, and then brings the steel slowly back up to room temperature before a second temper. While cryogenic quenching is not a necessity on high-carbon steels*, its effects are more profound on higher-alloy-content steels, which do not completely transition from austenite to martensite at room temperature.
“Once the steel gets past -100°F it’s in a state where you aren’t hurting it, but you can’t leave it in there too long,” Bos added. “Some guys go right from the quench into the cryo, but the blade could crack or break, and I don’t do that because I can’t take a chance with my customers’ blades.”
Both factory and custom knifemakers take advantage of cryogenic quenching, and the process may be performed on a single blade or hundreds at a time. Bos’s career has spanned decades of heat treating blades for Buck and for a vast number of custom makers, including some of the most famous of all time. He may do a single blade or put a large quantity in a basket for immersion at one time, and control the rate of cooling and return to room temperature precisely.
According to Bos, creating the optimal transformation of austenite to martensite is an integral part of the heat-treating process. To obtain the maximum formation of martensite, two or more complete tempering cycles are necessary following the sub-zero cryogenic quench. He stressed that the blades always should be allowed to cool to room temperature between tempering sessions.
Deep-Treatment Believer
For many custom makers, the benefits of cryogenic quenching are proven in the knife’s overall performance. Bob Beaty is a firm believer in the deep treatment below -300°F. A knifemaker since 1994, he does, however, note that simple steels do not seem to exhibit enhanced performance as a result of the procedure.
“I do both forging and stock removal,” Beaty remarked, “and basically you find most of the benefit in the more complex stainless steels. I believe the knife stays sharper longer, and I’ve tested that a lot and am still testing it. Once a month I’ll cut rope, cardboard and leather. I always get a big difference, probably a 40-to-50-percent difference in edge-holding capability, as the cryogenic quench refines the grain of the steel.”
Though he admits there are skeptics, Beaty says the enhancements of the cryogenic quench are real. In fact, he says he has experienced fewer incidences of edge chipping and an easier time getting a mirror finish on a blade after the cryogenic treatment.
For the custom maker, outsourcing cryogenic treating remains the most efficient method of getting the job done. “I recommend it for those makers using complex steels, and I’m only charged a small amount for the blades I send for cryo treating,” Beaty noted. “One of the downsides of liquid nitrogen is it evaporates, and that would make the process more expensive for me. Not only would I have to buy the nitrogen, but also the tank and other equipment, including an oven. It really does not add much to the overall cost of the knife. Of course, if you wanted to, you could cryo treat something in a thermos bottle. Just don’t put the lid on it, don’t put your hand in it, and don’t do it in your wife’s kitchen!”
A Difference Maker
The choice of steel apparently drives the benefit of the cryogenic quench. From a knife buyer’s standpoint, a cryogenically treated blade could make the difference in performance and easily justify any minimal added expense.
*According to Paul Bos, high-carbon steel usually is any steel containing anywhere from .6 to 2 percent carbon.
For more on the latest knives, knife legislation, knifemaking instruction, knife trends, knifemakers, what knives to buy and where and much more, subscribe to BLADE Magazine, the World’s No. 1 Knife Publication. For subscription information click on http://www.shopblade.com/product/blade-magazine-one-year-subscripti…?r+ssfb040312#BL1SU.